
PP welding rod batch consistency is a pre-fabrication control: the welding consumables released to a chemical tank job should match the approved material, documented duty, weld procedure or project instruction, and identification record. It is not a promise that one document alone proves finished-tank performance. The purpose is to prevent avoidable mix-ups before welding begins.
This guide complements QEEHUA’s articles on choosing PP welding rod for chemical tanks e welding-rod traceability. Its narrower focus is whether the pack, label, release record, work area, and allocated consumable all stay consistent through one tank-fabrication job.
Verify PP welding rod batch consistency against the approved requirement
Before receiving a batch, create one project line item that identifies the approved rod type, diameter or profile where relevant, colour if it is a specified visual identifier, quantity, project or tank tag, and the document revision that released it. Do not begin with a warehouse description such as “PP rod.” The project record should connect the consumable to the panel material, weld process, and service information already approved for that job.
Chemical-service evidence should be tied to the actual reagent, concentration, temperature, contact method, and exposure duration. ASTM D543 explains why chemical-resistance evaluation depends on the similarity between test and end-use conditions. Treat that evidence as an input to the engineering decision; do not infer universal compatibility from the word PP.
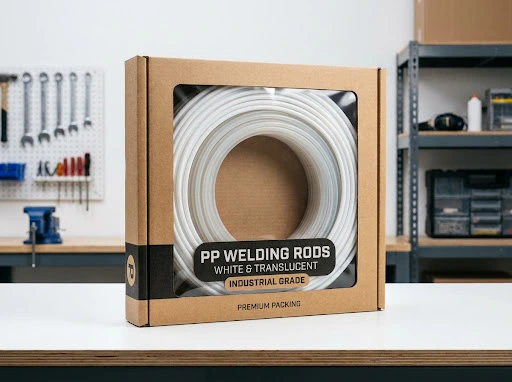
Compare the received batch against the purchase and release records
At receipt, compare the supplier’s identifying information with the purchase order, packing list, approved submittal, and the fabricator’s release list. Record the received quantity and any visible packaging damage. If the project requires a certificate, test report, or supplier declaration, check that its product identification agrees with the package before assigning material to the work order.
The receiving check does not need to invent a test programme that the contract has not requested. It should simply make discrepancies visible early: an unrecognised product description, missing identification, a different rod form, mixed packs, or an incomplete supporting record should be held for resolution rather than sent to the welding station.
Use this PP welding rod batch consistency check before the pack reaches the welding station, while replacement or clarification is still practical.
Keep approved batches physically and digitally separated
Once a batch is accepted, label the allocated storage location and the work-order issue record. Separate released material from quarantine, returned off-cuts, unknown remnants, and consumables assigned to other projects. A simple location tag and issue log are often more useful than a complex database if the team can show which material was released to which tank job.
Repeat the PP welding rod batch consistency check whenever a new pack is issued, a work order changes, or material returns from the fabrication area.
| Control point | What the reviewer should confirm |
|---|---|
| Approved requirement | Rod type, project tag, quantity, and governing drawing or instruction are identified. |
| Receipt record | Package identification agrees with the PO, packing list, and required supporting documents. |
| Issue to fabrication | The work order shows the released batch or package reference and allocated tank job. |
| Hold and disposition | Unknown, damaged, or discrepant material is separated and has an owner for resolution. |
Confirm the work area does not reintroduce a mix-up
A correctly received batch can still be mixed at the fabrication bench. Before welding, verify that the active job packet, prepared panels, and welding consumables use the same project identifier. Remove obsolete labels and close out the prior job before staging a new one. If several tank projects use similar rod sizes or colours, make the job tag visible at the point of use.
This check belongs with basic welding preparation, not with final inspection. For the next stage, use the separate PP tank weld inspection guide, which deals with release evidence after fabrication rather than batch consistency before it.
Define what happens to remnants and partially used packs
Remnants can be useful only when their identity is still controlled. The project procedure should state whether a partially used pack keeps its original label, receives a transfer label, is limited to the same job, or is returned to a controlled store. Do not combine unidentified short lengths into a future tank package merely to avoid waste.
When a job stops or changes, reconcile issued and returned material in a proportional way. The aim is not to create paperwork for every short off-cut; it is to keep uncertain material from silently becoming approved material on the next project.
A retained PP welding rod batch consistency record gives the project team a clear basis for deciding whether a returned pack remains suitable for controlled reuse.
Align batch review with material and weld records
Batch review sits inside the material-selection and fabrication controls for the complete PP assembly, but sheet values must not be copied into a welding-rod acceptance record. The local specification table gives PP sheet data; it does not publish a rod-specific qualification result for this job.
| Local PP sheet datum | Recorded result | Correct batch-control use |
|---|---|---|
| Tensile strength, ASTM D638-22 | 30 MPa | Do not treat as a welding-rod batch acceptance value |
| Flexural test, ASTM D790-25 | 1870 MPa | Do not treat as a weld or tank acceptance value |
| Density, ASTM D792-20 | 912 kg/m³ | Keep separate from pack identity, release, and issue records |
The useful numerical control here is the distinction between data types: sheet-test evidence, rod-pack identity, project weld instruction, and completed-weld inspection each need their own record and acceptance route.
The internal QEEHUA knowledge base keeps PP sheet and PP welding rod as separate product records because they serve different roles in a fabricated assembly. Preserve that separation in the batch review. A sheet identification record supports panel traceability; a rod-pack record supports consumable control; a weld or inspection record documents a further stage. Do not merge those records into one generic PP certificate statement.
For each released job, make the relationships visible: which panel designation is being joined, which approved rod batch is allocated, which drawing revision controls the joint, and where a discrepancy would be recorded. This supports disciplined material handling through receipt, issue, use, and remnants. It does not replace qualification, inspection, or project acceptance requirements, but it gives those later reviews a reliable chain of material and document references.
The fabricator can include the batch issue record with the material-identification, dimensional, and weld-inspection documents required by the contract. This gives the buyer a coherent evidence trail without overstating what any single record proves. For projects with a controlled drawing package, add the relevant record references to the PP chemical tank shop-drawing review before fabrication release.
If the project calls for material-property testing, make the request explicit: identify the test method, sample source, acceptance criteria, and approving party. ASTM D638 is a recognised test method for tensile properties of plastics, but the project team should specify whether it applies and how its result is used rather than treating it as an automatic tank-weld acceptance test.
Close discrepancies before the first weld
Give every discrepancy a clear owner and disposition. Typical examples include a missing package label, a mismatch with the release list, damaged packaging, incomplete documentation, or uncertainty about a remnant. The responsible project party can accept, replace, re-identify, or quarantine the material. The fabricator should not convert an unresolved question into an assumed approval.
Request a PP welding-consumable review
Share the tank duty, approved material requirement, purchase information, and fabrication record expectations with QEEHUA PLASTIC. A defined batch-control check helps the team resolve consumable questions before welding begins.
Referência em vídeo: This QEEHUA production video provides limited material-feeding context for PP manufacturing. It does not demonstrate PP welding-rod batch release, chemical tank welding, or final weld acceptance.
Perguntas frequentes
Is batch consistency the same as PP welding-rod traceability?
No. Traceability records the identity and movement of material. Batch consistency is the practical pre-fabrication check that the material released to the job agrees with the approved requirement and has not been mixed with unknown or other-job material.
Does a supplier certificate guarantee a chemical tank weld?
No. A certificate is one project input. Finished-tank suitability also depends on the approved design, service conditions, fabrication process, inspection plan, and the responsibilities stated in the contract.
How should a fabricator handle unidentified PP welding-rod remnants?
Keep them separate from approved job material and follow the project procedure for re-identification, return, or quarantine. Do not issue them to a tank job until their status is resolved.

