
A PP semicon screen can describe a perforated, slotted, or open-area PP sheet component used within semiconductor wet-process equipment. The name alone is not a complete specification. Before fabrication, the project team needs to define the process function, aperture pattern, open area, panel geometry, support method, interfaces, cleaning access, and the approved chemical duty.
When a screen drawing is released, Seleção de chapas de PP para equipamentos de processamento úmido de semicondutores has to be assessed alongside the component-specific aperture pattern, open area, panel geometry, supports, interfaces, and cleaning access. The material review identifies the operating environment; the screen RFQ then translates those conditions into controlled component inputs.
State what the PP semicon screen must do
Start the drawing with a functional statement. Is the part intended to separate a work zone, support a process item, distribute flow, protect an opening, retain a larger component, or provide an access barrier? Each function changes the relevant design inputs. A screen used as a simple guard does not need the same open-area, stiffness, or interface review as a panel that affects liquid movement through a process chamber.
Include the equipment tag, location, orientation, normal operating position, and the interfaces it touches. If the screen has a process effect, the equipment designer should provide the required aperture geometry, open-area target, permitted pressure or flow assumptions, and acceptance method. Do not create those values from a generic perforated-sheet catalogue.
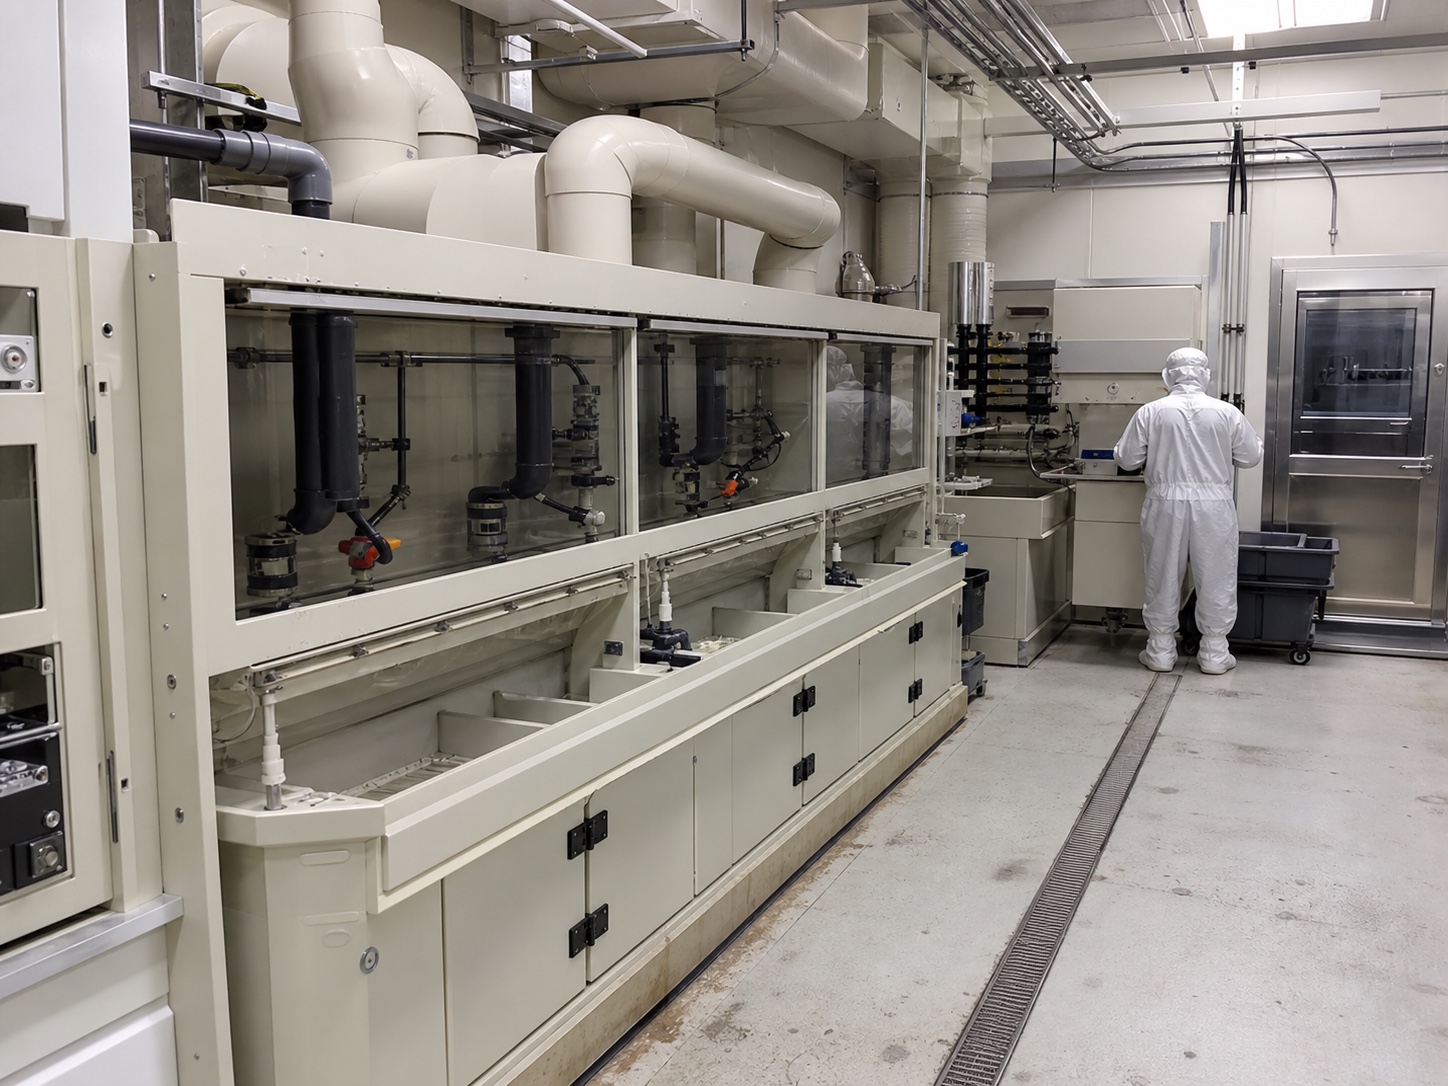
Put aperture geometry and open area on the controlled drawing
The drawing should identify aperture shape, size, pitch, pattern, panel edge distance, and any non-perforated border. State whether dimensions refer to the finished open area, the cutting pattern, or a nominal layout. Include the drawing revision and the approved file format for any digitally cut pattern.
Open area is not just a percentage on an RFQ. It works with panel thickness, support spacing, liquid path, cleaning method, and the process function. Where a customer supplies a layout, preserve its orientation and datum references. Where the layout is still under development, mark it as a hold point rather than releasing a generic substitute.
Confirm chemical duty and the actual exposure condition
The chemical record should be reviewed with the PP sheet material, fabrication, and application factors that govern the equipment component. The local material values below can identify the sheet evidence under review, but they do not state a screen’s open-area capacity, allowable load, chemical qualification, or equipment compliance.
| Local PP sheet datum | Test method | Recorded result | Screen-specification boundary |
|---|---|---|---|
| Densidade | ASTM D792-20 | 912 kg/m³ | Material identity and mass-estimate input only |
| Teste de flexão | ASTM D790-25 | 1870 MPa | Not a perforated-screen load rating |
| resistência ao impacto com entalhe Izod | ASTM D256-24 | 59 J/m°C | Not a component impact-acceptance criterion |
The component record should list the chemical or mixture, concentration, operating and cleaning temperature, contact method, expected duration, and any stress or mechanical contact that the process team considers relevant. ASTM D543 explains that meaningful plastic chemical-resistance evaluation depends on the similarity between test and end-use conditions. This is why the screen RFQ needs a duty record rather than only a material name. Review the QEEHUA PP sheets range alongside the approved project requirement.
Keep the chemical-duty decision separate from the aperture design. A panel can have a correct pattern but still require project review if the exposure record changes. For a broader material and equipment discussion, link the released component record back to the approved PP wet-process equipment selection package.
Design the border, supports, and mating interfaces together
A perforated area does not show the whole component. The drawing should also show the perimeter border, support tabs, fastener holes, slots, weld interfaces if any, and contact surfaces. Identify which party provides the mating frame, clips, fasteners, gaskets, or support rails. This prevents a fabricated screen from arriving with an open pattern that cannot be fixed, removed, or inspected in the equipment.
| Drawing item | Question to close before release |
|---|---|
| Open-area pattern | Are aperture shape, size, pitch, border, orientation, and file revision controlled? |
| Support concept | Has the responsible project party approved the intended supports and contact points? |
| Equipment interface | Are fasteners, frames, clips, and supplied-by responsibilities clear? |
| Maintenance access | Can the component be inspected, removed, and returned without an unplanned equipment change? |
Plan removal, cleaning, and reinstallation
Specify whether the screen is fixed, removable, or replaced as part of a service kit. A removable component needs a removal direction, required clearance, handling expectation, and a method for retaining or replacing its fixing hardware. It should not obscure an inspection point, sensor, label, or access route that the equipment user requires.
Where the screen will be cleaned, the project should provide the approved method and any limits on tools or handling. Make the cleaning and inspection sequence part of the equipment handover documents instead of leaving it as an informal site practice.
Align the component review with semiconductor equipment controls
QEEHUA’s local product records distinguish PP sheet, profile extrusions, and welding rod as separate fabrication inputs. For a semicon screen, the controlled drawing should state which of those roles is actually present. A perforated or slotted panel may begin as PP sheet; a frame, edge detail, or joining route may introduce another input. Naming them separately prevents a component-level RFQ from hiding fabrication decisions inside a generic PP screen description.
Carry that distinction into the review record. Identify the panel geometry, aperture pattern, borders, supports, mating interfaces, removal method, and any project-specified cleaning or material evidence. Then route chemical duty, process suitability, and equipment safety questions to the approved project controls. The result is an RFQ that uses QEEHUA’s internal application and product knowledge constructively without claiming that the component has a performance classification it has not been given.
Semiconductor equipment projects often have their own EHS, process, customer, and documentation requirements. SEMI S2 is a performance-based EHS guideline for semiconductor manufacturing equipment. The equipment owner or qualified project reviewer should determine which requirements apply to the complete machine and its options.
A PP sheet component does not by itself demonstrate equipment compliance. The screen RFQ should therefore identify the governing equipment specification, risk-review owner, drawing revision, and required records. This makes a small component easier to integrate into a controlled equipment package without overstating its role.
Send an RFQ that can be reviewed without assumptions
A complete RFQ should include the component function, equipment tag, drawing revision, aperture file or pattern, overall geometry, PP material requirement, chemical-duty record, support and attachment details, access constraints, required documentation, quantity, and packaging or cleanliness instructions supplied by the project. If a requirement is not final, label it as an open item with an owner.
Request a PP semicon screen review
Share the controlled component drawing, aperture pattern, chemical-duty record, equipment interface information, and documentation requirements with QEEHUA PLASTIC. A defined review package helps close component details before production is released.
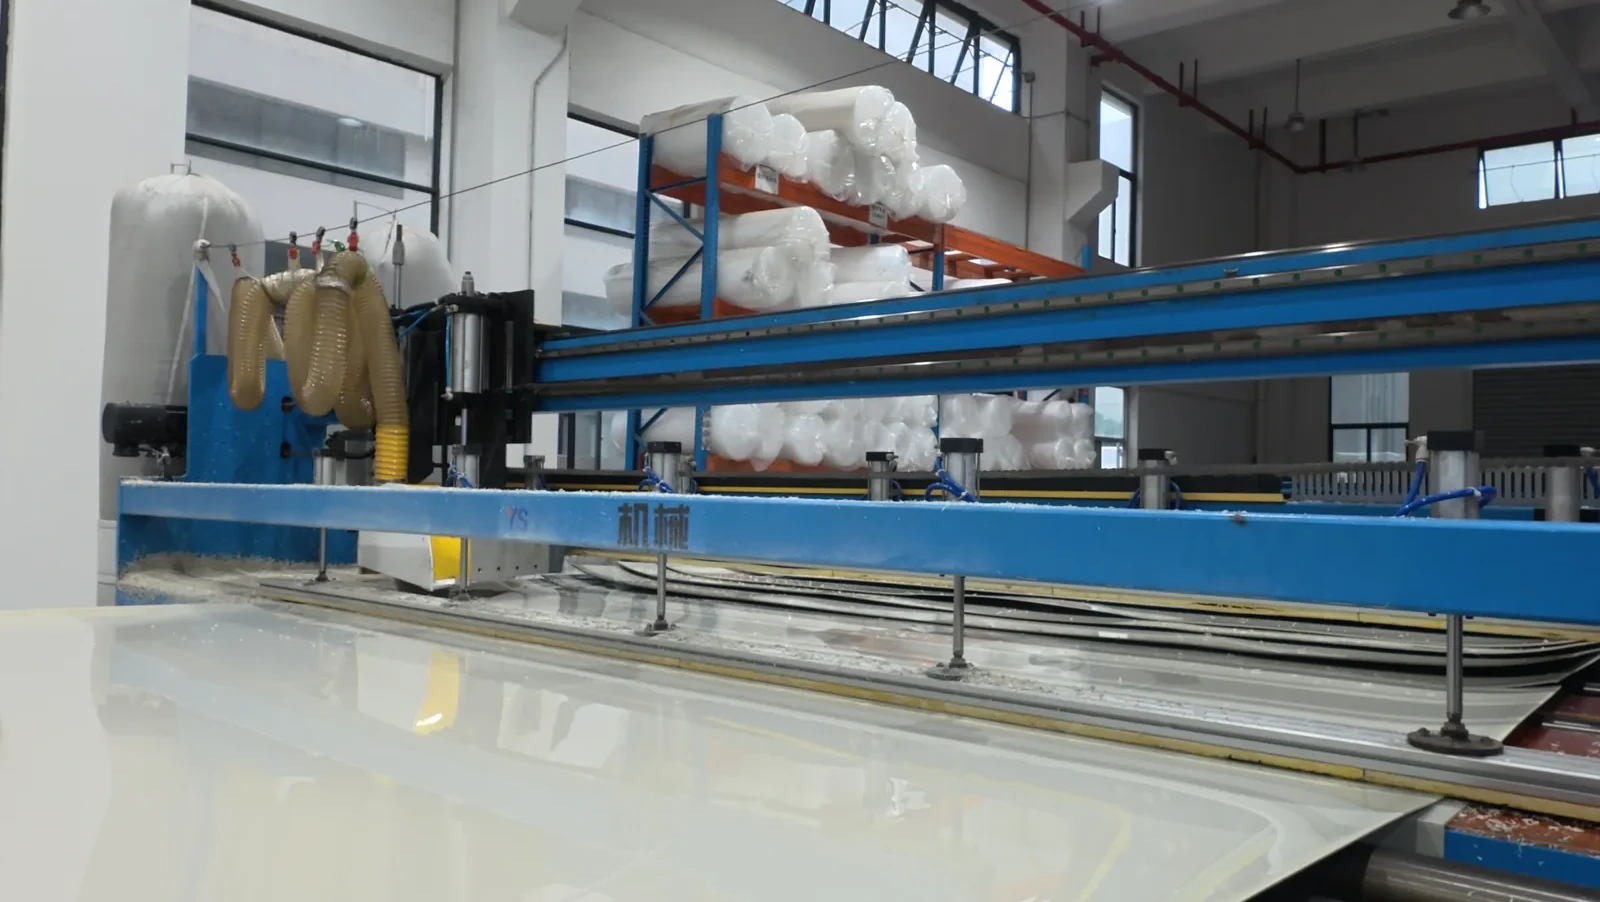
Referência em vídeo: This QEEHUA production video provides limited PP sheet manufacturing context for material preparation. It does not demonstrate semiconductor wet-process operation, PP screen performance, or equipment compliance.
Perguntas frequentes
Is a PP semicon screen the same as a rated filter?
No. A perforated or slotted PP screen component should be described by its project-approved geometry and process function. Do not assign filtration performance unless the responsible process design defines and validates it.
What must be provided before a PP screen pattern is fabricated?
Provide the approved drawing or pattern file, component function, overall geometry, chemical-duty record, support and interface details, and the equipment access requirements.
Can a generic PP perforated panel be substituted for a wet-process screen?
Not without project review. The aperture layout, border, supports, process role, chemical duty, and equipment interfaces must match the approved component requirement.

