
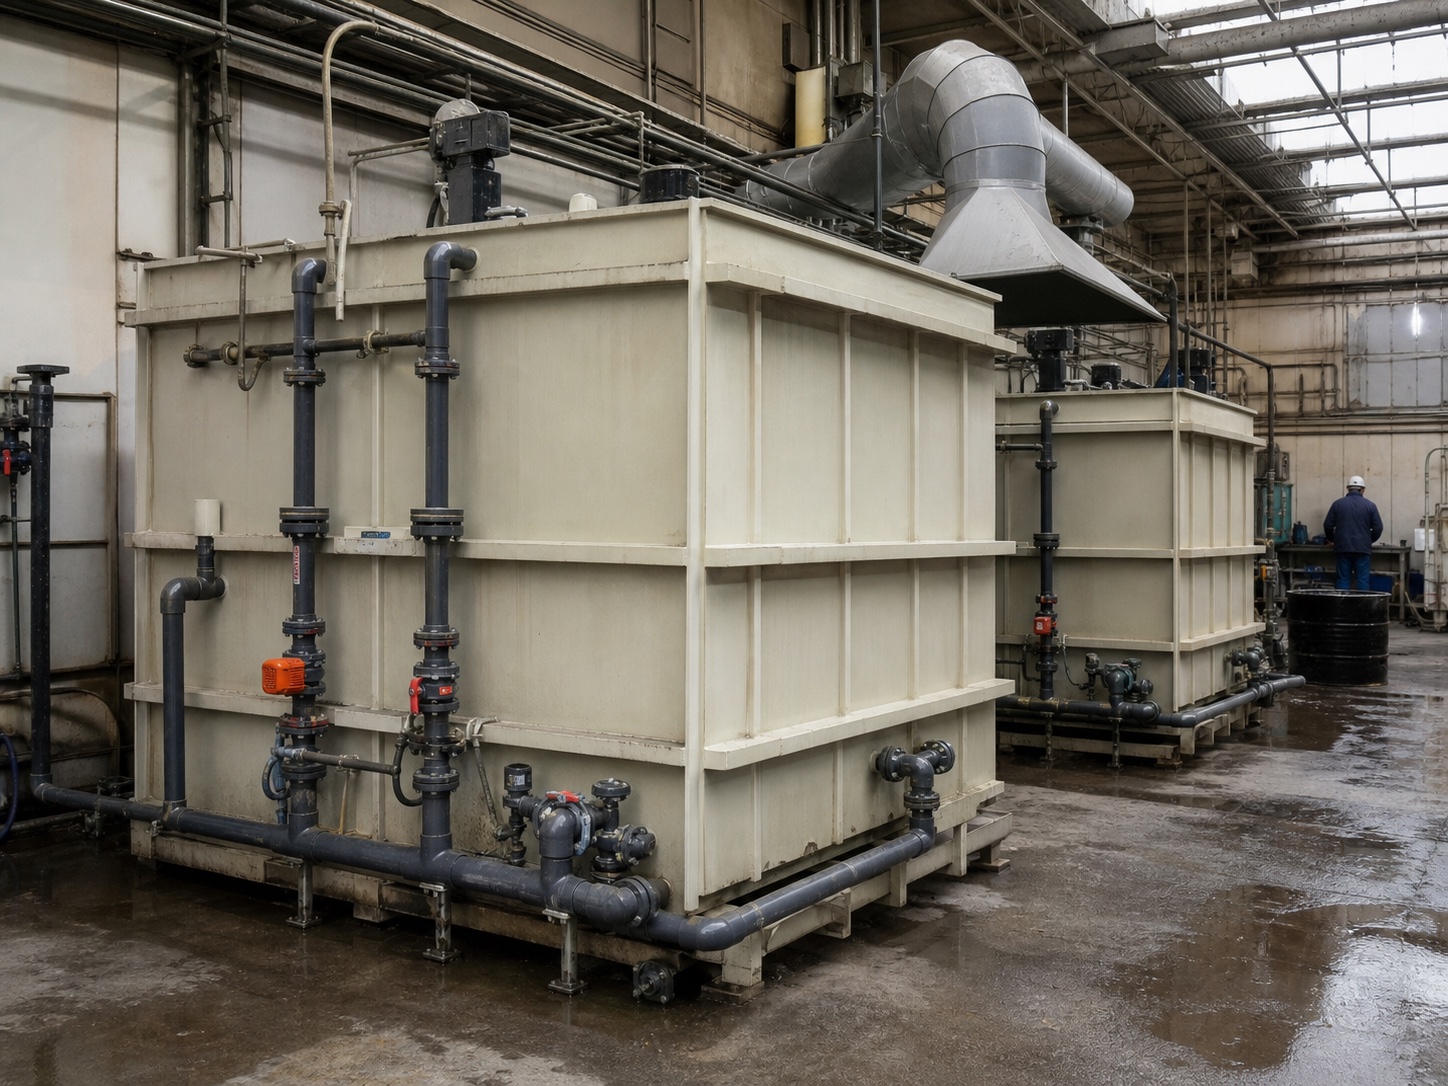
A PP tank cover specification should define the tank drawing, access needs, openings, support detail, chemical service conditions, and planned fabrication method. It can protect or close an approved equipment opening, but it does not establish tank-wall design, ventilation performance, containment capacity, or chemical suitability without project-specific confirmation.
This guide covers removable cover details rather than the broad selection of a chemical tank.
PP tank cover specification: start with the cover function
Specify whether the cover is intended to provide personnel protection, reduce splash exposure, support a process connection, close a non-pressurized opening, permit periodic inspection, or provide a removable interface for maintenance. One cover may have more than one function, but each function changes the drawing, support, access, and inspection requirements.
QEEHUA PP sheet is used in chemical equipment, wastewater and exhaust-treatment applications. For chemical service, the medium, concentration, temperature, cleaning process, and operating environment must be reviewed for the specific project before material suitability is confirmed.
Define the drawing interfaces before fabrication
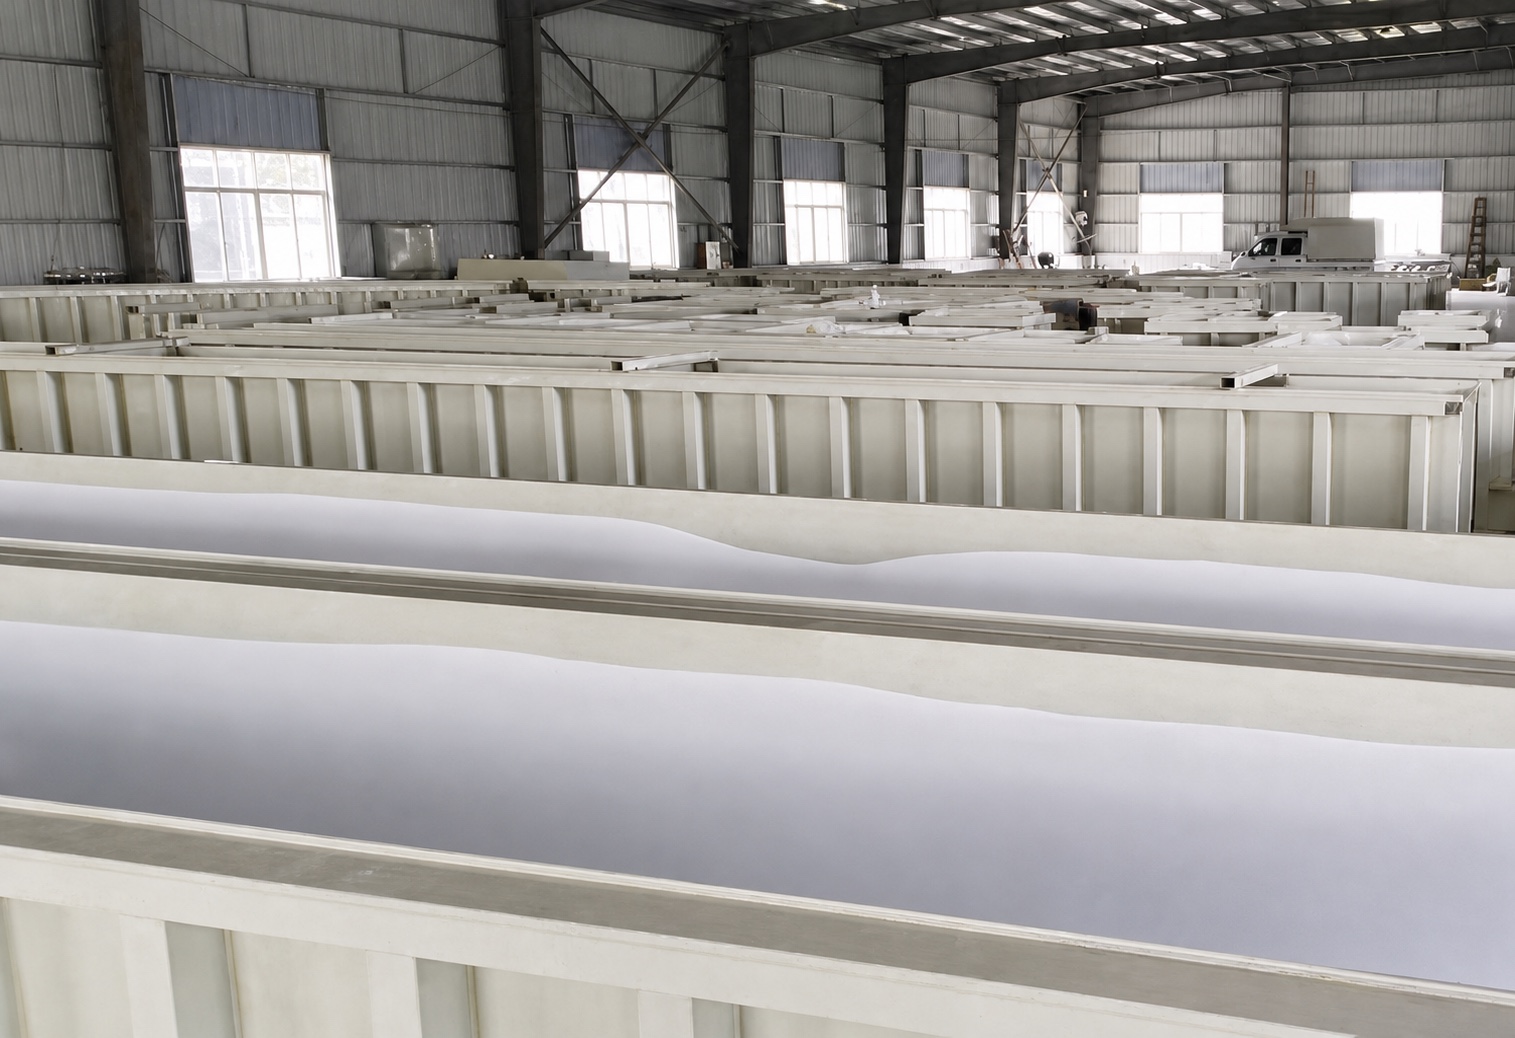
A useful RFQ identifies the tank opening, cover outline, planned overlap or seating detail, supports, removable sections, penetrations, inspection ports, flange or pipe interfaces, and any lifting or handling point. Mark which dimensions are controlled by the tank and which are controlled by the cover assembly.
- Tank drawing number, revision, opening geometry, and cover tag.
- PP sheet material callout, thickness specified by the approved design, and colour if relevant to the project.
- All cut-outs, nozzle locations, inspection openings, hinges, handles, or removable panels.
- Support points, clearances, alignment requirements, and access needed to remove the cover safely.
- Fabrication route, joint preparation, welding access, and required inspection records.
- Service medium, concentration, temperature, external exposure, cleaning conditions, and project acceptance criteria.
O Lista de verificação para solicitação de cotação (RFQ) de tanques PP helps set the tank-level inputs, while the PP welding-joint preparation guide helps identify fabrication details that should not be omitted where the cover is welded or includes welded interfaces.
Use material test data within its limits
A cover is one application within the broader PP sheet material, fabrication, and application decision. The local thermal results below can help a project team identify the material evidence being reviewed, but they do not establish a cover’s installed temperature limit, geometry, lifting method, or chemical suitability.
| Local PP sheet datum | Test method | Recorded result | Review boundary |
|---|---|---|---|
| Temperatura de deflexão sob carga | ASTM D648-18 | 137,0 °C | Test result for the stated method; not a cover service-temperature approval |
| Vicat softening temperature | ASTM D1525-25 | 155.2 °C | Material softening datum; not an installed-component rating |
| Módulo de tração | ASTM D638-22 | 1820 MPa | Material datum; not a cover-support calculation |
QEEHUA’s local knowledge base keeps PP sheet data and PP welding-rod information as separate product records. Use that separation when reviewing evidence. A sheet result can support the identity or stated property of the sheet material it covers, while a welding consumable record addresses a different input. Neither record automatically proves the performance of the finished cover, its joints, its installed interfaces, or its chemical suitability in a specific service.
In the RFQ, ask for the document reference, material identity, and the project condition to which the evidence is being compared. Keep any chemical, temperature, loading, or regulatory decision with the project approver. This makes the internal material record useful without extending it beyond its demonstrated scope, and it avoids treating a generic PP label as a substitute for a controlled cover design.
Material documents can support a PP-sheet submittal, but a flexural or tensile value for a specimen is not a structural rating for a finished tank cover. ASTM D790 covers flexural-property testing for plastics, and ASTM D638 covers tensile-property testing for plastics. Neither method replaces cover geometry, support, opening size, service conditions, or project engineering review.
Where the buyer needs records, list the requested document, applicable material, revision, and project acceptance route in the RFQ. The Lista de verificação para envio de material em chapa de PP is a useful companion for that documentation step.
Plan access, handling, and inspection together
A removable cover is only usable if operators can remove and replace it without conflicting with adjacent pipework, guardrails, supports, instruments, or maintenance space. Put lifting points, handles, removable seams, and assembly sequence on the drawing. If a project needs an inspection or fit-up trial, state it before the production lot begins.
The video below gives limited context for completed PP components after cutting. It does not demonstrate a tank-cover installation or determine the correct cover support detail.
Referência em vídeo: PP Sheet Finished Products After Cutting | QEEHUA. It shows general finished PP components after cutting; it does not verify tank-cover support, sealing, chemical duty, or installation requirements.
Acceptance checks in the PP tank cover specification
Agree the checks before delivery so that the receiving team can compare the finished cover with the approved drawing. Typical checks include drawing revision, cover tag, overall shape, cut-out locations, accessible removal path, visible fabrication quality, interface fit-up, required material documents, packing, and labels. Any test or acceptance limit must be the one approved for the project, not a copied generic value.
When to request further engineering review
Escalate the cover detail when it must carry a significant load, span an unsupported opening, control a pressurized process, support piping or equipment, provide a safety-critical barrier, or resolve uncertain chemical exposure. These conditions require a project-specific review beyond a PP sheet RFQ.
For a drawing review, entre em contato com QEEHUA with the tank drawing, cover function, service conditions, interfaces, and required records.
Perguntas frequentes
Can a removable PP tank cover be specified without the tank drawing?
No. The tank drawing is needed to define the opening, supports, penetrations, clearances, and removal path. A material description alone is not enough to establish a usable cover detail.
Does PP sheet test data define the load capacity of a finished tank cover?
No. PP sheet test data describes a material specimen under its stated method. Finished-cover capacity depends on the approved geometry, supports, joints, service conditions, and project engineering review.
What should be inspected when a removable PP tank cover is received?
Check the approved drawing revision, cover tag, dimensions and cut-outs, interface fit-up, access path, visible fabrication quality, required records, packing, and labels against the agreed inspection plan.

