
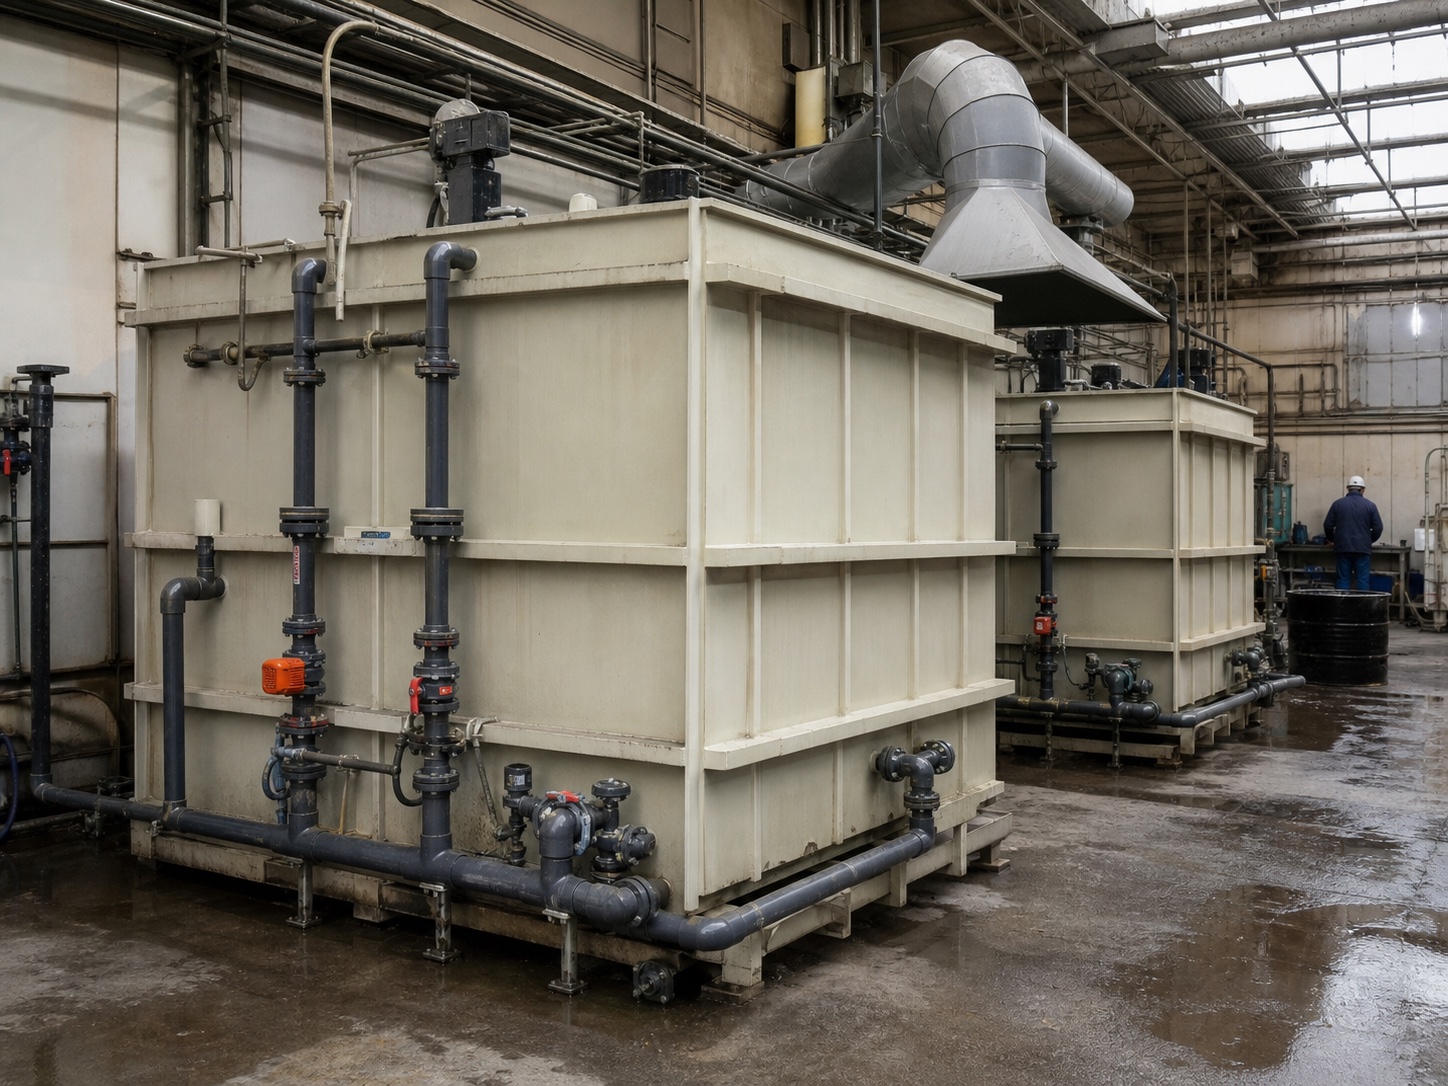
A chemical storage area needs enough drum spill pallets to separate incompatible liquids, hold every active drum position, and keep receiving and decanting work outside the normal storage footprint. Start with the drum inventory and each pallet’s verified usable capacity; do not choose a count from a generic rule of thumb.
That distinction matters because a tidy pallet layout can still fail operationally: a newly received drum may be left on the floor, an incompatible liquid may share a containment area, or an empty pallet may not be available when a leak is discovered. The existing Контрольный список покупателя поддонов для сбора пролитой полипропиленовой жидкости helps with product review; this article focuses on deciding the quantity and locations before an RFQ is issued.
Build the count from the maximum simultaneous drum inventory
Use the highest number of drums expected to be present at one time, not an average monthly purchase quantity. Include full drums, partly used drums, returns awaiting collection, and material staged for an active process. Exclude only locations that are genuinely outside the storage scope and controlled by a different containment arrangement.
| Input to record | Why it changes the pallet count |
|---|---|
| Drum size and closure condition | It affects the usable footprint and the containment case that must be assessed. |
| Maximum simultaneous drums | It is the starting quantity for each storage zone. |
| Verified pallet capacity | Use the supplier’s approved drum configuration, not a visual estimate of available space. |
| Receiving, dispensing, and quarantine locations | These often need their own positions because their contents and operating conditions change. |
| Liquid identity and compatibility | It determines whether drums should be separated into different zones rather than counted together. |
For planning only, use this transparent worksheet expression for each zone: pallet positions = ceiling(maximum simultaneous drums / verified drums per pallet) + dedicated operating positions. It does not size the sump, establish legal capacity, or replace a site risk assessment.
Separate zones before you calculate
Count each containment zone independently when liquids are incompatible, when one zone serves a different process, or when access controls differ. A receiving bay and a long-term storage row may have the same drum size but need separate pallet positions because they serve different stages of handling.
- Bulk storage: stable, labelled drums held for normal inventory.
- Receiving and inspection: newly delivered drums awaiting identification, condition checks, or transfer.
- Dispensing or decanting: drums used in routine operations, where drips and temporary hoses change the exposure scenario.
- Quarantine: leaking, damaged, unknown, or return material kept away from normal stock under the site’s procedures.
Check containment volume separately from pallet quantity
One pallet position is not automatically one compliant containment system. In the United States, the containment provisions in 40 CFR 264.175 apply to a defined hazardous-waste container-storage context and address an impervious base, drainage or liquid removal, capacity, run-on, and timely removal. The rule’s capacity test is 10% of the aggregate container volume or the largest container, whichever is greater, for that context.
That is not a universal instruction to buy a fixed number of spill pallets. The U.S. EPA also explains that secondary containment obligations vary with facility status and the material being managed; confirm the applicable authority, permit, local fire requirements, and site procedures before treating a federal example as your design basis. See the EPA’s TSDF secondary-containment guidance.
Keep operating space out of the storage calculation
Do not assume that a spare corner in the storage row will always be available for a delivery, a damaged drum, or a pump change. Mark dedicated positions on the layout for receiving and dispensing if those activities occur. If a project includes tanks, transfer points, or fabricated interfaces in addition to drums, capture them in the same scope document used for the PP tank RFQ so the containment boundary is clear.
Turn the count into a useful pallet RFQ
A quantity request alone leaves critical decisions unresolved. Send the supplier a zone-by-zone table and identify the actual drum arrangement required on each pallet. If PP sheet construction is being considered, QEEHUA can review the material and fabrication request alongside the chemical, concentration, temperature, mechanical loading, weld access, and cleaning conditions. Chemical compatibility remains an application-specific confirmation.
The following production overview provides general PP sheet manufacturing context for a containment-pallet enquiry. It does not determine pallet quantity, containment volume, chemical compatibility, or regulatory compliance.
Видеоссылка: “Behind the Scenes: QEEHUA’s Premium PP Sheet Production” is a general PP sheet production overview only; use the documented drum inventory and containment basis to determine the pallet layout.
Your RFQ should include:
- drum sizes, maximum quantity in each zone, and required orientation;
- liquid names, concentrations, temperatures, and incompatibility separation rules;
- the applicable containment-volume basis and authority having jurisdiction;
- receiving, dispensing, quarantine, and drainage arrangements;
- access needs for forklifts, drum handlers, inspection, and liquid removal; and
- the material, welding, inspection, and acceptance information needed for a fabricated solution.
For a broader material-selection path, see the Руководство по выбору, изготовлению и применению полипропиленовых листов.. For enclosed storage arrangements, the chemical storage cabinet buyer checklist identifies separate cabinet-selection inputs that should not be mixed into a pallet count.
Часто задаваемые вопросы
How do I calculate the number of drum spill pallets required?
Calculate each storage zone separately. Divide its maximum simultaneous drum count by the supplier’s verified drum capacity for the pallet, round up, and then add dedicated positions for receiving, dispensing, quarantine, or maintenance. Verify containment volume and regulatory requirements separately.
Can different chemicals share one spill pallet?
Only when the site’s compatibility assessment and operating procedures allow it. Incompatible liquids, different handling stages, or different containment requirements should be separated into distinct zones before the pallet count is calculated.
Does the 10 percent containment rule determine how many pallets I need?
No. The 10 percent or largest-container test in 40 CFR 264.175 applies in a specific U.S. hazardous-waste container-storage context. It addresses containment capacity, not a universal pallet quantity. Confirm the rules and design basis that apply to your facility.
What information should I send with a spill pallet RFQ?
Provide the drum sizes and maximum zone quantities, liquid details, required containment basis, handling and access plan, drainage arrangement, and any material or fabrication acceptance requirements. This lets the supplier assess the requested layout rather than guess from a total drum number.
Need a zone-by-zone containment layout review?
Send your drum inventory, liquid list, handling flow, and required containment basis. QEEHUA can help structure the PP sheet and fabrication information needed for a project enquiry.

