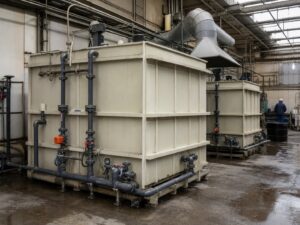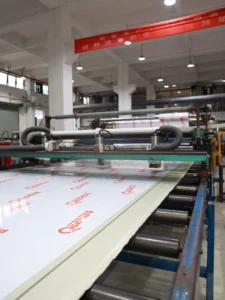
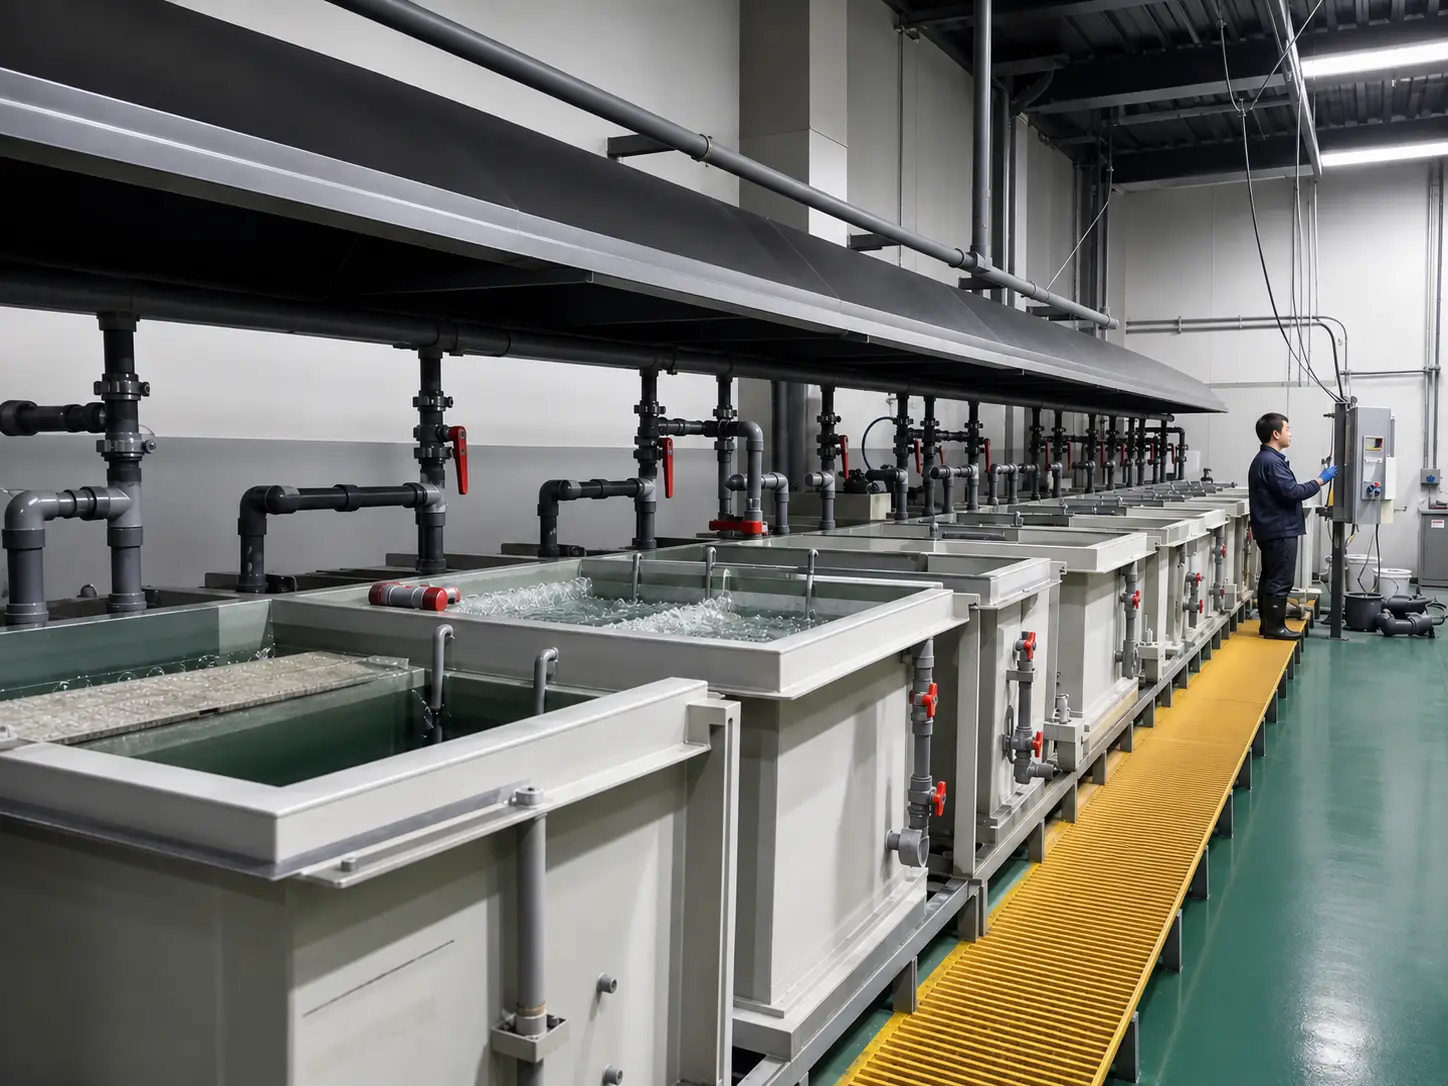
Anti-static PP sheet for electroplating tank areas should be specified as an equipment requirement, not simply ordered by name. Define the part, chemical duty, electrical behaviour, test method, grounding interfaces, fabrication details, and acceptance records before selecting a grade. This keeps a static-control request separate from ordinary PP sheet selection.
Start with the electroplating area and the part’s job
Ask where the sheet will sit before choosing a grade. A removable splash panel, tank cover, enclosure panel, equipment guard, cabinet liner, or fabricated tank component can have different chemical contact, cleaning, mechanical, electrical, and inspection requirements. The same is true when the component touches a process area versus when it only forms an external guard.
For the wider material-and-equipment framework, start with the PP Sheet selection and fabrication hub. For chemical-duty questions specific to tanks, review PP sheet selection for electroplating tanks by chemical duty before turning a static-control request into a purchase order.
Seven RFQ checks for anti-static PP sheet
| RFQ check | What the buyer should define | Por qué cambia la decisión |
|---|---|---|
| 1. Component and location | Name the finished part, equipment tag, drawing revision, and whether it is inside, beside, or remote from the process area. | Static-control needs belong to the finished equipment context, not only to a material label. |
| 2. Required electrical behaviour | State the project requirement for anti-static, static-dissipative, or conductive behaviour and the required acceptance band. | These terms should not be treated as interchangeable without a project criterion. |
| 3. Test basis | Specify the method, sample condition, measurement location, environmental conditioning, test voltage where applicable, and report format. | Resistance results depend on how the specimen is prepared and measured. |
| 4. Process duty | Record chemical, concentration, operating and cleaning temperatures, contact time, splash or immersion exposure, and ventilation conditions. | Electrical behaviour is only one part of a material-and-equipment review. |
| 5. Grounding and bonding interfaces | Show the approved interface, fasteners, conductive path, excluded scope, and responsible design party. | Material selection does not replace the electrical design of the installed system. |
| 6. Fabrication definition | Provide thickness target, cut features, bends, welds, supports, tolerances, visible faces, and edge condition. | The fabricated part can introduce interfaces and inspection points not visible in a sheet-only request. |
| 7. Acceptance and traceability | Define sample approval, material identification, electrical test record, visual inspection, packing, and release documents. | The supplied material and the accepted component should be traceable to the same requirement. |
Specify a measurement method, not only a resistance number
Surface-resistance data should be requested with the test context. The ESD Association’s ANSI/ESD STM11.11-2022 identifies test procedure, equipment, sample preparation, and conditioning as inputs to reproducible planar-material surface-resistance measurements. Your RFQ should identify the project-approved basis rather than copying a number from an unrelated part.
ASTM D257 likewise describes direct-current resistance and conductance measurements and notes the influence of test conditions and surface contamination. Treat a reported result as evidence for the stated specimen and method, not as a blanket approval for every finished panel or installation.
Where QEEHUA modified PP sheets fit
QEEHUA’s Láminas de PP modificadas page identifies an Antistatic Series AS-10 with a stated surface-resistivity range of 106–1011 Ω and a stated charge-decay time below 2.0 seconds. The same page identifies a Conductive Series EC-01 with stated surface resistivity below 106 Ω and an instantaneous charge-decay statement. These are product-page starting points for a technical discussion; the project must still confirm the applicable series, test method, conditioning, sample, finished-part design, and acceptance criterion.
Do not substitute an anti-static or conductive sheet specification for hazardous-location engineering. Where a process area is classified, the responsible project team must determine the area, equipment, wiring, and installation requirements. OSHA’s hazardous-location rule illustrates that electrical equipment and installations must be suitable for the classified location; a sheet alone is not an explosion-proof approval.
Keep chemical duty, fabrication, and static control in the same review
An electroplating request can fail when these decisions are separated. The material route needs the actual liquid or vapour duty; the fabrication drawing needs joint and support details; the electrical package needs the required behaviour and interfaces. The supplier quotation should reference the same controlled drawing and the same acceptance boundary.
For an underlying PP material discussion, consult the QEEHUA PP Sheets product page. For the material-document questions that belong beside a fabricated part, use the Guía de fichas técnicas de hojas de PP. Neither link replaces the responsible engineer’s review of the completed equipment.
What to send with the enquiry
- Finished-part description, location, drawing revision, quantity, dimensions, and thickness target.
- Anti-static or conductive requirement, required resistance range, method, conditioning, test points, and report format.
- Electroplating-process information needed for the component’s chemical and cleaning review.
- Grounding or bonding interface drawing, plus clear confirmation of which party owns the installed electrical design.
- Cutting, welding, machining, visual-face, tolerance, packing, and material-identification requirements.
- Sample, first-article, inspection, and release requirements before series fabrication.
Referencia de vídeo: Behind the Scenes: QEEHUA’s Premium PP Sheet Production. It offers a general view of PP sheet production activities; it does not verify anti-static or conductive performance, chemical compatibility, or electroplating-area controls.
Preguntas frecuentes
Does anti-static PP sheet make an electroplating area explosion-proof?
No. An anti-static or conductive sheet is a material-selection input. Hazardous-area classification, equipment approval, wiring, grounding, installation, and operating controls must be confirmed for the actual project by the responsible parties.
What resistance information should be included in an RFQ?
State the required acceptance range, the measurement method, sample preparation, conditioning, test points, and report format. Do not rely only on a generic resistance number because the measured result depends on the stated test basis and finished-part context.
How do anti-static and conductive PP sheet requests differ?
They should be treated as different project requirements. QEEHUA identifies separate Antistatic Series AS-10 and Conductive Series EC-01 product routes; select the route only after the required electrical behaviour, test basis, component design, and acceptance criteria are defined.
Should grounding details be part of the PP sheet supplier’s scope?
The RFQ should show every required grounding or bonding interface and name the responsible design party. A sheet supplier can review the requested material and fabrication scope, but the installed electrical design and compliance decision belong to the responsible project team.
General technical and procurement guidance only. Final material suitability, chemical compatibility, ESD-control design, grounding, electrical classification, fabrication design, and regulatory compliance must be confirmed for the documented project conditions.