
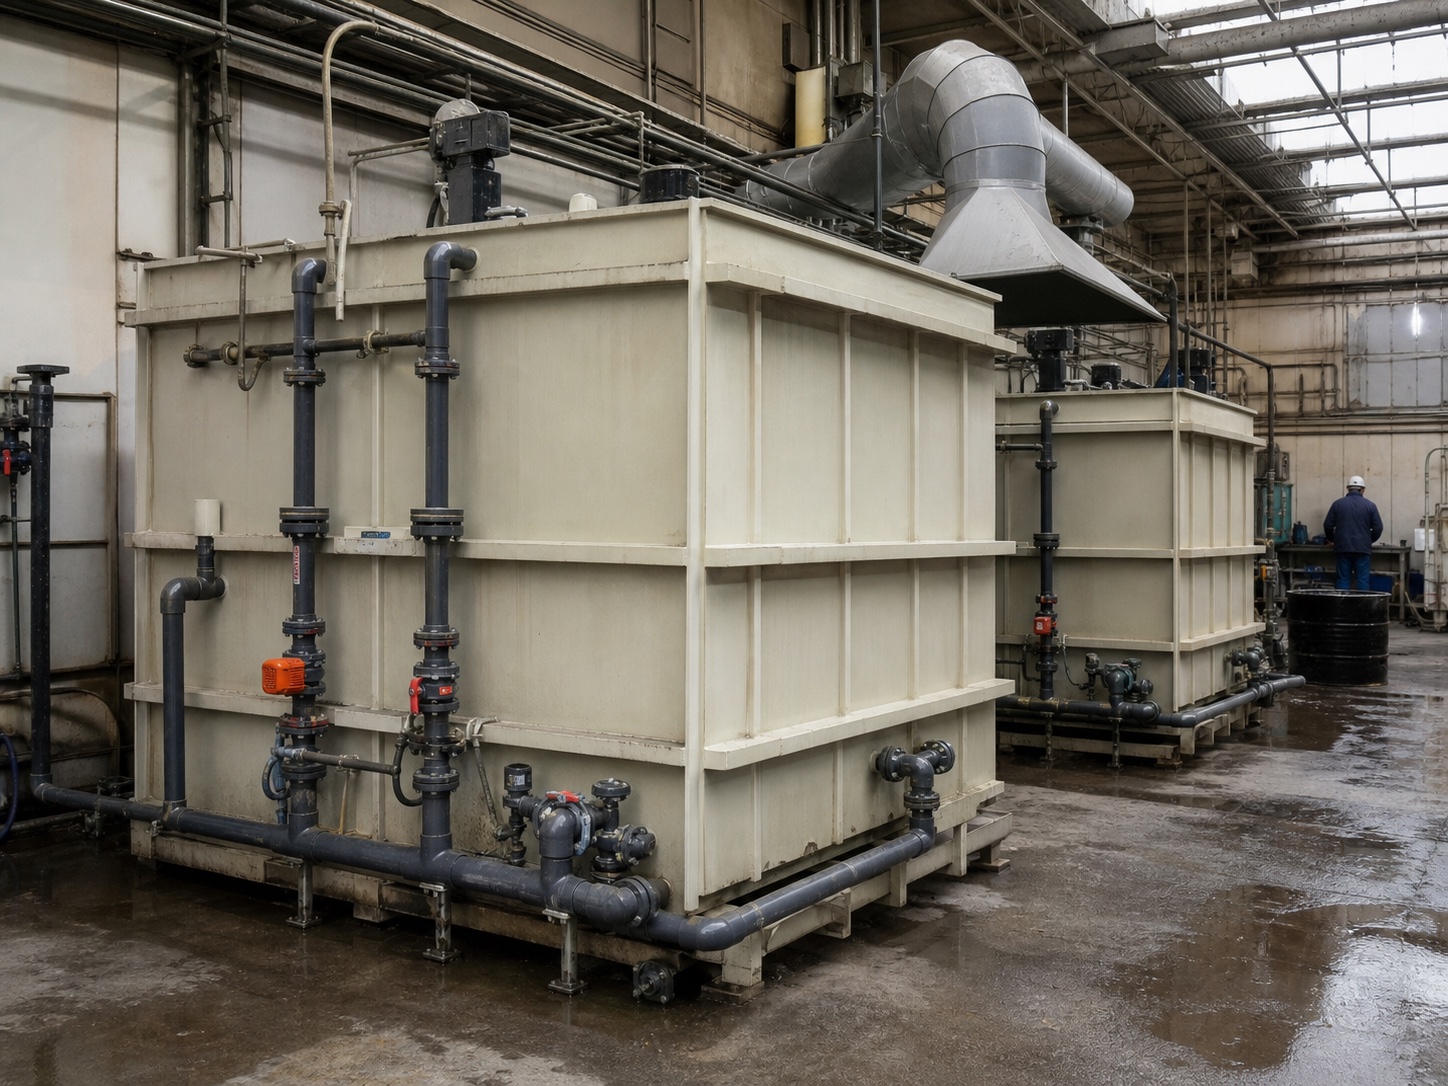
A PP chemical tank leak test record should identify the tank and drawing revision, service conditions, test boundary, approved method, preparation, result, defects or repairs, inspector, date, and release decision. It should connect the result to the weld map and handover dossier. Do not invent a universal pressure or hold time: the project specification, tank design, and approved inspection plan control acceptance.
What the PP chemical tank leak test record must prove before shipment
A pre-shipment PP chemical tank leak test record has two jobs. First, it shows that the specified test was completed on the correct fabricated tank. Second, it gives the receiving team enough context to understand the result and any limitations. A statement such as “tank tested OK” is too weak if it does not identify the boundary, medium, method, acceptance criteria, or unresolved scope.
For welded static, non-pressurised thermoplastic tanks, EN 12573-1 standard reference is useful context because it addresses general principles for workshop and site fabrication of tanks, including PP. It does not create one universal leak-test pressure or replace the project engineer’s approved test plan. Record the governing document and revision that actually applies to the order.
The same discipline applies to quality records. ISO guidance on documented information treats records as evidence of planned and completed work; in a PP tank handover, that means the form should preserve the decisions and observations needed for later review, not merely a signature.
Identify the tank, service, and drawing revision first
Start at the top of the form with the identity of the test object. The PP chemical tank leak test record should carry the same equipment tag used on the drawing, joint map, photographs, and packing list. This prevents a valid result from being attached to the wrong tank or an obsolete drawing.
| Record field | What to enter | Por qué es importante |
|---|---|---|
| Tank identity | Project, purchase order, equipment tag or serial number, customer, and fabrication location | Connects the test to one physical item and its shipment documents. |
| Design reference | Approved drawing number and revision, tank dimensions, nominal capacity, and scope boundary | Shows which geometry and interfaces were actually inspected. |
| Condiciones del servicio | Chemical or process duty, operating temperature range, liquid level, and any stated density or specific-gravity assumption | Explains the intended load and supports a project-specific compatibility review. |
| Fabrication traceability | Sheet grade and thickness, weld procedure revision, welding-rod identification, and joint-map reference | Lets the owner connect the leak result with material and weld records. |
| Test responsibility | Prepared by, performed by, witnessed by, and approval roles with dates | Separates the person who performed the test from the person who accepted the result. |
QEEHUA’s practical preference is to use one equipment tag consistently across the drawing, joint map, photographs, test sheet, packing list, and certificate folder. If a nozzle, cover, baffle, or support is outside the fabrication scope, state that exclusion on the same record rather than allowing a reader to assume it was tested.
Define the test boundary before filling, wetting, or closing the tank
“Leak test” is not a complete method. The record should show the part of the tank that was included and the temporary arrangements used to isolate it. Identify the shell, bottom, cover, nozzles, drains, overflow, baffles, liners, external trays, or connected pipework included in the test. Mark excluded openings and field connections on a sketch or annotated drawing.
List every temporary blank, plug, hose, sight point, level mark, or drain arrangement. Note whether the test medium contacted the final service surfaces and whether the tank was tested before or after accessories were fitted. A drain that is open during the test can be intentional, but it must be visible in the boundary definition.
Do not use a pressure-vessel form for a tank that was designed only for liquid head. A closed top, small nozzle, or temporary hose can create an unintended pressure or vacuum condition. The responsible engineer should approve the boundary and method before the test begins.
Record the approved method and acceptance criteria—not a generic number
The method section of the PP chemical tank leak test record should be specific enough that another competent person can understand what was done without guessing. Depending on the design and project specification, the approved check may involve a controlled liquid-fill observation, a visual examination, a low-risk functional check, or another defined method. The record should include:
- Method name, governing specification, drawing or inspection-plan reference, and revision.
- Test medium and its condition, including any chemical or cleanliness restrictions.
- Starting condition, level or exposure used, observation duration, and environmental conditions when relevant.
- Instrument or level-reference identification where an instrument is part of the approved method.
- Safety controls, temporary supports, exclusion zones, and drain-down precautions.
- Acceptance criteria stated in the project language: no visible leakage, no unacceptable deformation, or another defined requirement.
Never copy a pressure, vacuum, fill height, or hold time from another tank simply because the construction material is also PP. Geometry, thickness, reinforcement, nozzle loading, temperature, and service duty can change the safe method. If the purchase order is silent, place the test on hold and obtain a written engineering decision.
Capture pre-test condition and evidence while the setup is visible
Before starting, record that the tank was in a suitable condition for the approved test. Confirm that the intended welds are complete, accessible, and free from standing liquid or loose debris. Note the status of covers, fittings, supports, transport braces, temporary blanks, and any protective film that could hide a leak path.
Photographs are most useful when they are traceable. Use the equipment tag, joint or nozzle reference, and a date in the file name or image log. Take overview images of the test boundary and close-ups of unusual interfaces. Do not treat a photograph as a substitute for the signed result; it is supporting evidence that makes the record easier to audit.
Where the customer requires cleanliness, record the cleaning or rinse condition and the disposition of the test medium. For chemical service, the EPA secondary-containment reference is useful context for containment and transfer-area planning, but it does not define the leak-test method or release criteria for a fabricated PP tank.
Link observations, repairs, and retests to the joint map
If the result is acceptable, state the observed condition and the acceptance decision. If it is not acceptable, the record should become the starting point for a controlled nonconformance loop:
- Give the indication a unique NCR or observation number and locate it by seam, nozzle, corner, or grid reference.
- Describe what was observed, when it was observed, and whether the test was stopped or completed.
- Obtain an approved disposition and repair method before cutting, grinding, heating, or adding weld material.
- Record the repair area, materials and procedure used, responsible person, and photographs before concealment.
- Repeat the specified inspection or test, link the new result to the original record, and close the NCR only after approval.
This traceability is where the PP chemical tank leak test record becomes more valuable than a standalone certificate. The receiving team can see whether a “pass” was original, repaired and retested, or limited to a particular boundary. For broader weld-release checks, link the record to the PP tank weld inspection checklist and retain the same joint references in both documents.
Referencia del proceso: this QEEHUA clip shows a tensile-strength verification process for PP sheet. It is useful when discussing material and production traceability alongside a tank test, but it does not establish a tank leak-test method or acceptance result.
Referencia de vídeo: PP Sheet Tensile Strength Test | QEEHUA Lab Quality Verification. The clip is a general material-verification reference, not a fabricated-tank leak-test procedure.
Assemble a handover package that can be reviewed after shipment
The final PP chemical tank leak test record should sit inside a small, indexed dossier rather than in an isolated email attachment. A practical package can include:
- Approved drawing, revision history, equipment tag, and marked test boundary.
- Material and welding-rod identification, weld procedure, and joint or operator traceability.
- Pre-test condition checklist, photographs, test method, medium, observations, and signed result.
- Dimensional and interface checks for nozzles, drains, overflow, supports, covers, and lifting points.
- NCRs, repair records, retest results, and approval signatures.
- Cleaning, drain-down, packing, handling, and scope-exclusion notes for installation.
Utilice el PP tank RFQ checklist early in the project so the same inputs—service, dimensions, nozzles, supports, and acceptance documents—are available before fabrication starts. For material selection and fabrication context, the Guía de láminas de PP: Selección, fabricación y aplicaciones provides the wider decision framework. Neither page replaces the project-specific test approval.
A concise release checklist for the responsible reviewer
Before signing the shipment release, confirm that the answer to each question is visible in the dossier. Store the signed PP chemical tank leak test record with the final handover documents:
- Is the tested tank identified by tag, drawing revision, and scope boundary?
- Are service conditions and any design assumptions recorded?
- Is the approved test method named, with its medium, duration or level, and acceptance criteria?
- Are temporary blanks, drains, connected pipework, and exclusions documented?
- Can each observation be located on a joint map or annotated drawing?
- Are repairs, retests, and approvals linked to the original indication?
- Does the final signature distinguish fabrication completion from customer or engineering acceptance?
A complete PP chemical tank leak test record does not guarantee chemical compatibility, structural adequacy, or installation quality by itself. Those decisions remain controlled by the approved design, service data, responsible engineer, and project acceptance plan.
Preguntas frecuentes
Does every PP chemical tank use the same leak-test method?
No. The method depends on tank geometry, thickness, reinforcement, openings, service, temperature, and the governing project specification. Use the approved inspection plan and engineering decision rather than a generic pressure, vacuum, fill height, or hold time.
What should be identified before a PP tank leak test?
Identify the equipment tag, drawing revision, test boundary, included and excluded connections, test medium, temporary blanks or fixtures, approved method, acceptance criteria, and responsible people. This prevents a valid result from being attached to the wrong configuration.
Can a leak-test record replace a weld inspection report?
No. A leak-test record documents the specified test and its result. The weld inspection report should cover material and procedure traceability, joint-by-joint observations, dimensions or interfaces, repairs, and any other inspection required by the project. Link the records with the same joint references.
What should happen when a PP tank fails the test?
Stop or control the test as required, record the indication and location, issue an NCR or observation, obtain an approved repair disposition, document the repair, repeat the specified inspection or test, and close the issue only after the responsible reviewer accepts the retest.
Send the tank drawing, service conditions, test requirement, joint map, and desired handover format through the Página de contacto de QEEHUA. We can review the PP sheet and fabricated detail against the project requirement before shipment.

