
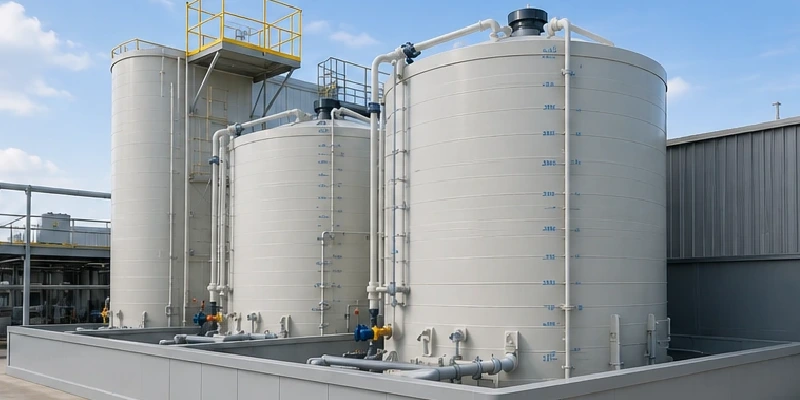
A PP sheet chemical bund lining can be a practical repair route when the stored chemical, concentration, temperature, exposure pattern, substrate condition, drainage layout, and weld access are known. It is not a universal cover-over solution: the repair must restore containment, remove the cause of the damage, and leave the bund inspectable and drainable.
When a Chemical Bund Should Be Re-Lined Instead of Patched
Re-lining is worth evaluating when deterioration is distributed across the floor or wall junctions, when repeated repairs have created uncertain interfaces, or when a new process duty calls for a more defined internal surface. A local patch may be enough for an isolated, understood defect; it is a poor substitute for a lining system when the source of leakage, chemical exposure, or drainage failure remains unresolved.
Start with an inspection record: map cracks, open joints, damaged coatings, penetrations, previous repairs, low points, sump connections, and areas that collect rainwater or washdown. Then separate structural questions from lining questions. A sheet lining can provide a contained internal surface, but it does not replace a structural assessment of the slab, retaining wall, supports, or settlement.
Define the Chemical Duty Before Selecting PP Sheet
Chemical compatibility cannot be confirmed from a product name alone. The chemical identity, concentration, temperature, contact duration, splash versus standing-liquid exposure, cleaning fluids, and any mixed or changing streams should be written into the repair enquiry. ASTM D543 explains why evaluation conditions must match the particular reagent, concentration, temperature, stress, and service exposure; it is a useful framework for defining the project test or evidence request.
QEEHUA PP sheet is used in chemical and environmental-protection equipment applications, but suitability for a particular bund must be confirmed against the project chemical duty. Do not approve a lining from a generic resistance chart, a short exposure result, or a material label alone. Ask for the current SDS, process description, operating and upset conditions, and any previous failure observations.
A PP Sheet Chemical Bund Lining Must Preserve the Containment Function
The lining design should be checked against the function of the whole bund: liquid retention, drainage or liquid removal, access for inspection, and interfaces with tanks, pipe supports, drains, curbs, and expansion or movement locations. For U.S. hazardous-waste container storage, 40 CFR 264.175 describes a base that is free of cracks or gaps, sufficiently impervious, and designed for collection and removal of liquids. It also includes a capacity rule for that regulatory context. It is not a universal design code, so the local authority, permit, site standard, and engineer of record remain controlling.
| Area to define | What the repair scope should state | Por qué es importante |
|---|---|---|
| Uso químico | Chemical name, concentration, temperature, exposure duration, cleaning agents, and upset conditions. | Material suitability is duty-specific. |
| Existing substrate | Defects, contamination, moisture condition, flatness, repairs, and areas that must be removed or rebuilt. | A lining cannot correct an unaddressed structural or moisture problem. |
| Sheet layout and joints | Panel map, upstands, corner treatment, seams, terminations, and permitted field adjustments. | The details control continuity at the places most likely to leak. |
| Interfaces | Pipe penetrations, drain/sump details, supports, tank feet, anchors, and access covers. | Interfaces often determine whether the finished bund remains inspectable and drainable. |
| Acceptance | Visual inspection, seam records, repair rules, hold points, and handover documents agreed by the project team. | Acceptance should test the approved scope, not an assumed material claim. |
Plan the Fabrication and Site Interfaces Before Panels Arrive
Specify whether the work is a shop-fabricated liner assembly, a field-fitted panel system, or a hybrid. The drawing package should show panel sizes, transport constraints, lifting and access paths, welding sequence, work clearances, pipe penetrations, vertical returns, and the order in which temporary supports or equipment will be moved. This is where the material scope connects with a PP equipment RFQ checklist and with the project’s existing inspection plan.
The following calibration-process video provides general PP sheet production context before lining panels are fabricated. It does not demonstrate site installation quality, leak-tightness, or suitability for a specific chemical bund.
Referencia de vídeo: “PP Sheet Extrusion: Haul-off and Calibration Process | QEEHUA” shows general haul-off and calibration context only; the re-lining design must still preserve the project containment function.
Where thermoplastic joints are part of the scope, record the approved joining method, operator qualification requirements, sample or coupon requirements if specified by the project, and the inspection method. The related guide on checking PP welding joints before shipment can help procurement teams turn a general request for “good welds” into reviewable acceptance points. The lining contractor and engineer should still define the site-specific criteria.
Seven Questions to Put in the Re-Lining Enquiry
- What chemicals, concentrations, temperatures, and exposure durations can reach the bund?
- What is the observed failure mode: cracking, coating loss, joint failure, contamination, settlement, or a drainage issue?
- What are the existing base, wall, sump, curb, drain, and penetration conditions?
- Which areas require continuous lining, vertical returns, removable covers, or special interface details?
- What access, lifting, shutdown, ventilation, cleaning, and work-permit constraints apply?
- Which local code, permit, owner standard, containment-capacity rule, and inspection records govern the work?
- What drawing, material, fabrication, seam-inspection, and handover evidence will be required before acceptance?
For a new containment asset rather than a repair, compare this scope with the existing Lista de verificación para compradores de paletas de contención de derrames de PP. Pallets and fixed bunds solve different storage problems, so their capacity, access, drainage, and inspection requirements should not be copied from one another.
The Procurement Decision
Use PP sheet for chemical bund lining only after the project team has made the duty and interface decisions explicit. A useful enquiry gives QEEHUA the chemical-duty information, the survey drawings or photographs, panel layout constraints, and the acceptance requirements; this allows the material and fabrication scope to be reviewed without assuming an unsupported thickness, chemical rating, or regulatory approval. For project-specific support, Contacto QEEHUA with the SDS, bund dimensions, existing-condition record, and required handover documents.
Preguntas frecuentes
Can PP sheet cover a cracked chemical bund base?
PP sheet may form part of a re-lining system, but a cracked base must first be assessed for its cause, extent, movement, contamination, and effect on the containment function. The project should not use a lining to conceal an unresolved structural, drainage, or substrate problem.
What information is needed to check PP sheet compatibility for a bund?
Provide the chemical name, concentration, temperature, contact duration, splash or standing-liquid exposure, cleaning chemicals, upset conditions, and the required service life or inspection plan. Material approval should be tied to those stated conditions.
Does a new liner remove the need to check bund capacity and drainage?
No. A liner is only one part of the containment system. Capacity, drainage or liquid removal, rainwater/run-on control, penetrations, inspection access, and applicable regulatory or owner requirements must be checked for the completed bund.
What should be included in a PP sheet bund-lining RFQ?
Include the chemical-duty record, survey drawings or photographs, bund dimensions, base and wall condition, pipe and drain details, access constraints, panel and joint layout expectations, required inspection records, and project acceptance criteria.

