PP sheet splash guards for acid pickling lines should be specified from the actual process zone, liquid and mist exposure, openings, supports, cleaning method, and ventilation interfaces. The sheet request is only one part of the project: the responsible team must still confirm material suitability, guarding, and the complete ventilation design.
Define the pickling-line zone before naming a material
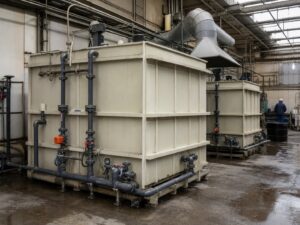
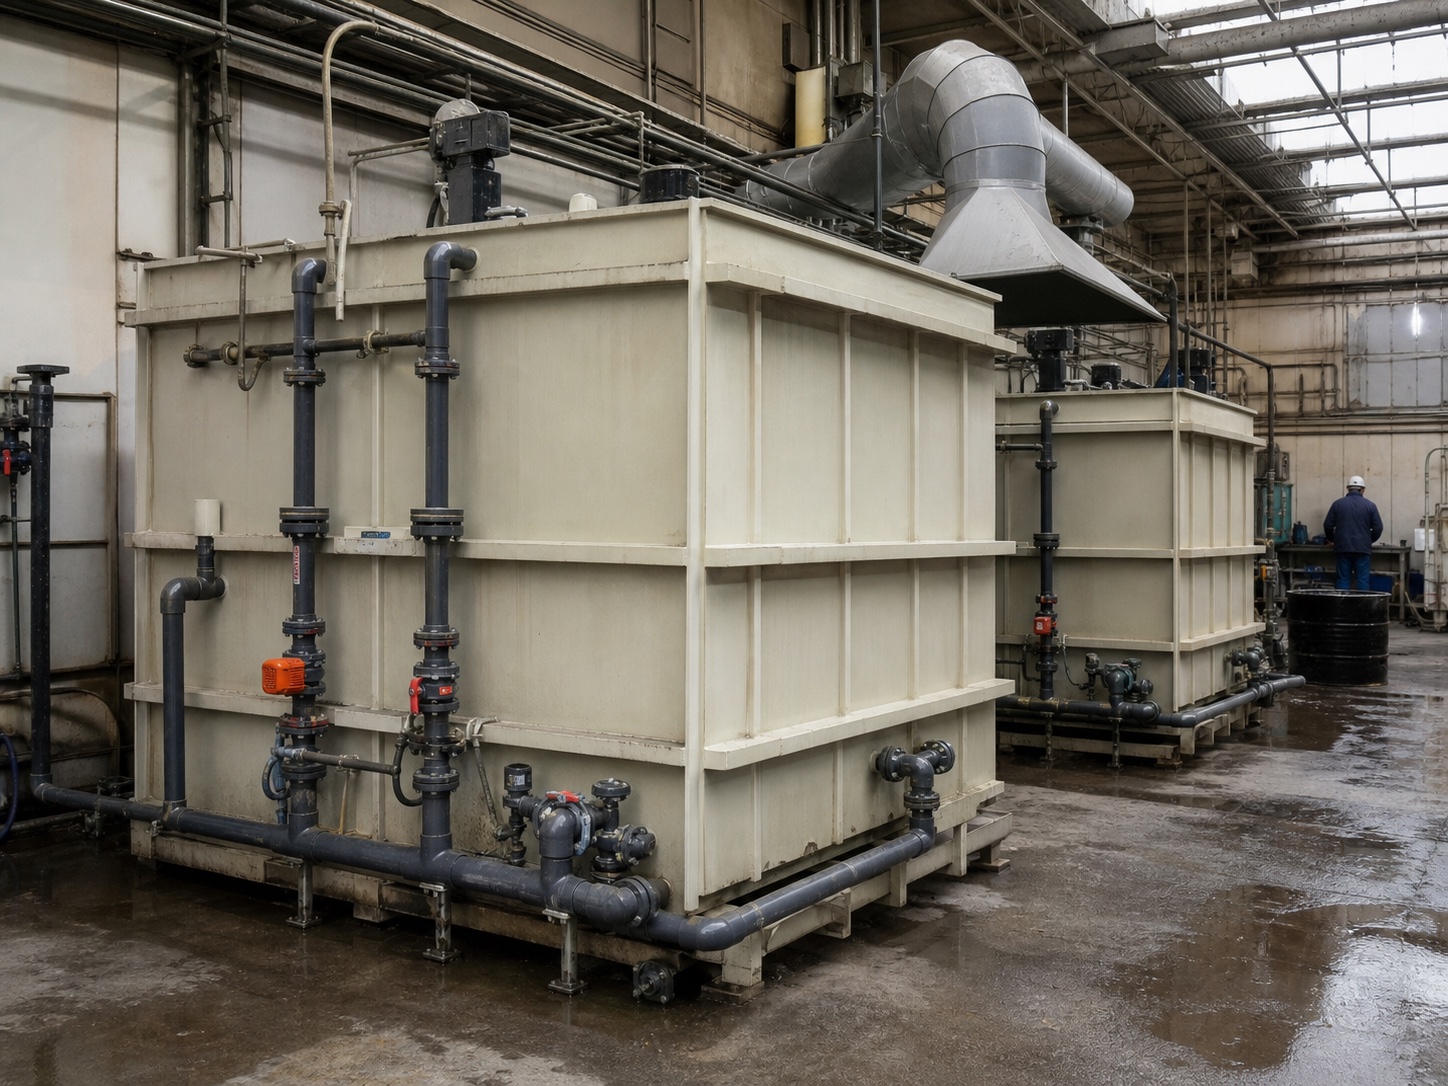
A splash guard beside an open pickling tank can see a different duty from a removable cover, a dry perimeter panel, a drip shield, or a panel at an exhaust opening. Record where the component sits, which face may contact liquid, condensate, mist, wash-down water, or cleaning chemicals, and whether the part is fixed or routinely removed.
For context, QEEHUA’s Arkusze PP page identifies industrial PP sheet options for chemical-storage and water-treatment applications, including standard 3-30 mm and extra-thick 40-100 mm formats. Those published ranges are product options, not a thickness instruction for a pickling-line guard. The component drawing, support arrangement, openings, and operating duty still determine what must be reviewed.
Seven RFQ checks for a PP splash guard
A usable RFQ makes the unknowns visible before material is released. The following checks separate a component request from an unsupported claim that one material solves the whole pickling-line risk.
| RFQ check | Co zapewnić | Dlaczego to ważne |
|---|---|---|
| 1. Component role | State whether the part is a side splash guard, removable panel, top cover, drip shield, divider, or enclosure panel. | Each role has different openings, access needs, joint details, and loads. |
| 2. Exposure map | Mark liquid-contact, splash, mist, condensate, wash-down, and dry faces on the drawing. | Exposure can vary across a single guard; a generic ‘acid service’ label is not enough. |
| 3. Process duty | Give the chemical names, concentrations, normal and maximum temperatures, dwell pattern, cleaning media, and credible upset conditions. | Material screening depends on the documented reagent and end-use conditions. |
| 4. Geometry and support | Include panel dimensions, cut-outs, free spans, edge returns, stiffeners, mounting points, and nearby equipment interfaces. | Panel geometry and supports affect the fabricated component; a material data value is not a design approval. |
| 5. Openings and maintenance | Show hand openings, viewing zones, access frequency, removal method, lifting points, and clean-out clearance. | These details determine where edges, joints, fasteners, and sealing interfaces need attention. |
| 6. Ventilation boundary | Identify any hood, slot, duct, capture opening, or makeup-air path adjacent to the guard. | The system designer must assess airflow and capture; a panel selection does not validate the ventilation system. |
| 7. Acceptance record | State the drawing revision, material request, required documents, visual checks, dimensional checks, and release authority. | A documented acceptance basis prevents an unverified prototype or substitution from becoming the production reference. |
Use a test basis that resembles the component’s real exposure
When chemical-resistance evidence is needed, match the evaluation to the component duty. ASTM D543 explains that chemical-resistance results depend on the reagent, concentration, contact duration, temperature, applied stress, and other end-use factors. It also distinguishes continuous immersion from short splash or spill exposure. That distinction is useful for a splash guard, but it does not replace project testing or a responsible engineer’s decision.
Use the current QEEHUA PP sheet data-sheet and fabrication guide to organize the material conversation. Then send the actual duty sheet and component drawing for confirmation. If the process contains proprietary additives, mixed acids, surfactants, or cleaners, name them or attach the relevant technical information instead of treating the base acid name as the whole exposure.
Keep splash guarding separate from ventilation design
A guard can be part of the physical arrangement around a tank, but it is not a declaration that emissions are captured or that worker exposure is controlled. OSHA’s open-surface-tank ventilation rule includes pickling among the covered operations and bases its treatment of tank operations on factors such as hazard potential and the rate of gas, vapor, or mist evolution. See OSHA 1926.57 for the regulatory context; the responsible designer must determine the applicable requirements for the project and jurisdiction.
For a nearby hood, duct, or capture interface, define the clear opening, flange or fixing detail, access requirements, expected deposits, and condensation path. QEEHUA’s chemical exhaust ductwork guide provides the related component-level framework. It should not be used to infer that a splash guard establishes airflow, capture, discharge, inspection, or compliance.
Specify the fabricated part, not only the sheet
Ask for a drawing or a controlled dimension list. Include outside dimensions, cut-outs, edge treatment, weld or mechanical joints, support method, seals, hardware, labels, and any interface with piping or a tank rim. A fabrication request should also say which party owns final fit-up and site installation.
Where the guard connects to process piping or other equipment, mark the no-go zones and service clearances so that the panel does not obstruct valves, drains, inspection tasks, or access. The PP Sheet selection, fabrication and applications hub provides the parent selection path; this article owns the narrower pickling-line splash-guard request.
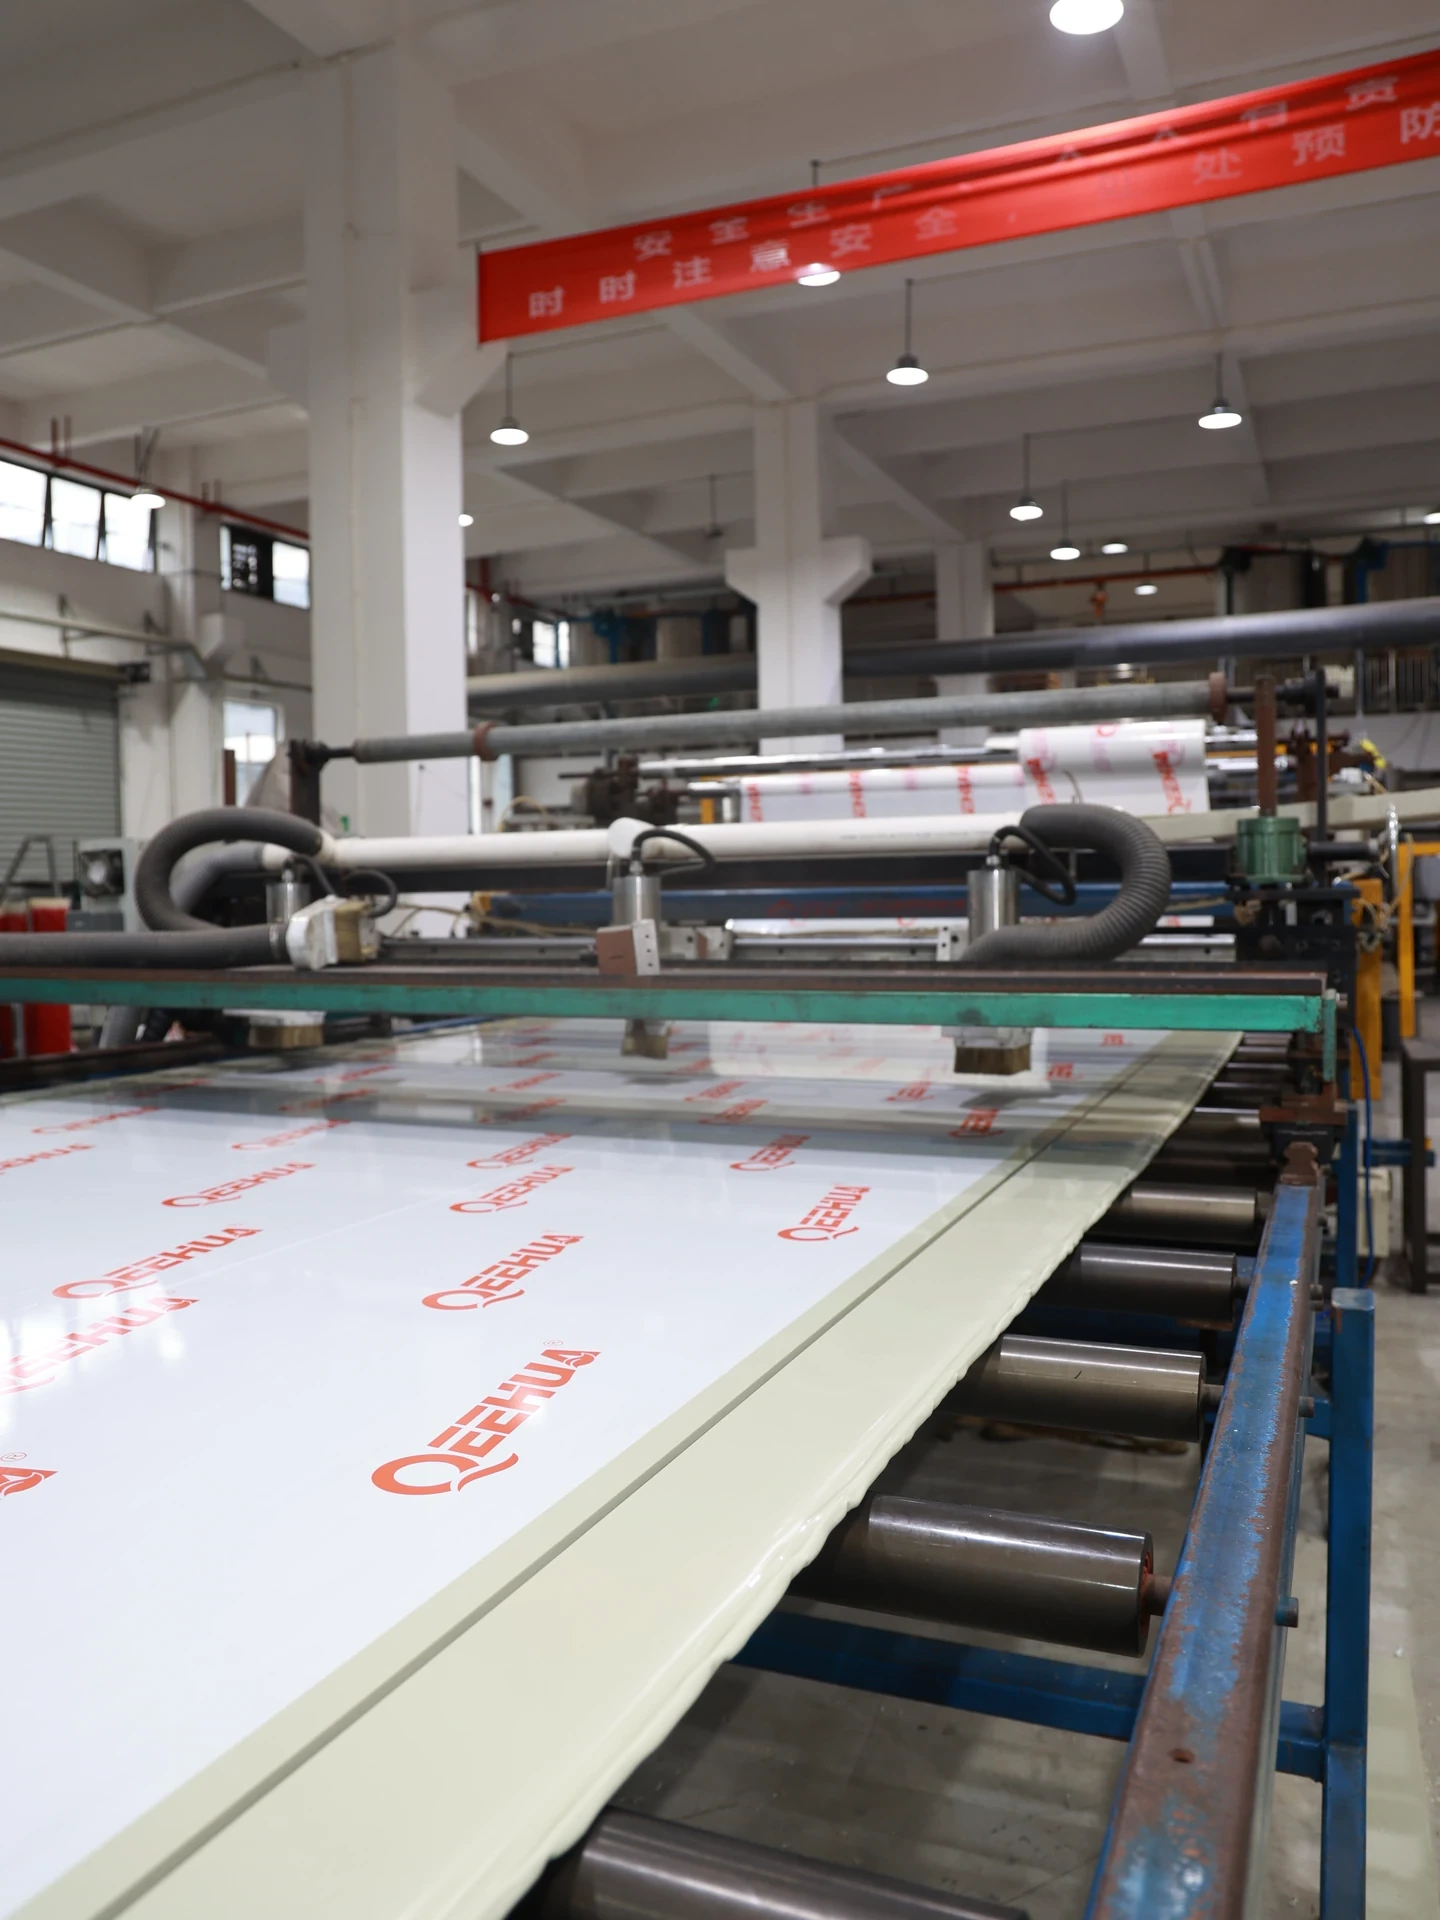
Fabrication video: panel-cutting context
This QEEHUA playlist video is relevant to the general cutting stage for fabricated PP sheet components. It does not demonstrate acid-pickling suitability, guard design, ventilation performance, or site acceptance.
Odniesienie do filmu: PP Sheet Cutting Process: Precision Cutting | QEEHUA. It shows a general cutting stage for PP parts; it does not determine acid exposure, splash-guard geometry, or pickling-line duty.
Prepare a clearer enquiry before release
Send the controlled drawing, the seven RFQ inputs above, the quantity, project location, target delivery date, and the required document list. QEEHUA can then review the request against the available PP sheet options without assuming the chemical duty or the ventilation design.
For broader equipment duty and material-screening context, see Jak wybrać folię PP do zbiorników na chemikalia i urządzeń procesowych. It is a related guide, not a substitute for the splash-guard drawing and pickling-line operating information.
Często zadawane pytania
Can a PP sheet splash guard replace local exhaust ventilation for an acid pickling tank?
No. A splash guard is one physical component. The responsible ventilation and EHS team must determine capture, airflow, discharge, inspection, and applicable requirements for the complete pickling-line system.
What process information should be sent with a PP splash-guard RFQ?
Send the chemical names and concentrations, normal and maximum temperatures, exposure map, cleaning media, component drawing, openings, supports, adjacent ventilation interfaces, quantity, acceptance checks, and required documents.
Can PP suitability be confirmed from the word ‘acid’ alone?
No. The actual reagent, concentration, temperature, contact pattern, stress, cleaning chemicals, and component role must be reviewed. Where the available evidence does not represent the project duty, record the item for project-specific confirmation.
Why should openings and mounting details appear on the drawing?
Cut-outs, free spans, mounting points, access frequency, seals, and nearby equipment interfaces can change the fabricated component and its inspection needs. They should be controlled before material release rather than resolved only at installation.