
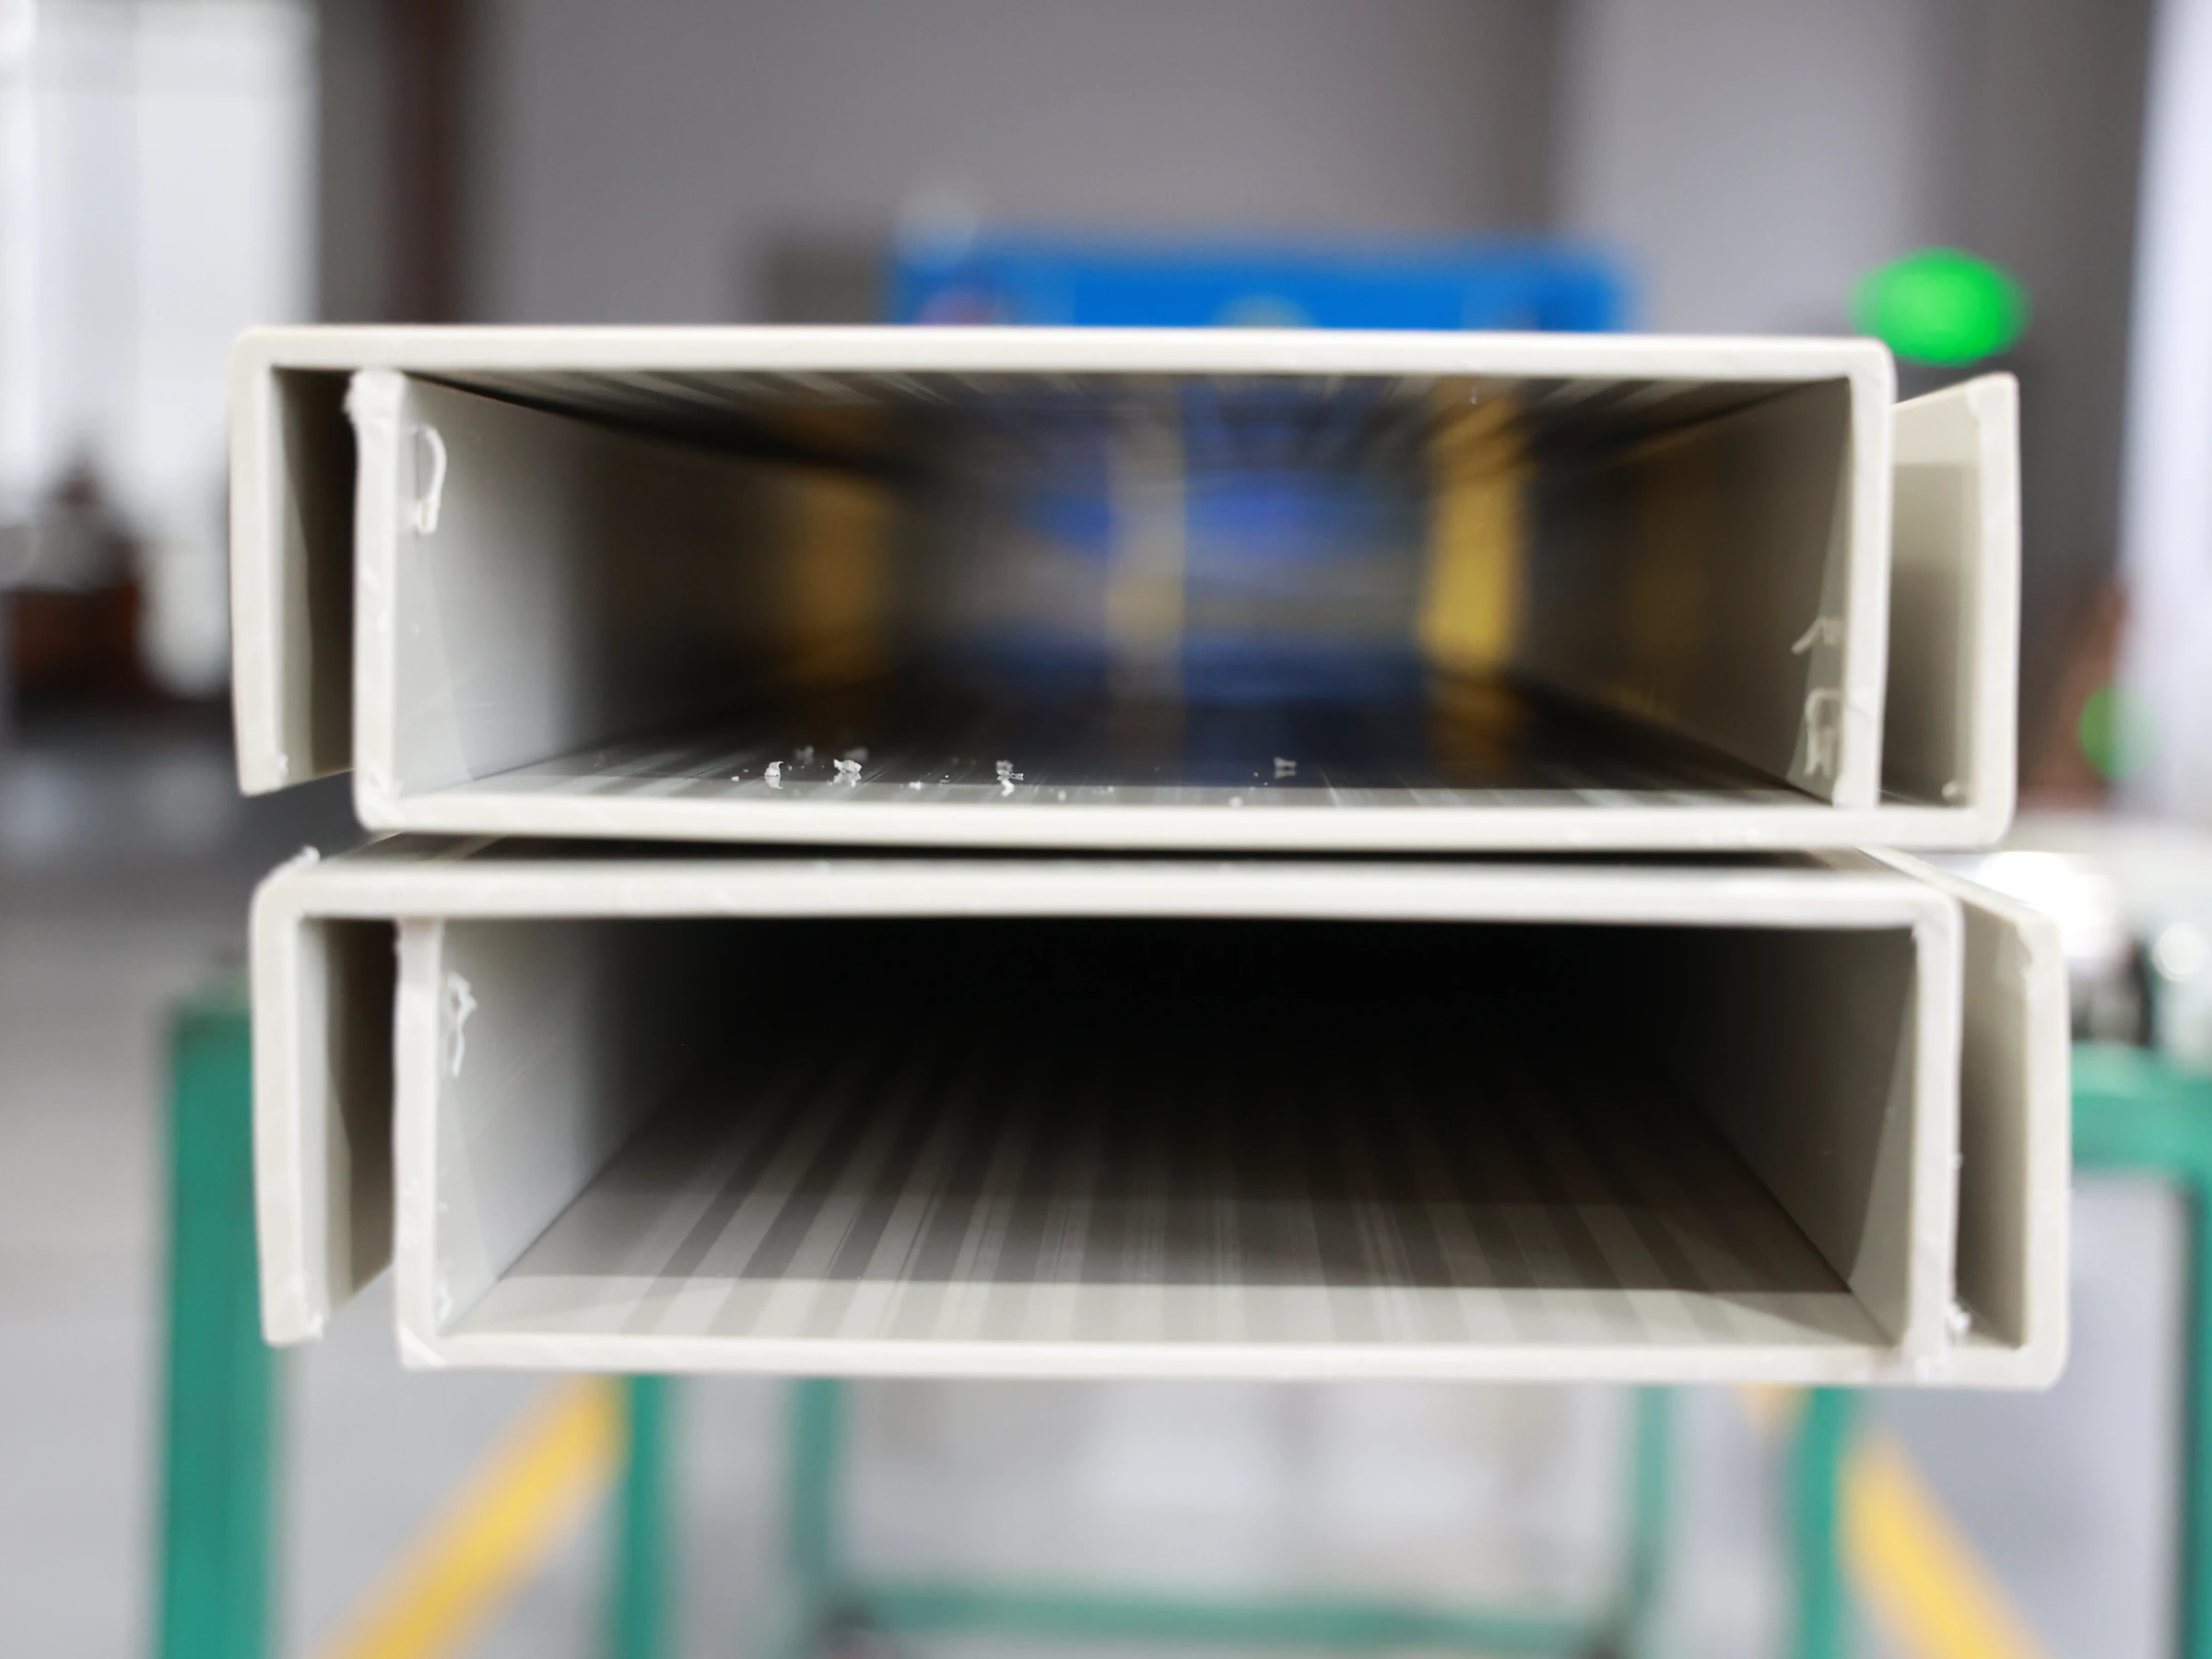
PP U-shaped channel reinforcement can help restrain and finish the edges of fabricated PP tank panels when its geometry, placement, weld path, and service conditions are defined with the panel design. It is not a substitute for tank-wall, support, or load calculations; those remain project-specific engineering decisions.
This article addresses how a PP profile can support a fabricated panel detail without blurring it with overall tank design.
When is a PP U-shaped channel the right reinforcement detail?
A PP U-shaped channel is useful when a fabricated panel edge needs a controlled finishing, locating, or restraining detail within an already defined equipment arrangement. Typical examples include the perimeter of a tank panel, a stiffened opening, a partition edge, or an equipment frame interface.
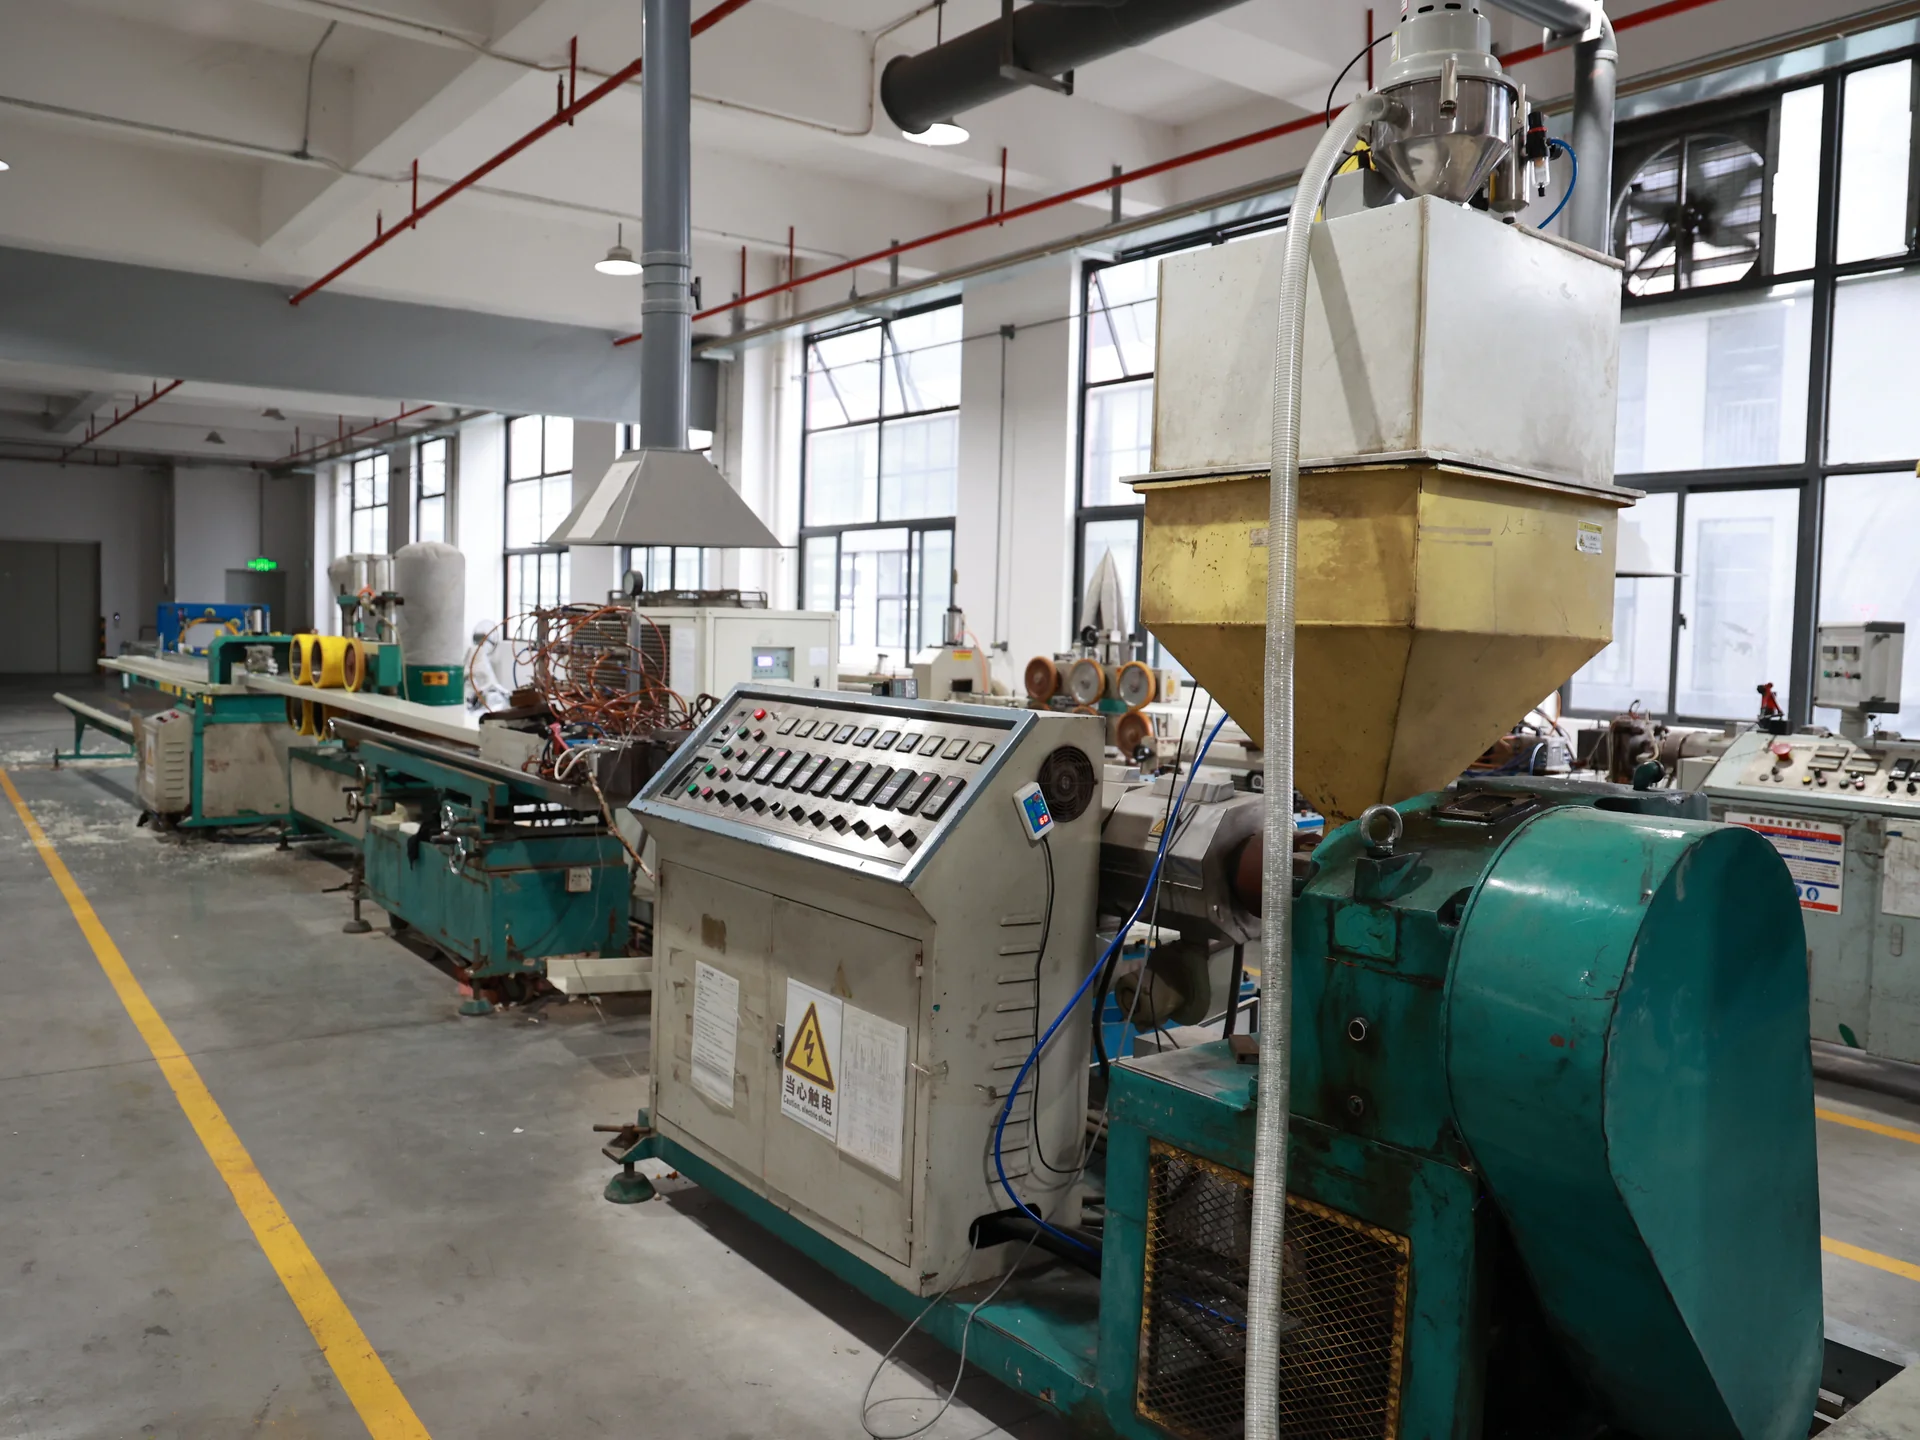
QEEHUA supplies PP profile extrusions, commonly described as U-shaped channels, as auxiliary materials for securing and reinforcing PP sheet equipment. The profile must be selected around the actual panel and interface, not from a profile name alone.
Start with the panel role, not the channel size
First identify what the channel is expected to do. An edge restraint, a frame connection, a local stiffener, and a protective trim can look similar in a drawing but require different information from the fabricator.
- Panel context: identify the panel location, span, adjacent supports, openings, and whether the edge is free, supported, or joined to another component.
- Load and movement context: identify the contained medium, operating conditions, handling loads, thermal movement, vibration, and any external attachments that affect the panel.
- Service environment: confirm the chemical, concentration, temperature, cleaning regime, and exposure conditions for both the sheet and the profile.
- Fabrication route: state whether the channel will be welded, mechanically retained as part of another approved assembly, or supplied as a cut-to-length component for later fabrication.
For equipment that will contain chemicals, the material selection still begins with the full service condition. The PP sheet chemical-tank selection guide is a useful companion for documenting medium and operating conditions before a reinforcement detail is finalized.
Define geometry and interface conditions on the drawing
A usable RFQ should show the panel thickness and edge condition, the required channel orientation, the continuous or intermittent length, corners and terminations, and every location where another component meets the profile. It should also distinguish a nominal profile dimension from the clear space required after fabrication tolerances are considered.
Do not assume that a channel which fits a loose panel sample will fit a welded panel assembly. Weld build-up, corner transitions, sheet flatness, cut quality, and access for welding all affect the detail. If a profile must receive a panel edge, request a drawing review or sample fit-up before a production quantity is released.
Use material data correctly
Before a profile geometry is released, the PP sheet material-selection and fabrication context needs to be read with this panel-specific detail. The property values below identify the tested sheet material; they do not establish a tank wall, support, channel, or joint design.
| Local PP sheet datum | Test method | Recorded result | Use in this review |
|---|---|---|---|
| Densidade | ASTM D792-20 | 912 kg/m³ | Mass estimate for a defined sheet volume |
| Teste de flexão | ASTM D790-25 | 1870 MPa | Material record only; not a panel-design load |
| Resistência à tracção | ASTM D638-22 | 30 MPa | Material record only; not a channel acceptance value |
For a flat-sheet handling estimate, use m = ρ × L × W × t, where m is mass in kg, ρ is density in kg/m³, and L, W, e t are finished dimensions in m. NIST defines mass density as ρ = m/V, which rearranges to this estimate. With the local density result, a 1.20 m × 0.60 m × 0.010 m panel estimates at 6.6 kg before machining, profiles, welds, tolerances, or installed supports are considered. It is a logistics estimate, not a structural calculation.
Material test data can support a submittal, but it does not create a structural rating for a finished tank panel or its U-shaped channel. QEEHUA PP sheet documentation identifies flexural and tensile test methods for the sheet material. For reference, ASTM D790 covers flexural-property testing for plastics, while ASTM D638 covers tensile-property testing for plastics.
Those methods are useful when a buyer asks which test framework is cited in a material document. They do not replace the project review of geometry, joints, supports, service medium, temperature, or allowable deflection. Ask QEEHUA to confirm the relevance of any requested material document to the specified PP sheet and profile before ordering.
Plan fabrication and inspection before the profile is cut
For QEEHUA fabrication documentation, keep the profile, sheet panel, and welding consumable traceable as separate line items even when they arrive for the same assembly. Record the drawing revision, panel tag, profile length, cut-list reference, and the approved joining route. This prevents a finished-looking channel from being accepted against an outdated panel revision or from being treated as interchangeable with a different edge detail.
Use the inspection record to close the same loop. Confirm that the channel position, end treatment, joints, and interfaces agree with the released drawing; then note any site-fit adjustment before the part leaves the shop. This is practical internal fabrication control, not a substitute for the project’s structural review. It gives the buyer and fabricator one auditable explanation of how the profile detail relates to the PP panel arrangement.
For welded equipment, the profile detail should leave clear access for the planned joint preparation, welding sequence, and inspection. The PP welding-joint preparation guide can help the procurement team align the drawing review with fabrication requirements.
Use the purchase order or drawing notes to define who verifies the incoming profile, cut lengths, orientation, fit-up, weld appearance, and final panel alignment. Where project documentation is required, include the profile detail in the Lista de verificação para envio de chapas de PP para projetos EPC rather than treating it as an unrecorded accessory.
A short factory video provides general context for finished PP components before they are supplied for fabrication.
Referência em vídeo: PP Sheet finished Products: Finished Products | QEEHUA. It gives general context for completed PP components; it does not demonstrate U-shaped channel installation or replace the project drawing, welding plan, or structural review.
What should a buyer include in the RFQ?
Specify the detail in a way that lets the supplier identify missing information before production. The following checklist is more useful than a request for a “PP U-channel” without an assembly context.
- Approved panel drawing, material callout, thickness, and revision number.
- Profile orientation, required channel length, corner treatment, cut quantity, and permitted trimming locations.
- Clear internal fit requirement and whether the channel is an edge receiver, a frame element, or a local stiffener.
- Medium, concentration, operating temperature, outdoor or indoor exposure, and relevant cleaning chemicals.
- Required fabrication method, weld access, inspection scope, packing, labeling, and documentation.
- Any sample, first-article, or drawing-approval step required before the production lot.
Know when a U-shaped profile is not enough
Escalate the detail for engineering review when the channel is being asked to carry a significant load, bridge a long unsupported span, replace a designed support frame, control a pressure-containing wall, or resolve a chemical-compatibility uncertainty. A change in one of those conditions can change the appropriate panel, support, and joint solution.
For a quotation or drawing review, entre em contato com QEEHUA with the panel drawing, service conditions, required PP profile function, and documentation needs. This allows the discussion to focus on the fabrication detail rather than an unverified generic channel size.
Perguntas frequentes
Can a PP U-shaped channel replace the structural design of a tank wall?
No. A PP U-shaped channel can be part of an approved reinforcement or edge-detail arrangement, but it does not establish tank-wall thickness, supports, allowable load, or deflection limits. Those decisions require project-specific design review.
What information should be sent with a PP U-shaped channel RFQ?
Send the approved panel drawing, sheet thickness, channel position and length, edge condition, service medium, operating temperature, fabrication method, inspection scope, and any required sample or documentation step.
Should the PP sheet and U-shaped channel be specified together?
Yes. Specify the PP sheet and U-shaped channel together with the planned joint and service conditions so that fit, fabrication, and material suitability can be reviewed as one equipment detail.
How should a fabricated PP channel detail be checked before shipment?
Check the approved drawing revision, profile orientation, cut length, fit-up, joint access, visible fabrication quality, required records, packing, and labels against the agreed inspection plan before shipment.

