
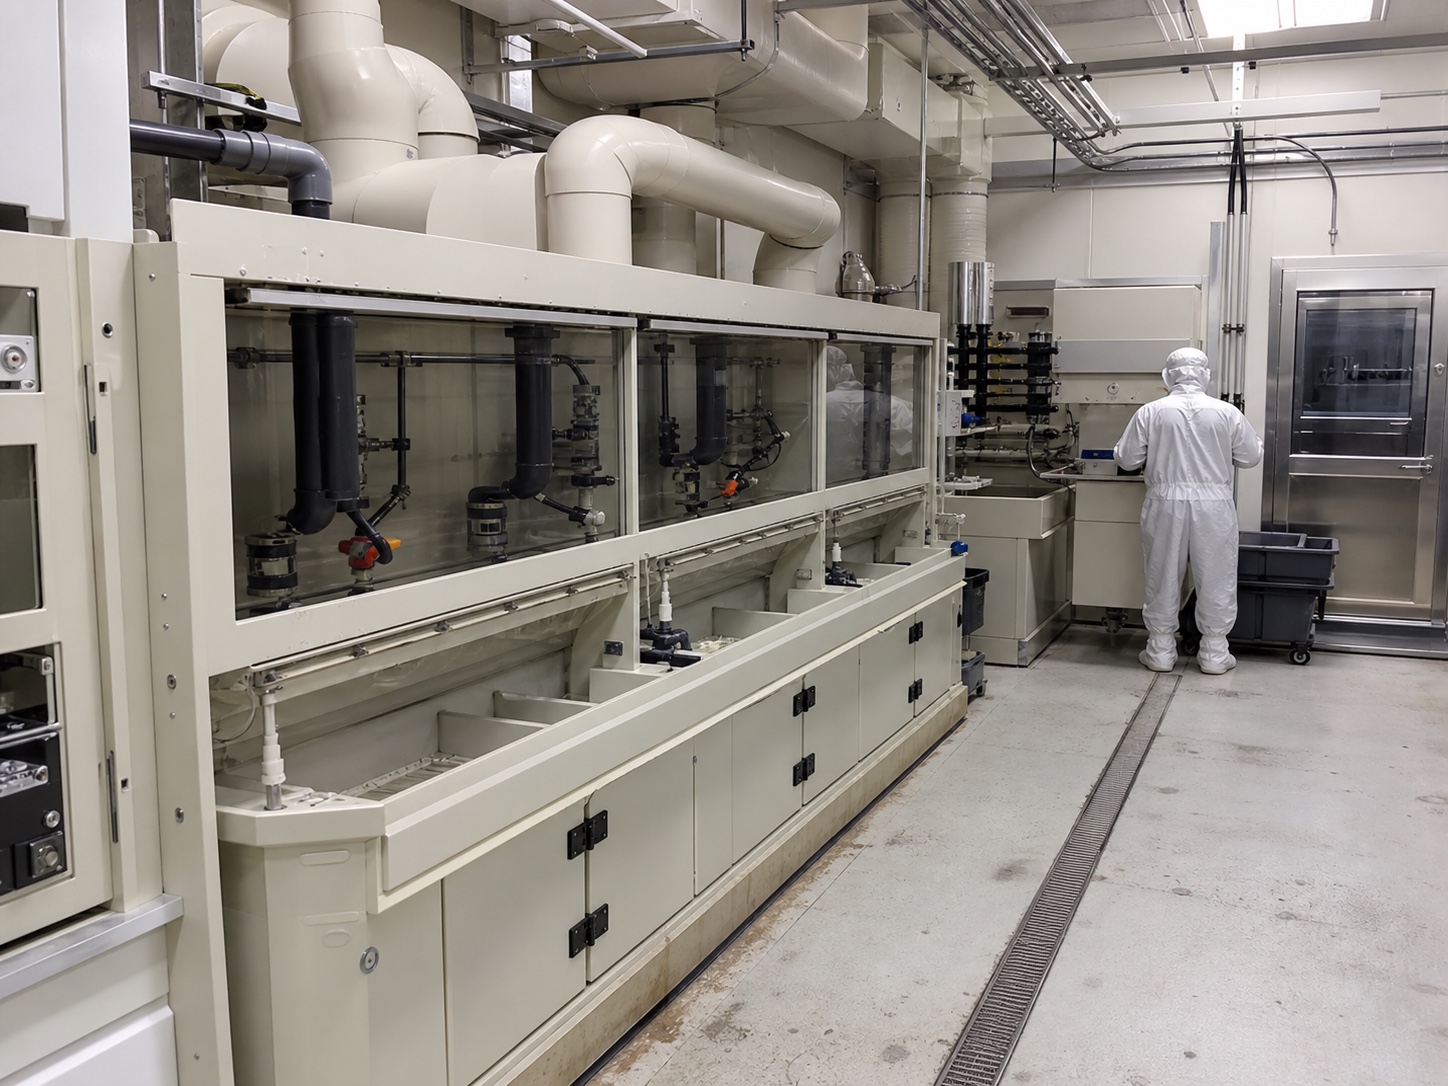
Before a fabricated PP component enters a cleanroom wet bench, the supplier should provide more than a packing slip. The PP sheet cleaning and packaging records should show what was cleaned, how the exposed surfaces were inspected, which packaging layer protects them, and how the receiving team can verify that the delivered part matches the released drawing and cleanliness requirement.
What PP sheet cleaning and packaging records must prove before wet-bench delivery
The delivery package has two jobs. First, it must show that the PP sheet or fabricated panel was identified, inspected and cleaned according to an agreed process. Second, it must protect that condition until the part reaches the receiving area. A cleaning certificate without part identity is not traceability; packaging photos without a cleaning record do not prove surface condition.
ISO 14644-5:2025 places material entry and exit, cleaning, maintenance and monitoring inside the cleanroom operations control programme. ISO 14644-13:2026 addresses cleaning surfaces to defined particle and chemical cleanliness levels. These references provide a framework; they do not assign a universal PP-sheet cleanliness level or replace the customer’s wet-bench specification.
| Record area | Minimum information to connect | Release question |
|---|---|---|
| Component identity | Part number, equipment tag, drawing revision, PP grade, thickness, lot or batch and quantity | Can the receiving team match the package to the released wet-bench drawing? |
| Cleaning activity | Approved method, cleaning agent or medium, rinse/dry step if specified, date, operator and equipment or area | Is the method known and compatible with the PP grade and the required surface condition? |
| تقتيش | Surface, edges, welds, openings, protective film, foreign matter and damage disposition | Was the component inspected after fabrication and again before packaging? |
| التغليف | Inner-contact material, protective layers, seal or closure status, package ID and photographs where required | Will the package prevent recontamination and mechanical damage during the agreed route? |
| Handover | Certificate or checklist, deviations, open items, handling instructions and receiving acceptance field | Can the site close the delivery without guessing what “clean”means? |
Define the cleanliness requirement before recording a cleaning result
Write the requirement in terms the supplier and receiving site can both check. Identify the room or transfer zone, the surface that will contact process chemicals or wafers, the allowable particle or chemical contamination concern, the required inspection method and the point at which outer packaging must be removed. If the customer has a site SOP, URS or contamination-control plan, cite its revision in the purchase or fabrication package. QEEHUA’s PP sheet semiconductor wet-process guide provides the broader material-and-equipment context before the delivery record is finalized.
ISO 14644-18:2023 describes assessing cleanroom consumables by product and process requirements, cleanliness attributes, special properties and documentation. It also makes clear that suitability is use-specific. A PP panel intended for a wet-bench enclosure, tank, splash guard or chemical-transfer interface should therefore be reviewed against its actual location and cleaning route rather than assigned a blanket “semiconductor grade”label.
- Record the required cleanroom or controlled-area destination and the transfer boundary.
- Separate particle cleanliness, chemical residue, ionic or metallic concerns and biocontamination requirements when they apply; do not collapse them into one unqualified score.
- State whether the requirement applies to the PP surface, welds, holes, fittings, protective film, package interior or all of them.
- Define who approves the cleaning method and who accepts the final package at the wet-bench site.
Record the cleaning method and its compatibility with PP
A useful cleaning record names the method instead of saying “cleaned.”It should identify the approved agent or medium, contact or wipe sequence where the project specifies one, rinse and drying controls, the work area, operator, date and result. If a customer requires particle counts, extractables, ionic analysis or another test, record the method, sample location, instrument or laboratory reference and acceptance basis rather than inventing a limit.
Cleaning agents and wipes can affect a polymer surface, printed marking, protective film or welded detail. Review chemical compatibility and drying behaviour with the PP grade and the wet-bench owner before production. Do not use a generic solvent list as evidence that every cleaning chemistry is suitable. If the part is rinsed, prevent trapped liquid in blind holes, channels or low points from becoming a later contamination source. Confirm the proposed material family against the QEEHUA PP sheet product range before recording a grade or lot that the quotation does not identify.
QEEHUA’s internal PP sheet use standard adds a practical control: inspect first, process second. Keep the protective film when the surface requirement calls for it, prevent metal edges or hard debris from rubbing the sheet, and record the point at which film was removed or retained. For fabricated panels, the cleaning record should reference the weld and machining inspection so a clean surface is not used to hide a burr, crack, heat mark or unreviewed repair.
Inspect the PP surface and fabricated details after cleaning
Final cleaning cannot replace a post-fabrication inspection. Check the sheet face, edges, holes, corners, welded seams, nozzles, supports and any area that will be hidden by packaging. Look for chips, deep scratches, burrs, embedded debris, discoloration, weld spatter, lack of fusion, cracks or water marks. Record “accepted,””reworked and re-inspected,”or “held for engineering review”against the part number and drawing revision.
ال PP sheet incoming-inspection checklist can be used as the receiving-side companion: grade, thickness, dimensions, edges, surface and protective-film condition must still match the purchase requirement. For a larger wet bench, link the panel or tank inspection to the equipment tag and weld map so a replacement part is not confused with a different cleanroom package.
If a crack, broken edge, severe scratch or obvious deformation is found, hold the part before packaging. The QEEHUA working manual treats these conditions as stop-and-review points for critical forming, welding and load-bearing work. A polished package is not a disposition for a defective sheet.
Build packaging records that protect the cleaned condition
Packaging should be specified as a contamination-control step, not only as transport protection. State which material contacts the cleaned PP surface, whether an inner bag or cover is required, how sharp corners and welded projections are protected, and where the package may be opened. The receiving site should know whether outer packaging must be removed in a dock, gowning area, airlock or pass-through. Keep the PP sheet cleaning and packaging records tied to this package boundary.
Record the package identifier, layer description, closure or seal status, date and operator. Add photographs when they help show the final condition, but do not treat a photograph as a cleanliness test. If double-bagging, vacuum packing, desiccant, cleanroom wipes or a special container are required, list them as approved project requirements and record their lot or status only when the project actually controls them.
ISO cleanroom operations guidance commonly separates dirty outer packaging from the controlled transfer boundary. Do not place cardboard, dusty pallets or unverified protective materials inside the clean transfer route unless the receiving procedure specifically approves them. The packaging record should state the removal sequence and the clean inner package that remains.
Label every package and preserve chain of custody
Use a package label that remains legible after handling and does not shed onto the clean surface. At minimum, identify the project, equipment tag, part or assembly number, drawing revision, package number, quantity, material or grade reference, cleaning-record number, inspection status and destination. Add orientation or lifting warnings where a large PP panel could be bent, dropped or dragged.
Do not add an expiry date or cleanliness shelf life unless the customer or validated procedure defines one. Instead, record the cleaning and packaging date, the storage conditions, the maximum hold period if specified, and the event that requires re-inspection or re-cleaning. Any opened, damaged, wet or unsealed package should move to a controlled hold status until the receiving team decides what evidence is needed.
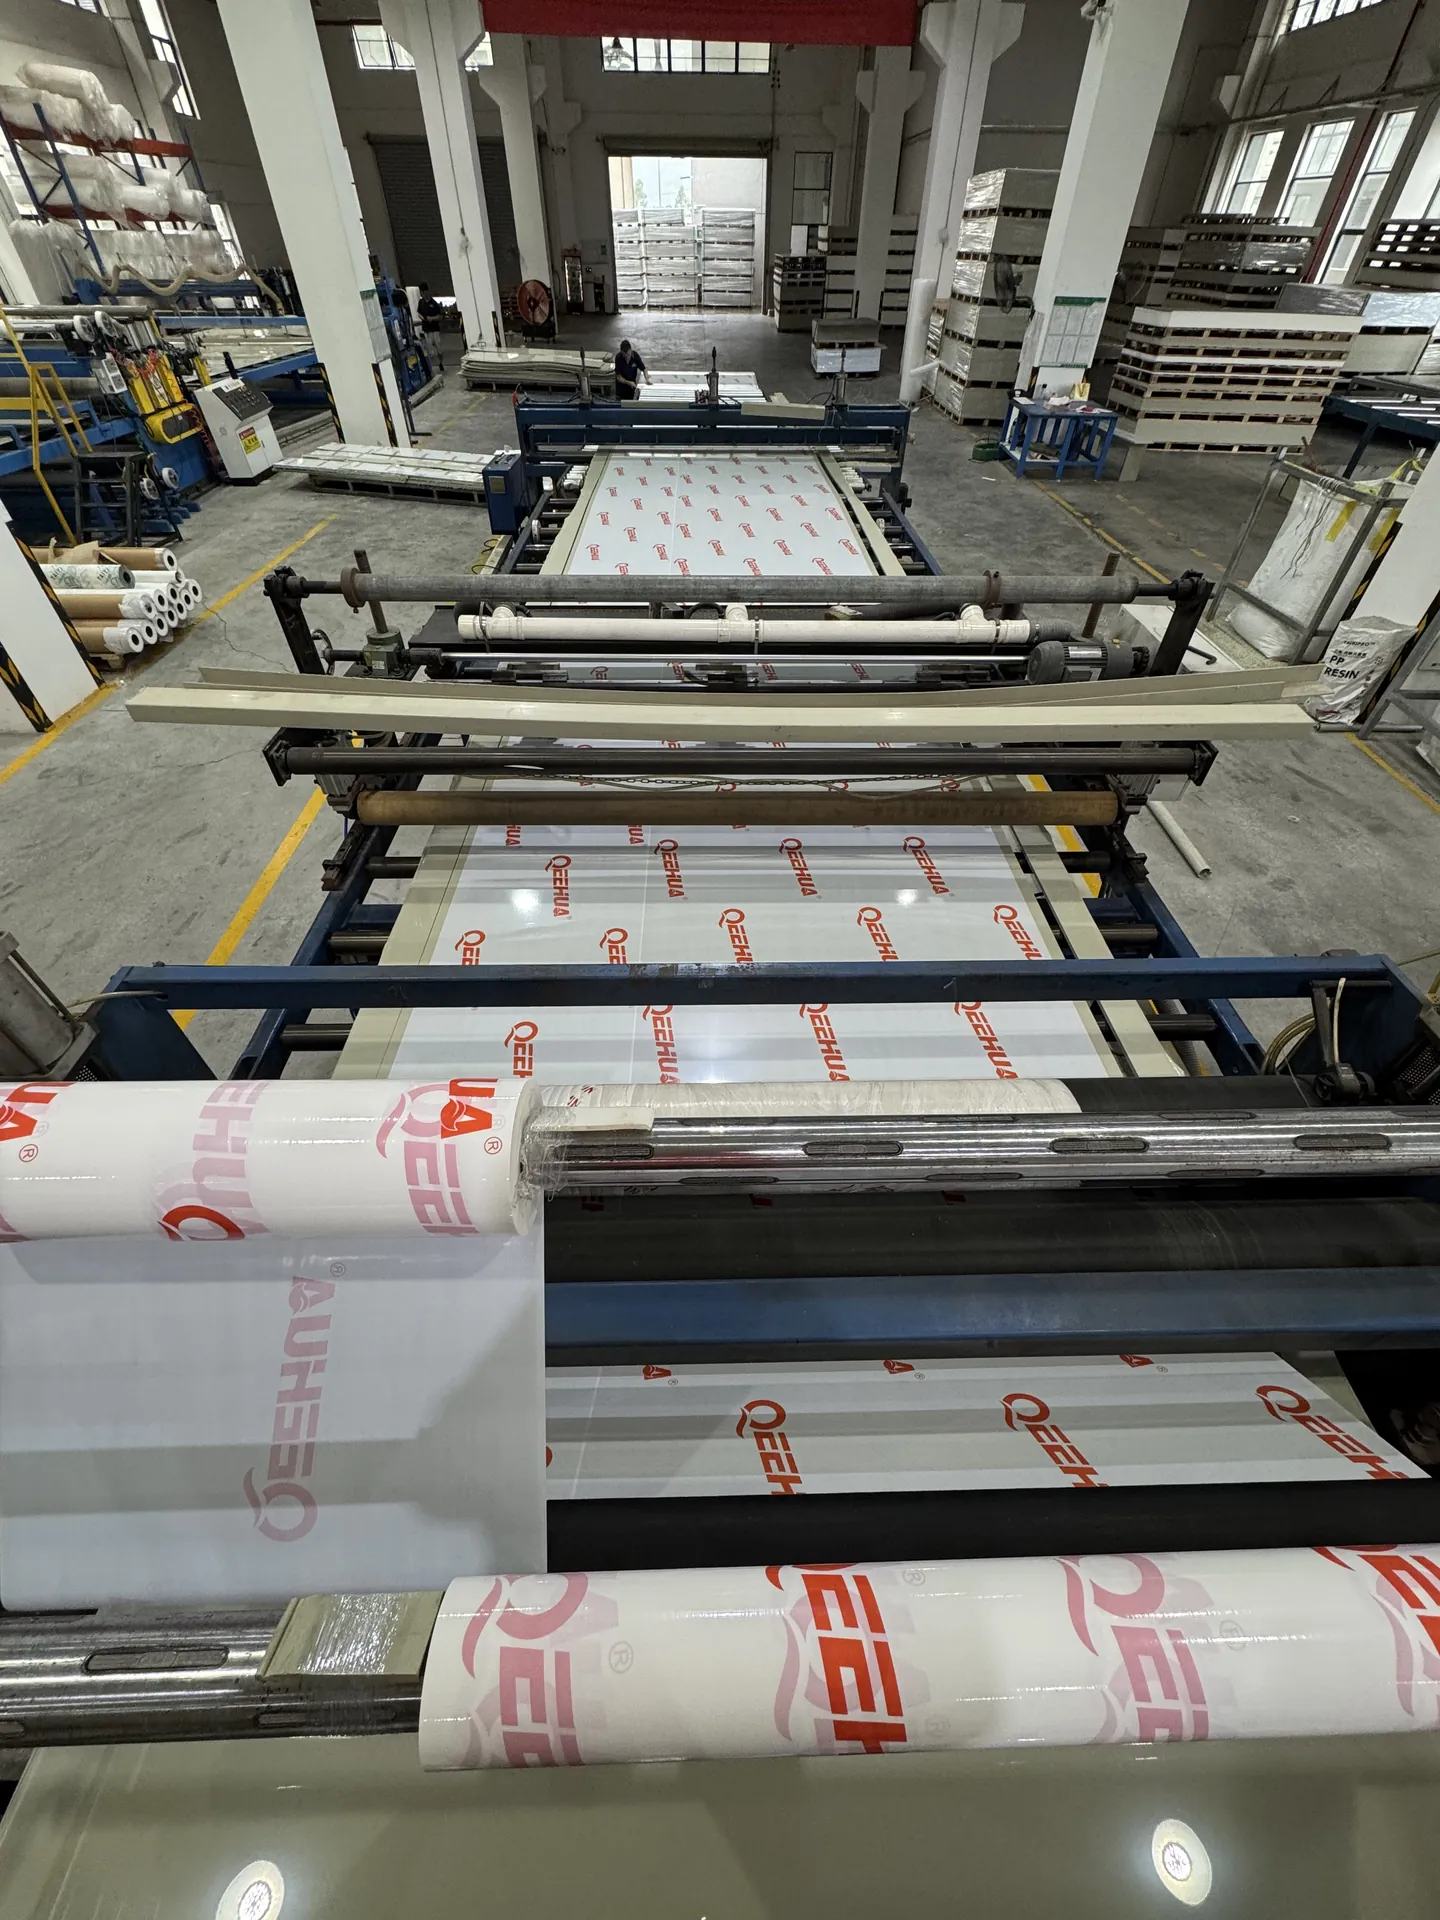
QEEHUA’s finished-product video can illustrate the transition from manufactured PP sheet to a released product, but it does not prove a cleanroom cleaning result or packaging qualification.
مرجع الفيديو: PP Sheet finished Products: Finished Products | QEEHUA shows general finished-product context only; it does not establish cleanroom class, cleaning validation, packaging qualification or wet-bench acceptance.
Keep PP sheet cleaning and packaging records together
The final dossier should let the wet-bench owner decide whether to accept, conditionally accept or hold the package. Keep the evidence in a controlled folder or transmittal rather than sending disconnected photos and certificates.
- Released drawing, bill of materials or part list, equipment tag and revision.
- PP grade, thickness, lot or batch and any material or product statement required by the project.
- Cleaning record with method, approved chemistry, date, operator, area and result.
- Post-fabrication inspection, weld or repair disposition and re-inspection evidence.
- Package record with inner-contact material, closure status, label number and photographs if required.
- Deviation, concession, open-item list and receiving instructions, including the location where outer packaging is removed.
QEEHUA’s قائمة التحقق من تقديم مواد ألواح البولي بروبيلين helps organize the engineering file. For the broader material and fabrication path, see the دليل ألواح البولي بروبيلين: الاختيار والتصنيع والتطبيقات. ال PP semicon screen RFQ guide is a useful sibling reference for cleanroom equipment interfaces. The existing PP sheet project-shipping packaging guide covers general transport questions; this article adds the cleanroom-specific cleaning, transfer and acceptance records.
Hold release when cleaning or packaging records conflict
Stop the delivery review when the package label does not match the drawing, the cleaning record names a different grade or part, a weld repair has no disposition, the inner packaging material is unapproved, the seal is broken, or the receiving procedure cannot determine where outer packaging is removed. Also hold a package when the supplier uses “cleanroom ready”without stating the controlled attributes or evidence behind that phrase.
Send the open item with the drawing, chemical duty, wet-bench location and receiving procedure. QEEHUA can review the proposed PP sheet or fabricated detail against the documented requirement, but the cleanroom owner remains responsible for the final cleanliness level, transfer boundary and site acceptance decision.
الأسئلة الشائعة
Does a cleanroom label prove that a PP sheet is ready for wet-bench delivery?
No. The supplier should identify the component, cleaning method, inspection result, packaging status and receiving boundary. A generic cleanroom label does not define particle, chemical or biocontamination controls.
Should the cleaning record include the chemical or wipe used?
Yes, when the project controls the cleaning method. Record the approved agent or medium, relevant rinse or drying step, date, operator, area and result, and confirm compatibility with the PP grade and any protective film or marking.
Can the package be opened inside the cleanroom?
Only when the receiving procedure allows it. The delivery record should state where outer packaging is removed and which inner package is approved to cross the controlled boundary.
What should happen if a sealed package is damaged in transit?
Place it on hold, photograph the condition, preserve the package label and notify the responsible quality or cleanroom team. Re-inspection or re-cleaning should follow the project procedure before the part enters the wet bench.
For a project review, send the released drawing, PP grade and thickness, cleaning requirement, packaging specification, wet-bench location and acceptance form through the QEEHUA technical inquiry form.
Send the cleaning requirement, drawing revision, package boundary and receiving checklist. QEEHUA can help identify missing traceability, inspection and packaging evidence before the PP component reaches the wet bench.

