A PP sheet fire-performance submittal should prove that the proposed grade, thickness, surface, additives, fabrication method, and finished assembly match the equipment approval requirement. A single “flame-retardant” statement is not enough. The reviewer needs the required test method, specimen basis, result, limitations, traceability, and a clear statement of what the evidence does—and does not—approve.
Start with the approval question, not the rating name
“Fire performance” can mean different things in different approvals. A chemical exhaust duct may be reviewed for flame spread and smoke in a building or air-handling space. A process tank may need a client material declaration and an ignition-risk assessment, while a laboratory enclosure may need an interior-finish or equipment-submittal response. The first page of the PP sheet fire-performance submittal should state the installation location, exposure, mounting orientation, maximum thickness, adjacent materials, ventilation condition, and the authority or specification that defines acceptance.
Ask the reviewer to identify the required method before requesting a certificate. ASTM E84, for example, reports flame-spread and smoke-developed indices under a defined surface-burning test. ASTM also explains that the method is comparative, does not by itself define a material as noncombustible, and can be affected when a material melts, drips, delaminates, or requires support. Those limitations belong in the submittal instead of being hidden behind a pass/fail label.
Separate material-scale evidence from assembly approval
| Evidence type | What it can show | What the reviewer must still confirm |
|---|---|---|
| UL 94 material classification | Small-scale burning behavior for a specified plastic formulation and specimen condition | Whether the thickness, color, formulation, orientation, and end use are covered; UL 94 is not automatically an assembly or building-finish approval. |
| ASTM E84 or UL 723 report | Comparative surface flame-spread and smoke-developed results for the tested specimen | Test mounting, support, thickness, surface, melt/drip behavior, and whether the installed product matches the specimen. |
| Finished-assembly test or listing | Evidence for a defined panel, liner, duct, support, joint, or multi-layer construction | Exact construction, joint details, penetrations, fasteners, coatings, repairs, and allowable field changes. |
| Supplier declaration or SDS | Material identity, hazards, composition boundaries, and handling information | It does not replace a fire-test report, code evaluation, or project-specific approval decision. |
UL Solutions lists UL 94 as a standard for flammability of plastic materials for parts in devices and appliances. Its combustion and fire-testing overview also distinguishes the small-scale UL 94 methods and their specimen conditions. A submittal should therefore name the exact evidence being used instead of treating every fire test as interchangeable.
Build the PP sheet fire-performance submittal around traceability
For a PP sheet fire-performance submittal, the material record is as important as the rating. Include the manufacturer, product family, grade designation, color, nominal thickness and tolerance, surface texture, reinforcement or backing if any, additive or flame-retardant designation, production lot, manufacturing date, and the document revision. If the report uses a different thickness or color, explain the applicability rather than implying that all PP sheet variants share the same result.
QEEHUA’s internal PP-use guidance follows an inspect-first/process-second approach. Before fabrication, verify sheet identification, thickness, surface condition, edge integrity, protective-film status, and storage history. A fire document should be linked to that receiving inspection and to the lot used for the equipment. If the sheet is cut, hot-bent, welded, coated, laminated, or combined with a backing, record the process because the finished configuration may not behave like an untouched laboratory coupon.
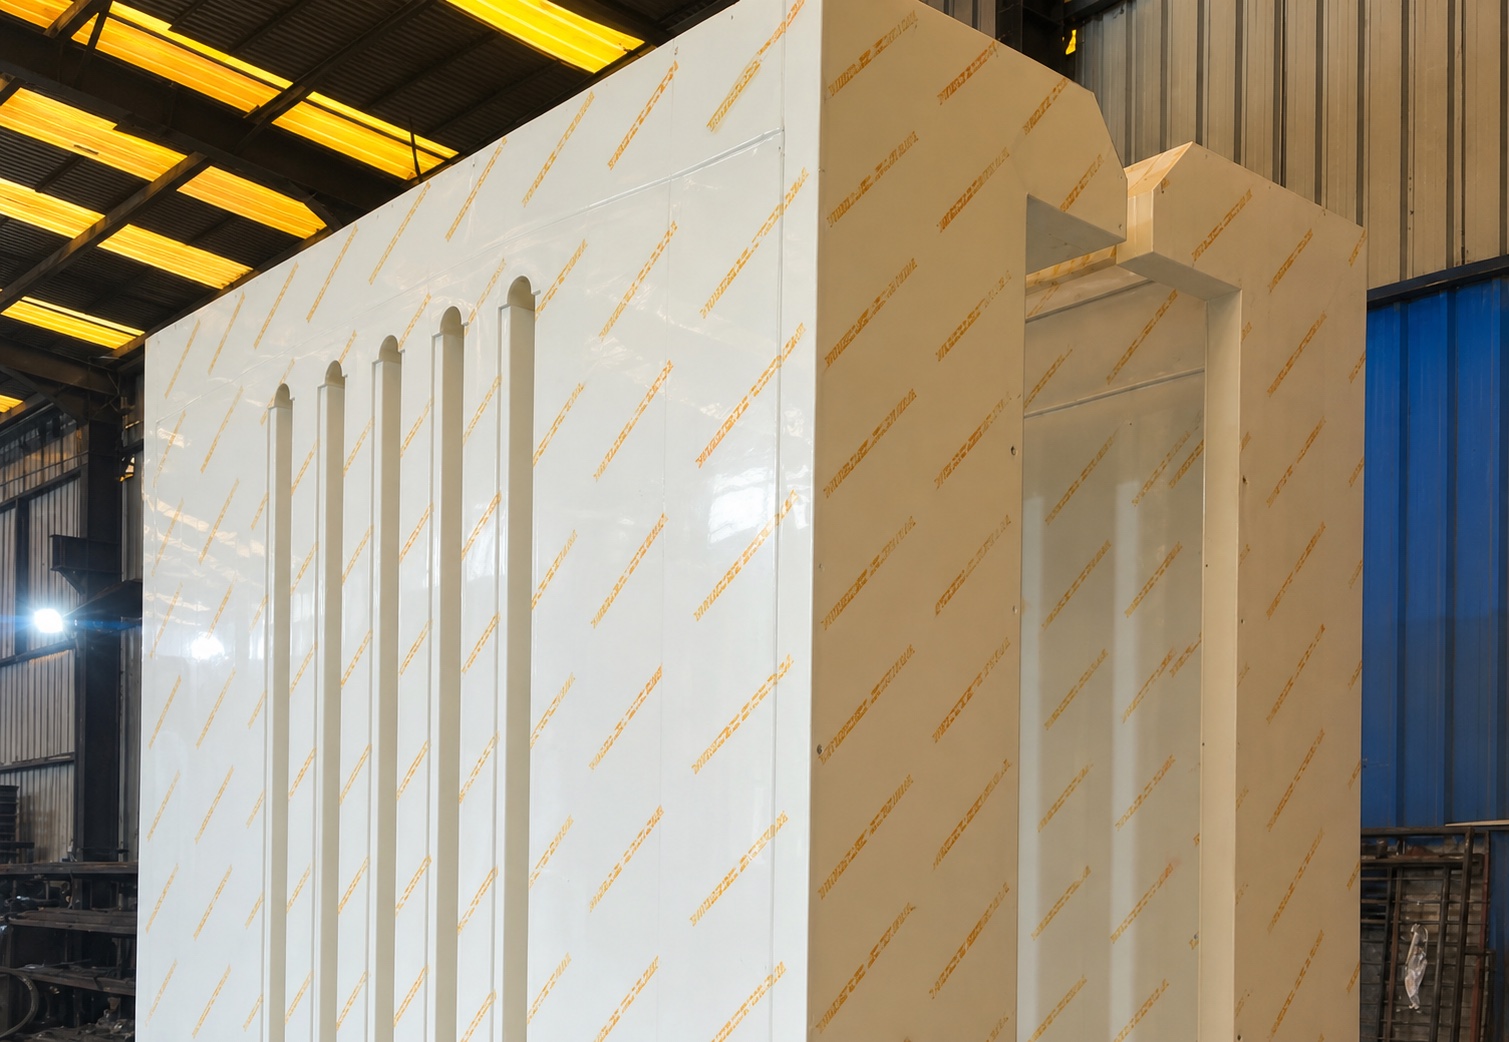
Show the tested specimen and the proposed equipment side by side
The most useful submittals include a one-page applicability matrix. Put the tested specimen on the left and the proposed equipment on the right:
- Material: grade, formulation, color, surface and supplier match.
- Grubość: tested value versus proposed nominal and minimum thickness.
- Geometry: flat sheet, formed panel, liner, duct section, tank wall, or assembly.
- Orientation: exposed face, underside, vertical wall, ceiling position, or enclosed cavity.
- Construction: backing, stiffeners, insulation, fasteners, weld beads, sealants, coatings, and penetrations.
- Exposure: internal process area, room side, plenum, exhaust path, outdoor location, or transport/storage condition.
- Result: report number, test date, laboratory, method edition, result units, classification, and limitations.
Do not hide a mismatch in a footnote. If the report is only a material-scale result, label it as material-scale evidence in the PP sheet fire-performance submittal. If approval depends on the assembled duct, enclosure, or panel system, identify the additional assembly test, engineering judgment, code path, or authority review that remains open.
Include fabrication controls that protect the fire evidence
Approval reviewers often focus on the certificate and overlook the way the equipment will be built. A practical package includes the approved welding method, rod-to-base-material match, joint preparation, weld access, heat-affected areas, repair limits, and a statement about any non-PP components. Keep joints clean and dry, prevent oil or debris from entering the weld, avoid forced bending or impact at a welded area, and allow the assembly to cool naturally unless the project procedure states otherwise.
For a large enclosure or exhaust module, show where the PP sheet meets flanges, supports, duct transitions, dampers, fans, metal frames, insulation, and access doors. The fire-performance evidence should not be presented as approval of a metal support, sealant, electrical item, or ventilation system that was not included in the test. Link the fire package to the drawing revision and to the inspection and handover record.
Use a clear approval checklist before release
Before equipment approval, the package owner should be able to answer every item below without searching through unrelated files:
- What fire requirement or code clause applies to this equipment location?
- Which test method or listing is required, and why is it appropriate for this use?
- What exact PP sheet grade, color, thickness, surface and lot are proposed?
- Does the test specimen match the proposed sheet and finished assembly?
- Are flame-spread, smoke, afterflame, afterglow, dripping, or other requested results shown in the correct units?
- Are welds, backing layers, supports, sealants, penetrations, and field modifications covered?
- Who reviewed the applicability matrix and who has authority to accept deviations?
- What inspection, traceability, repair, and handover records will be delivered?
For related material evidence, use the PP sheet SDS review guide, ten flame-retardant PP sheet selection guide, ten Karta katalogowa i przewodnik po produkcji arkuszy PP, i Strona kontaktowa QEEHUA. These pages support chemistry, application, and fabrication review; they do not replace the authority’s fire-approval decision.
Related QEEHUA process video: this extrusion reference helps explain why lot identity and sheet-process records belong in a technical submittal. It is not a fire test, certification, listing, or code approval.
Video reference: PP Sheet Extrusion: Sheet Formation Process | QEEHUA. It provides general manufacturing context only; fire performance must be demonstrated by the specified test method and matched to the proposed equipment configuration.
Często zadawane pytania
Is a UL 94 rating enough for a PP sheet equipment approval?
Usually not by itself. UL 94 is a defined small-scale plastics flammability test. The approving authority may require ASTM E84, an assembly test, a listing, a code evaluation, smoke data, or another method tied to the installed application.
What thickness should be shown in a PP fire-performance submittal?
Show the tested specimen thickness, proposed nominal thickness, minimum tolerance, and any thickness range explicitly covered by the report. Do not assume that a result at one thickness automatically covers every sheet thickness.
Do PP welds and backing materials belong in the fire package?
Yes. If the finished equipment includes weld beads, backing, stiffeners, insulation, sealants, coatings, penetrations, or metal interfaces, identify them and explain whether the submitted evidence covers the complete configuration or only the PP sheet material.
Who should accept a fire-performance evidence gap?
The project authority, code official, engineer of record, or other named approver should decide. The fabricator can identify the gap and propose additional testing or documentation, but should not convert a material certificate into an unapproved system claim.
Send the project fire requirement, proposed grade and thickness, test reports, assembly drawing, fabrication method, lot information, and acceptance matrix. Contact QEEHUA for a project-specific document review.