A PP sheet extrusion process video can show a buyer how sheet formation appears in a production sequence. It does not answer the project’s material-selection questions by itself. Before ordering, identify the finished component, requested thickness and dimensions, colour or surface needs, chemical exposure, temperature, support arrangement, and fabrication route. The embedded QEEHUA clip is a first-party process reference. It does not state a universal grade, tolerance, output level, or service life. Use it beside a written inquiry and a representative sample plan so the discussion stays connected to the actual equipment requirement.
PP sheet formation during extrusion should be reviewed against the documented project duty, drawings, fabrication scope, material records, and acceptance requirements.
Project context
PP sheet formation during extrusion: project review
Use the documented project requirements to compare the relevant material, fabrication, and quality-control inputs before release.
Sheet formation is only one part of the route from material to a fabricated panel. The buyer’s decision starts with the operating conditions of the final part. A flat enclosure panel, a tank wall, and a machined cover can require different review points even when they use the same nominal PP sheet category.
Write the requirements in the order the project team will use them: part name, drawing revision, dimensions, operating duty, fabrication steps, inspection need, and acceptance question. That record helps a supplier distinguish a request for a standard sample from a request that needs an engineered detail review.
For application context, review QEEHUA’s industry applications and match the inquiry to a named component rather than a broad material label.
Video reference
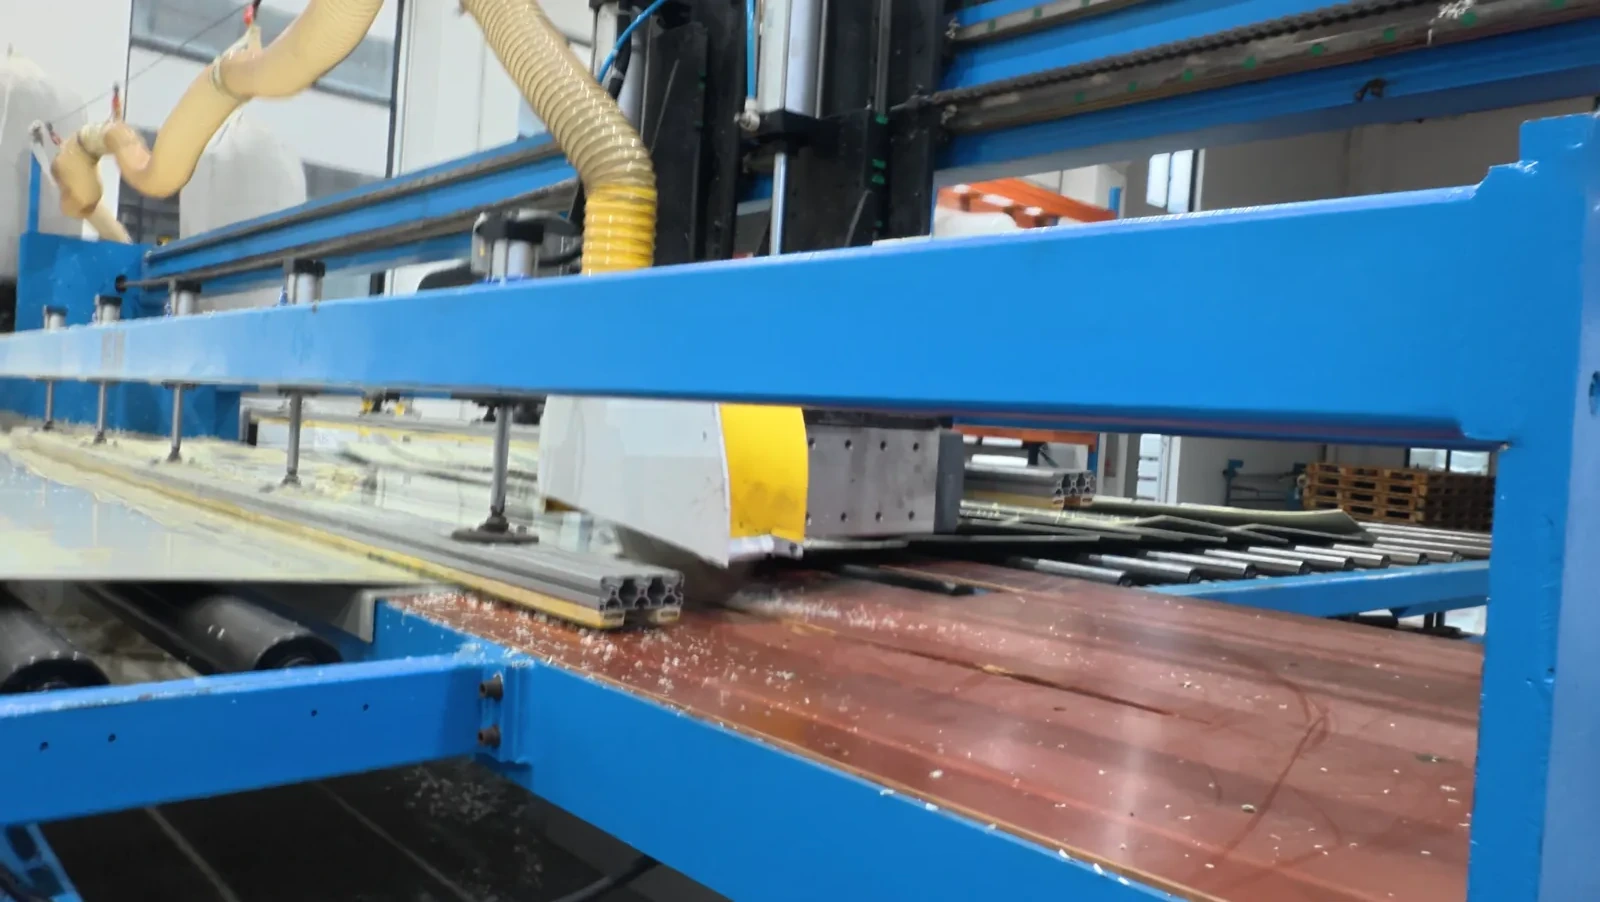
The QEEHUA video shows a sheet-formation stage during PP extrusion. It is embedded close to the discussion so readers can see the subject being described. The video does not replace a product data sheet, an inspection plan, or a confirmed order specification.
When reviewing a sheet-forming reference, keep the question practical. Ask which finished part is being made, which requirement must be maintained after cutting or welding, and what evidence the project will use to accept the sample. Those answers should be recorded before the production release.
Video reference: PP Sheet Extrusion: Sheet Formation Process | QEEHUA. It shows sheet formation during extrusion; it does not replace the project-specific material, fabrication, or inspection review.
Material checks
The data sheet reports density, tensile strength, elongation at break, and a flexural test result for a tested PP sheet sample. These properties are useful when an engineer is comparing a proposed material with a stated project condition. They do not set sheet flatness, cut quality, panel stiffness, or a fabricated-part design without the geometry, loads, supports, and service conditions.
Start with the QEEHUA PP sheet range, then compare the request with the operating conditions and drawing. For chemical-duty equipment, the chemical tank selection guide explains why the medium, concentration, temperature, load, and geometry must remain in the review.
Project data
The following values are presented as a compact reference for the material-review discussion. They remain attached to the tested sample and method. They are not values to copy into a finished-equipment calculation.
| Property | Reported value | Sample and condition | Method |
|---|---|---|---|
| Density | 912 kg/m³ | QEEHUA PP sheet data-sheet sample; conditioning and production grade are not stated | ASTM D792-20 |
| Tensile strength | 30 MPa | QEEHUA PP sheet data-sheet sample; conditioning and production grade are not stated | ASTM D638-22 |
| Elongation at break | 37% | QEEHUA PP sheet data-sheet sample; conditioning and production grade are not stated | ASTM D638-22 |
| Flexural test | 1,870 MPa | QEEHUA PP sheet data-sheet sample; conditioning and production grade are not stated | ASTM D790-25 |
These are reported values for the data-sheet sample. They do not set a saleable-grade specification, a production tolerance, or a finished-equipment design. Confirm the grade, thickness, drawing, process medium, and operating conditions for the project.
Sources and limits: The embedded QEEHUA process video shows the production scene discussed here. ISO 527-1 tensile-testing principles and ISO 178 flexural-properties testing provide published method or measurement context. The table still identifies the ASTM methods used for the reported QEEHUA sample. Neither external source converts a tested-sample value into an order specification; confirm the project requirements before release.
Before a purchase release, compare the data sheet with the actual request line by line. Check the proposed product, grade or required function, thickness, panel dimensions, colour where relevant, process duty, drawing revision, and sample purpose. A number that is not connected to a named component and condition cannot settle the project decision.
If the project asks for a capability outside the approved data record, state the requirement plainly. This can include a functional grade, an application approval, a special resistance target, a tolerance, or a fabrication test. QEEHUA can then confirm what information is available instead of allowing a general video or a tested-sample value to imply more than it proves.
Factory checks
For a panel that will be routed, drilled, cut, bent, or welded, state that operation in the request. The operation can change which edge, surface, or detail needs to be evaluated. A buyer who needs a clean machined face should say so rather than assuming that a general sheet image defines the acceptance condition.
For a chemical or water-contact component, keep the material screen tied to the actual process duty. State concentration, temperature, exposure time, stress, and any cleaning liquid that reaches the part. The internal chemical table is a preliminary screen for listed conditions, not a blanket approval for mixed process media.
Video limits
A production clip can show a process stage, but it does not show every material grade, inspection point, or order requirement. It should never be used to infer fixed lead time, universal tolerance, certification, functional performance, or a finished-equipment design.
Release record
Keep the release record simple and traceable. It should identify the customer component, drawing revision, proposed sheet, dimensions, the condition that controls the review, requested fabrication, sample purpose, and the party who will approve the result. When one of those items changes, the review should be reopened for that changed item.
This record also separates a technical discussion from a commercial assumption. A production image, a process video, a sheet coupon, and a completed equipment drawing have different purposes. Keep each item attached to the question it can answer, then record any requirement that still needs a project-specific confirmation.
Sample request
For a sheet-formation review, send the planned panel size and the intended finishing operation. If the project risk sits at a weld, opening, or support interface, request a detail sample that represents that feature. See the PP sheet sample-request guide for a project checklist, then send the drawing and request a project sample.
Frequently asked questions
What does the PP sheet formation video show?
It shows a QEEHUA production reference for the sheet-formation stage. It does not publish an order-specific specification.
Can a formed sheet video confirm panel flatness for my order?
No. Flatness and any other acceptance requirement need to be confirmed for the requested product and project.
What data should accompany a chemical-duty PP sheet request?
Provide the medium, concentration, temperature, exposure condition, load, drawing, and the component that will contact the medium.
When should I ask for a fabricated sample?
Ask for a fabricated sample when the decision concerns a weld, machined opening, formed feature, or mating interface.
For PP sheet formation during extrusion, record the final project assumptions and acceptance checks before releasing the fabrication or purchase scope.