

How Should Low-Temperature PP Sheet Welding Be Controlled Before Tank Fabrication?
Low-temperature PP sheet welding should be treated as a controlled fabrication condition, not as a reason to simply turn up the hot-air gun. Before a
Low-temperature PP sheet welding should be treated as a controlled fabrication condition, not as a reason to simply turn up the hot-air gun. Before a

PP sheet material traceability should follow the material through the whole job, not stop when the supplier truck is unloaded. A useful package connects the
A PP sheet weld test coupon should prove that the proposed material combination, joint detail, equipment and welding procedure can produce a weld suitable for
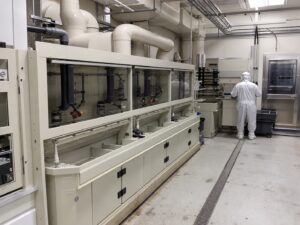
Define the cleaning, inspection, packaging, labeling and handover records a PP wet-bench component should carry before delivery into a controlled cleanroom.
Before chemical-tank fabrication starts, PP welding rods should be stored as controlled welding consumables, not as ordinary plastic stock. The supplier and fabricator should protect
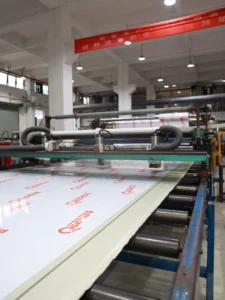
PP sheet surface defects should stop bending, rolling, or welding when they can reduce the remaining section, concentrate stress, or enter a joint or formed
Use a polypropylene sheet SDS review checklist before chemical-equipment approval. Verify identity, revision, hazards, handling, fire, storage and project fit.
Polypropylene sheet machining should be specified as a controlled fabrication process, not only as a list of cut sizes. Before CNC cutting or drilling, the
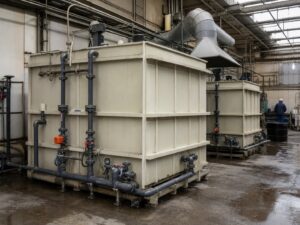
PP sheet chemical compatibility should be reviewed against the real chemical duty, not selected from a chemical name alone. Before choosing a polypropylene tank liner,