
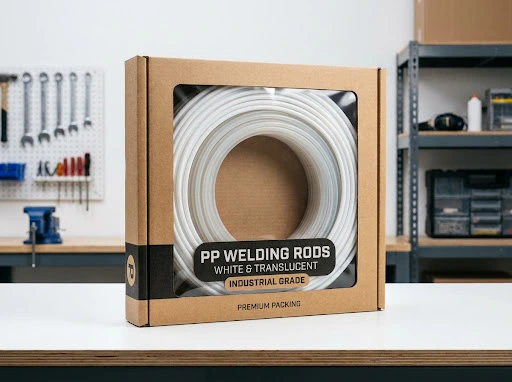
Before chemical-tank fabrication starts, PP welding rods should be stored as controlled welding consumables, not as ordinary plastic stock. The supplier and fabricator should protect material identity, cleanliness, package condition, lot segregation and release records so the rod issued to a weld is compatible with the approved PP sheet and the documented tank duty.
What PP welding rod storage must control before tank fabrication
Storage is the first control point in the weld-quality chain. It cannot correct a wrong polymer, but it can prevent a compatible rod from becoming contaminated, mixed with another grade or disconnected from its records. Treat each pack, spool or bundle as a traceable item that remains linked to the approved tank job until it is issued to the welder.
The storage plan should answer five practical questions:
- Can the team identify the material family, grade, diameter, colour and lot without opening every pack?
- Has the rod been protected from dust, oil, water, direct sunlight, chemicals and mechanical damage?
- Can different PP variants be separated so a similar-looking rod is not issued by mistake?
- Can the fabricator show who received, inspected, released and issued the consumable?
- Is there a clear hold disposition for wet, dirty, damaged, unlabelled or mixed material?
Match the rod to the approved PP sheet and welding process
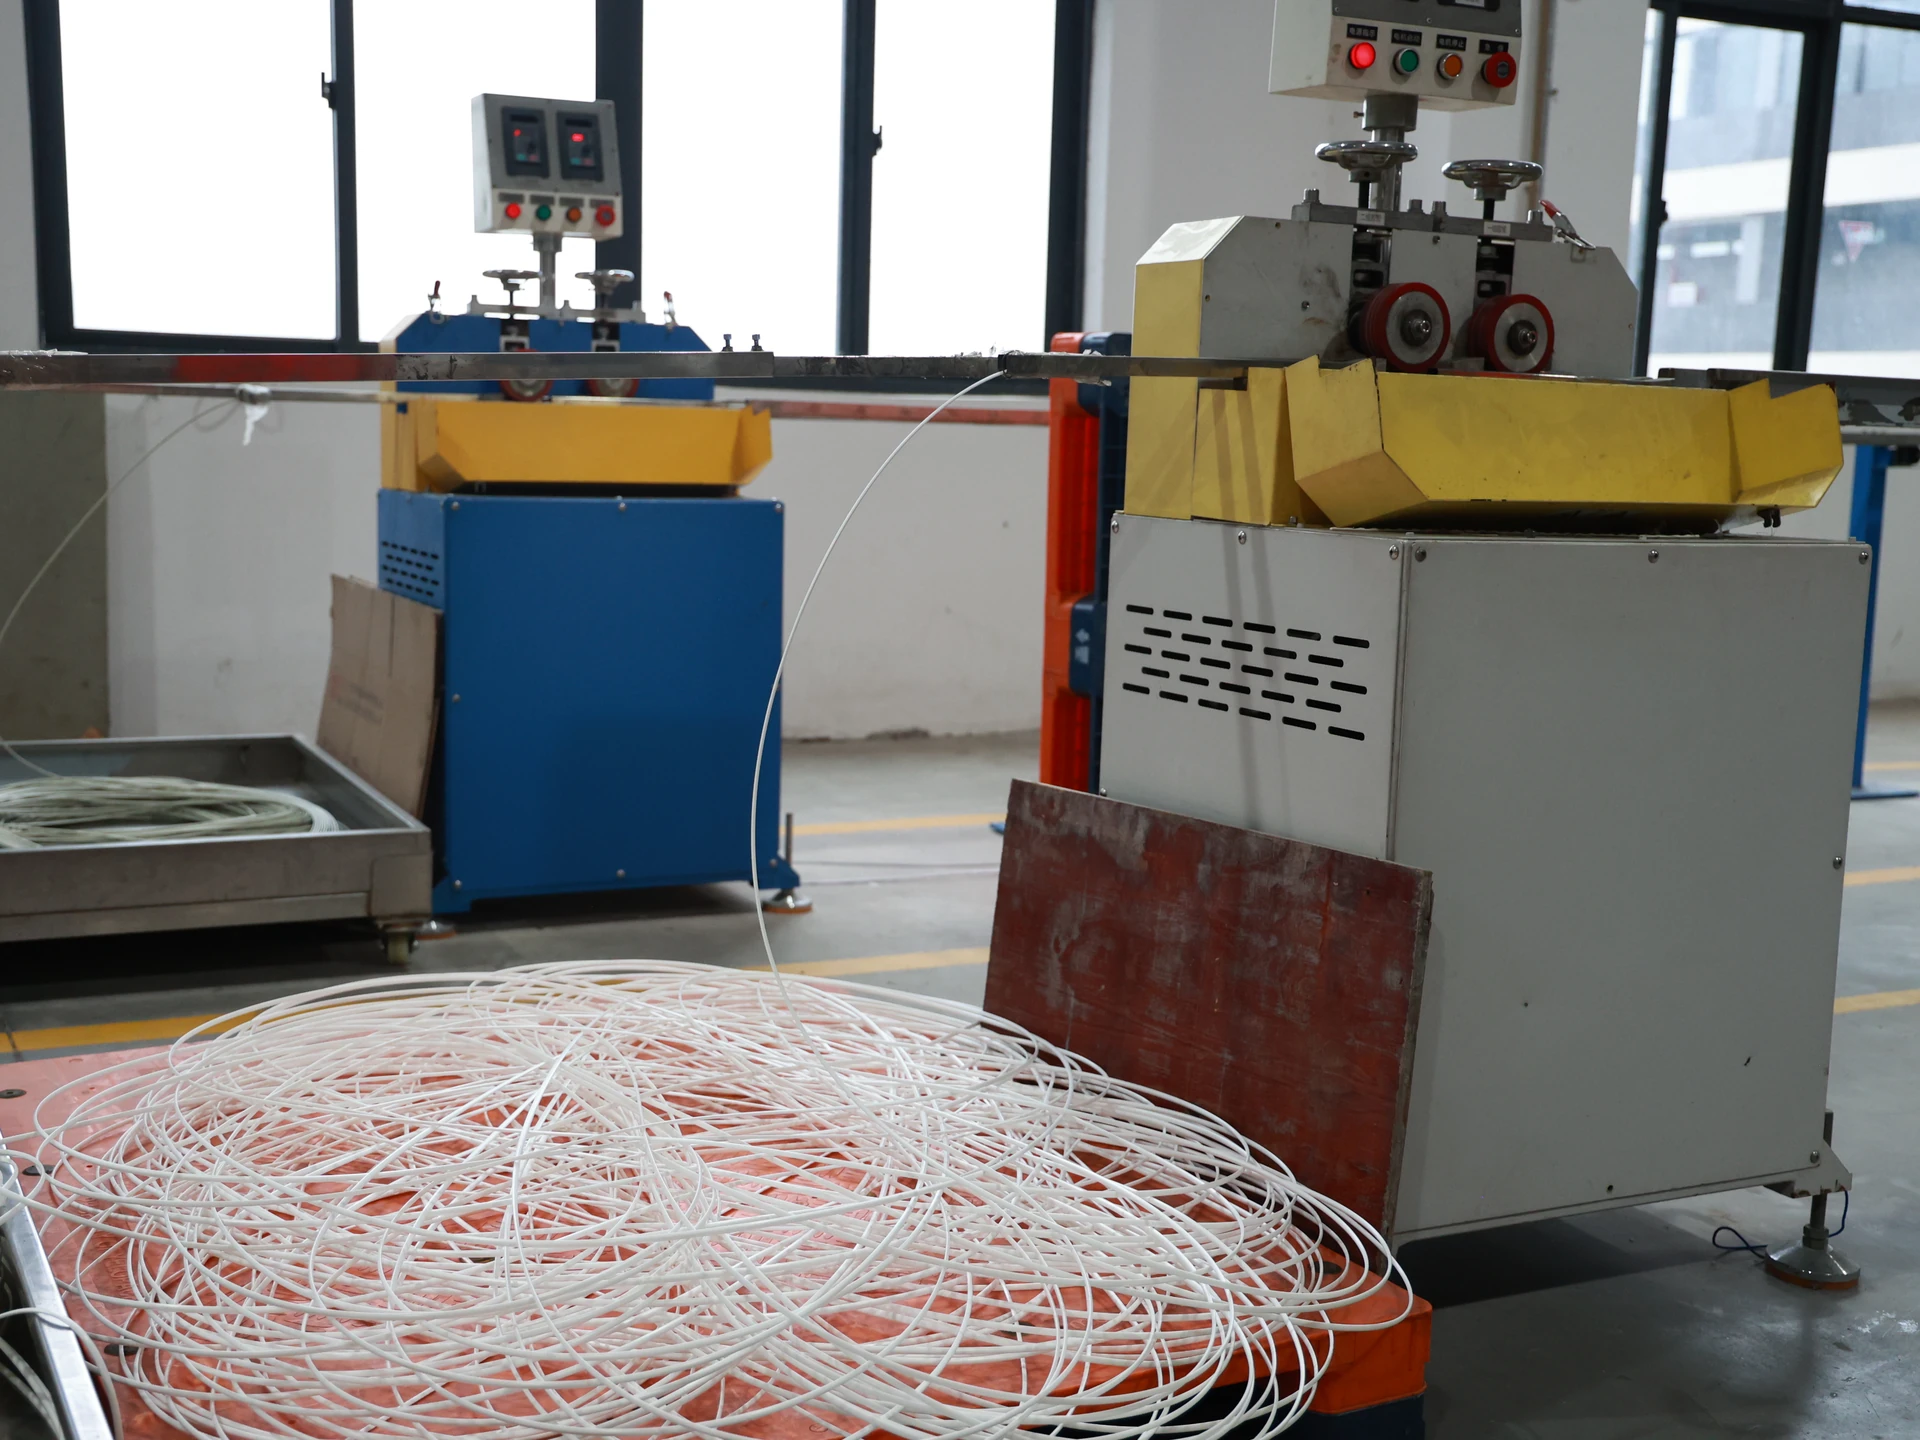
Do not select a rod by the word “PP” or by colour alone. Confirm the base-sheet material family and the filler specification in the drawing, welding procedure, customer requirement or approved technical submittal. PP-H, PP-B, PP-R, flame-retardant, conductive and other modified grades may not be interchangeable simply because their labels look similar.
The Roechling storage and processing guideline states that the base material and filler must be identical in material for the cited thermoplastic welding applications, and that weld surfaces must be clean and free of grease. It also points users to applicable DVS welding guidance for process parameters. Use that as a technical reference, not as a substitute for the grade-specific procedure on the project.
Before storage, record at least the sheet grade or designation, rod designation, diameter or profile, colour where controlled, supplier or manufacturer, lot number, purchase reference and intended tank or equipment tag. If the drawing does not identify the consumable clearly, hold the release and request clarification rather than allowing the welder to choose from a mixed shelf.
QEEHUA’s existing PP welding rod selection guide covers the material-and-application decision. This article adds the storage controls needed after selection and before the rod reaches the weld joint.
Choose a clean, dry and protected storage location
Keep PP welding rods indoors whenever practical, in a clean and dry area away from rain, condensation, process chemicals, oils, grinding dust, welding spatter, direct sunlight and local heat sources. The location should not be used as a general scrap shelf. If the project requires a controlled temperature, humidity or cleanroom boundary, record that requirement in the storage instruction and follow the customer’s validated procedure.
Protect open packs with a clean cover or resealable package that does not shed fibres onto the rod. Keep rods off a wet floor and away from sharp edges that can score or kink them. For spools, use a stable rack or pallet that prevents rolling and crushing. For straight rods, use full-length support so they do not bow under their own weight. Do not place heavy components on top of a consumable carton.
The broader PP sheet storage and handling guide applies the same practical principle to sheet stock: store flat, keep materials supported, avoid weather and one-sided heating, and inspect before processing. Welding rods need the same discipline even when their smaller size makes them easier to overlook.
Separate rods by grade, diameter, lot and fabrication job
Use physical shelf locations, bins or sealed containers with a label that remains legible after handling. Separate at least the variables that can change weld suitability or traceability:
| Control | What to separate | Why it matters before welding |
|---|---|---|
| Material family and grade | PP-H, PP-B, PP-R, flame-retardant, conductive or other approved variants | A similar colour or profile does not prove melt behaviour or compatibility with the sheet. |
| Diameter or profile | Rod diameter, strip or extruder-specific filler format | The welding tool and procedure may be qualified for one feed size only. |
| Lot or batch | Supplier lot, production batch and received quantity | Preserves the lot-to-weld record and supports an investigation if a defect is found. |
| Tank or job allocation | Equipment tag, drawing revision and work order | Prevents a released consumable from being issued to the wrong chemical duty. |
| Status | Pending inspection, released, issued, returned or on hold | Stops unreviewed or returned remnants from entering a critical weld. |
Never pour loose remnants from different lots into one unlabelled box. If a rod is returned from the work area, keep its identity and contamination status visible; otherwise treat it as hold material until the responsible quality person decides whether it can be re-identified and released.
Inspect packaging and rod condition before release
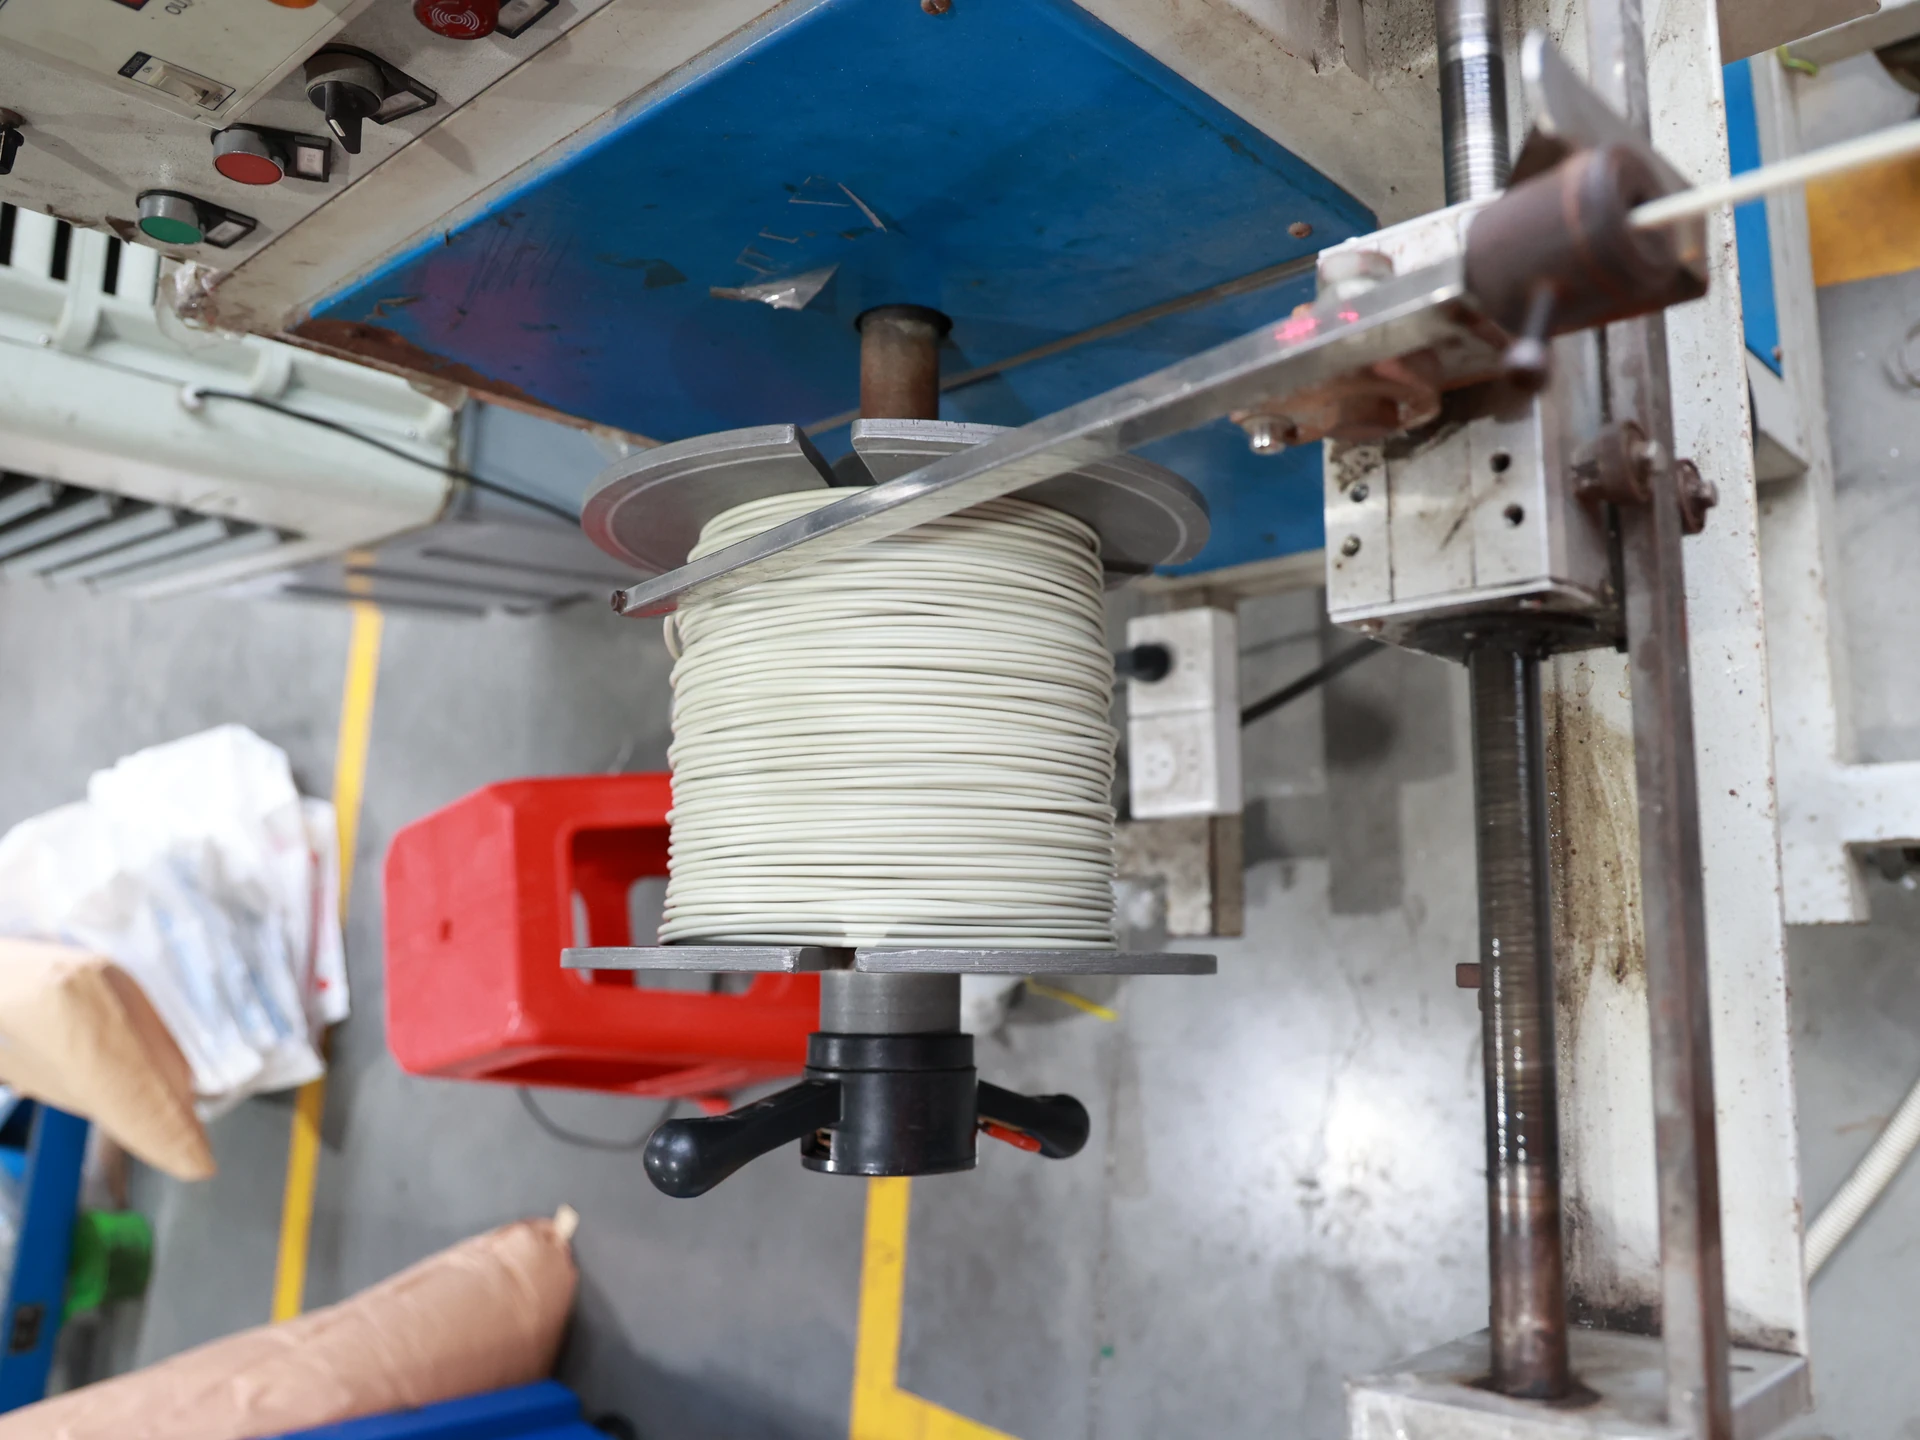
At receipt and again before issue, inspect the pack, label and exposed rod. The package should be closed or protected, with no evidence of water, oil, dust, chemical splash, UV damage, crushing, severe bending, surface scoring or mixed contents. Check that the quantity and lot on the delivery document match the label and purchase requirement.
Pay attention to the rod surface and end. A dirty or damaged end can carry contamination into the weld pool; a kinked or crushed rod can feed inconsistently. Do not “clean up” a serious surface defect and release the rod by judgement alone. Photograph the condition, place the item on hold and document the disposition or replacement decision.
QEEHUA’s internal PP sheet use standard follows an inspect-first, process-second rule. For tank fabrication, extend that rule to the consumable: verify the rod before setting the welding equipment, and verify the base sheet and joint preparation before opening the next pack. The rod cannot compensate for a cracked sheet edge, contaminated joint or unapproved repair.
Control temperature, moisture and acclimatization without inventing limits
Storage guidance must come from the rod supplier, grade data and project procedure. Do not transfer a sheet-storage number to welding rods as if it were a universal limit. If rods or the PP sheet have been kept in a cold, hot or humid area, allow the materials to reach the workshop condition required by the approved welding procedure before welding. Record any required conditioning step and its acceptance check.
The QEEHUA working manual warns that PP impact toughness decreases below 5 degrees C and recommends warming sheet material to at least 5 degrees C before processing. That is internal project guidance for the sheet and should not be rewritten as a universal rod-storage specification. It does, however, support a practical hold point: do not start a tank weld when the base sheet, rod or joint area is visibly wet, cold enough to affect the procedure, or otherwise outside the documented process window.
The DVS technical-code index for joining plastics identifies DVS 2207 procedures for hot-gas and extrusion welding and DVS 2211 requirements for welding fillers, marking and tests. Use the applicable code and the equipment or material supplier’s instructions to set actual parameters; storage records alone do not qualify a weld.
Build a pre-fabrication release record
The release record should be short enough to use at the shop floor and detailed enough to close a quality question later. Link the consumable to the tank rather than keeping a generic warehouse sign-off.
- Tank or equipment tag, drawing revision and welding-procedure reference.
- PP sheet grade and the approved welding-rod designation, diameter or profile.
- Supplier, purchase reference, package ID, lot or batch and received quantity.
- Storage location, package condition, inspection date and inspector.
- Segregation status, issue quantity, returned remnants and any hold or deviation number.
- Confirmation that the joint surface, welding equipment and work area are ready before issue.
For the weld itself, connect the rod issue record to the PP welding-rod traceability guide and the PP tank weld inspection checklist. The PP sheet material-submittal checklist can hold the grade, drawing and project-document references. These links are complementary: storage release, weld traceability and final inspection should not be treated as one interchangeable record.
Place the rod on hold when identity or condition is uncertain
Stop issue when the label is missing, the grade does not match the drawing, the package is wet or open, the rod is dirty or damaged, two lots are mixed, or a returned remnant cannot be tied to a job. Also hold the consumable if the customer changes the tank chemical, temperature, liner, sheet grade or welding process after the rod was released.
Send the discrepancy with the package photographs, delivery record, sheet identification, chemical duty and procedure reference. QEEHUA can review the proposed PP sheet and welding consumable against the documented requirement, but the fabricator’s qualified welding procedure and the project quality authority remain responsible for final release.
QEEHUA’s manufacturing video provides general raw-material feeding context. It can help explain why production and storage identity matter, but it does not qualify a particular welding rod, storage room or chemical-tank weld.
Video reference: PP Sheet Manufacturing: Industrial Hopper Mixer for Material Feeding | QEEHUA shows general material-feeding context only; it does not establish PP welding-rod storage limits, material compatibility or chemical-tank weld acceptance.
Frequently asked questions
Can PP welding rods be stored beside PP sheet?
They can share a clean, dry storage area when each item remains protected, labelled and separated by material, grade, lot and job status. Do not place rods where sheet handling, grinding dust, chemicals or wet floors can contaminate them.
Is rod colour enough to identify the correct welding consumable?
No. Colour is only an identification aid when the project controls it. Confirm the material family, grade, diameter or profile, lot and approved welding procedure before issue.
What should happen to an opened or returned package?
Keep it identified and protected, record the quantity and condition, and return it to the same job-controlled location. If identity or cleanliness is uncertain, place it on hold until the responsible quality person decides its disposition.
Does correct PP welding rod storage prove the tank weld is acceptable?
No. Storage protects the consumable and its identity. The weld still requires compatible base material, qualified process parameters, clean joint preparation, competent fabrication and the project-specified inspection or leak-test evidence.
For a project review, send the PP sheet grade, rod designation and diameter, chemical medium and concentration, operating temperature, tank drawing revision, welding procedure, storage requirement and receiving or inspection form through the QEEHUA technical inquiry form.
Send the approved sheet grade, welding-rod specification, lot records, storage condition and chemical-tank drawing. QEEHUA can help identify missing segregation, cleanliness and release evidence before fabrication begins.

