
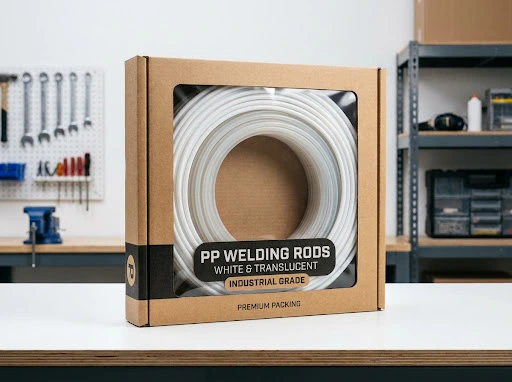
Verify PP welding-rod traceability by matching the delivered rod label to the approved material, component drawing, receiving log, and weld record. Keep that chain with the equipment dossier, then resolve any mismatch before welding. For QEEHUA material, request project-specific confirmation of the available lot and accompanying documentation.
Why PP Welding Rod Traceability Matters for Fabricated Equipment
For fabricated tanks, ducts, wet-process equipment, and other PP assemblies, a shipment label alone is not a complete project record. The practical aim of PP welding rod traceability is to make a later review possible: start with the rod received at the shop, follow it to a defined weld location, and connect that location to the equipment drawing and inspection record.
That record is useful when a purchaser asks which consumable was used on an equipment section, when a shop needs to isolate an uncertain delivery, or when a revision changes the material callout. It is a control method, not proof by itself that a weld is acceptable. Joint preparation, process control, inspection, and the project acceptance plan remain separate checks. See our guidance on PP welding joint preparation for fabricated equipment for the preparation step that should sit beside the record.
As a quality-system principle, records can provide evidence and formalize traceability; ISO also treats documented information as a controlled form of evidence. ISO 9000 terminology is useful background when a project team defines its own document set.
Build the PP Welding Rod Traceability Record Before Fabrication
Create the record before loose coils, offcuts, or substitute materials enter the work area. Give each received lot an internal receiving reference if the supplier label does not already provide one. The reference can be simple, provided it is carried consistently from receipt to the weld log.
Minimum project record
- Purchase order, supplier name, delivery date, and received quantity.
- Supplier label details actually present: product name, rod profile or size, colour, lot or batch identifier, and any stated documentation reference.
- Approved drawing or material schedule identifying the PP component and planned weld area.
- Receiving check result, storage location, and the person who released the material to fabrication.
- Weld log entry tying the rod reference to the assembly, seam number, operator, date, and applicable inspection record.
| Checkpoint | Co porównywać | Evidence to retain |
|---|---|---|
| Receiving | Delivery paperwork against the order and the physical label. | Receiving log, delivery note, label photograph where project rules allow it. |
| Material issue | Rod reference, profile, colour, and intended PP assembly. | Material issue ticket or controlled weld-log field. |
| Fabrication | Issued rod reference against the seam or assembly identifier. | Weld map or traveller signed under the project procedure. |
| Release | Weld record, inspection result, and any unresolved deviation. | Equipment dossier or customer turnover package. |
Match the Rod to the Intended PP Component
Before material issue, compare the approved product description with the physical rod and the component callout. QEEHUA public product information identifies PP welding rods for welding plastic sheets, pipes, and related products. It does not establish which project-specific lot records or certificates accompany a particular order, so the buyer should list those deliverables in the RFQ or purchase order.
Use the same review discipline when selecting the rod in the first place. Our article on choosing PP welding rod for fabricated equipment helps separate product selection from the subsequent traceability task. When the base sheet itself needs review, connect the record to the approved sheet identification and the Lista kontrolna dotycząca składania materiałów arkuszowych PP w projektach EPC.
Record PP Welding Rod Traceability at the Weld
Do not wait until shipment to reconstruct the link. Record the rod reference when the seam is made, while the work order, operator, assembly, and material issue information are available. Where several operators or shifts work on one vessel, the record should identify the relevant seam segment or assembly rather than applying one broad batch statement to the whole project.
This approach supports a focused review if a mismatch later appears. It also prevents a label from being mistaken for a release decision: the completed record should point to the inspection result, not replace it. For a complementary final-stage check, read how to check PP welding joints before a chemical tank ships.
What to Do When the Traceability Chain Breaks
Segregate material with an unreadable, conflicting, or missing identifier until the project authority decides how it will be dispositioned. Do not assume that similar colour, appearance, or storage location establishes identity. Record the deviation, the affected assemblies or seams, the evidence reviewed, and the decision made. If replacement material is issued, start a new controlled reference rather than extending the uncertain record.
Safe welding practice is also a separate obligation. OSHA notes that welding and cutting hazards can include burns, eye damage, shock, cuts, and other risks controlled through work practices and PPE. Follow the site procedure and applicable requirements; OSHA’s welding safety overview is general safety background, not a PP fabrication procedure.
Video: PP Sheet Preparation Context
Odniesienie do filmu: PP Sheet Manufacturing: Industrial Hopper Mixer for Material Feeding | QEEHUA. It shows a material-feeding stage in PP sheet production; it does not verify welding-rod identity, lot traceability, or finished-weld quality.
FAQ
What is PP welding rod traceability?
It is the controlled link between an identified welding-rod lot or receiving reference, the intended PP component, and the weld or assembly record retained for the project.
Is a supplier label enough for traceability?
No. The label is starting evidence. A project record should also link the supplied rod to receiving, material issue, the relevant weld or assembly, and the release or inspection record.
Should a QEEHUA order include a lot certificate?
Request the required lot, batch, certificate, and documentation deliverables in the RFQ or purchase order. Confirm what can be supplied for the specific project before fabrication begins.
Does traceability prove a PP weld is acceptable?
No. Traceability identifies material and records. Weld acceptance still depends on the approved procedure, workmanship, inspection, and the project’s defined acceptance criteria.
Plan the documentation with your PP material order
Send QEEHUA the equipment application, drawings, required rod profile, colour, quantity, and the traceability documents your project needs. We can help you start a clear material discussion before fabrication.

