
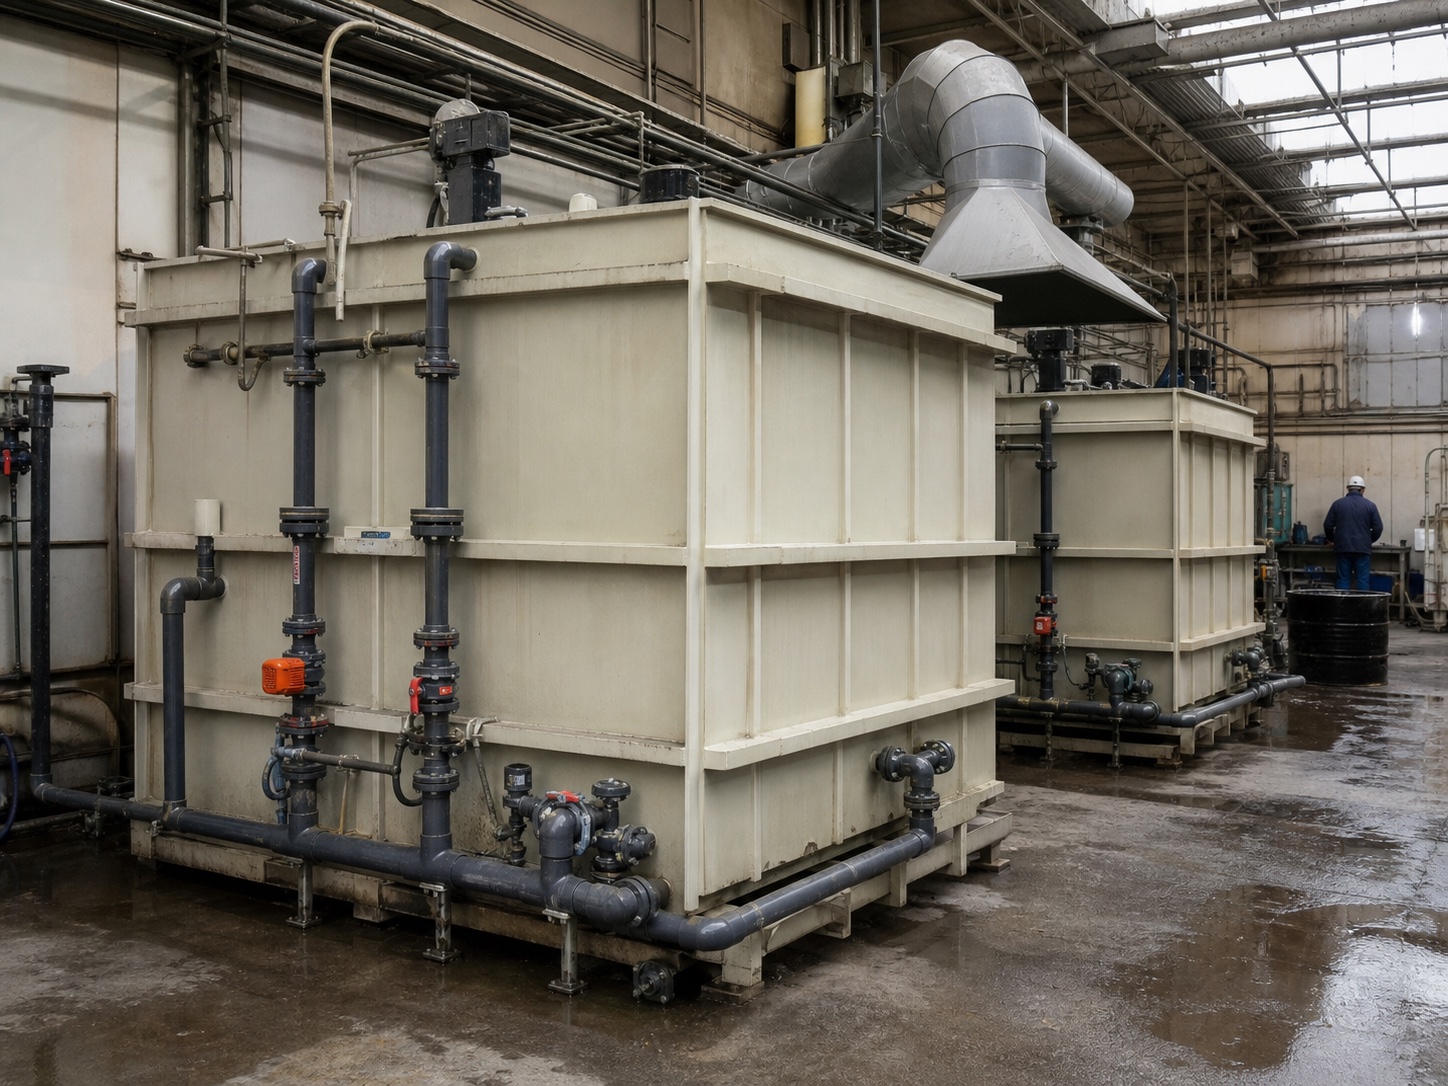
A PP ductwork RFQ for acid fume extraction should define the emission source, chemical and temperature data supplied by the process owner, required airflow or pressure basis, route, interfaces, fabrication scope, inspection records, and commissioning responsibilities. Without those inputs, a supplier cannot responsibly confirm material suitability or a complete duct system.
Start the RFQ with the Acid Fume Capture Problem
Begin with the process, not a generic duct diameter. Identify every tank, hood, enclosure, pickling line, or other emission point; its operating cycle; nearby openings; and where operators work. Local exhaust ventilation is intended to capture contaminants at or near their source before they disperse, so the capture point and operating conditions belong in the request. OSHA’s ventilation primer provides general background on that control principle.
State the exact chemical names, concentrations, temperatures, mist or vapour conditions, and any cleaning or upset conditions that the process owner can provide. These are project inputs, not values to infer from the term “acid fume.” QEEHUA-specific material suitability and fabrication details should be confirmed against the actual service conditions. For the preceding selection question, see PP sheet for chemical exhaust ductwork: selection guide.
Define the System Boundary and Air-Side Data
Make the quotation boundary visible on a layout drawing. Mark where the supply begins and ends, which items are by others, and the intended connection to hoods, fans, scrubbers, stacks, dampers, or existing ducts. Include the design airflow or pressure information supplied by the ventilation designer, or state that it remains to be provided. Do not ask a material supplier to silently assume the ventilation duty.
Process and air-side inputs to request
- Equipment list, capture-point locations, hood or enclosure drawings, and operating modes.
- Known chemical, concentration, temperature, moisture, particulate, mist, and cleaning conditions.
- Airflow, pressure, fan, scrubber, and stack data supplied by the responsible ventilation designer.
- Required capture performance, applicable site standards, and any emission-control acceptance criteria.
- Existing-system survey information where the new ductwork joins installed equipment.
HSE guidance treats a local exhaust system as a connected set of hoods, ducts, air movers, air cleaners, and supporting documentation. Its RFQ guidance is useful for defining design, commissioning, and documentation deliverables without substituting for the project engineer’s calculation. HSE HSG258 is a general reference for those system elements.
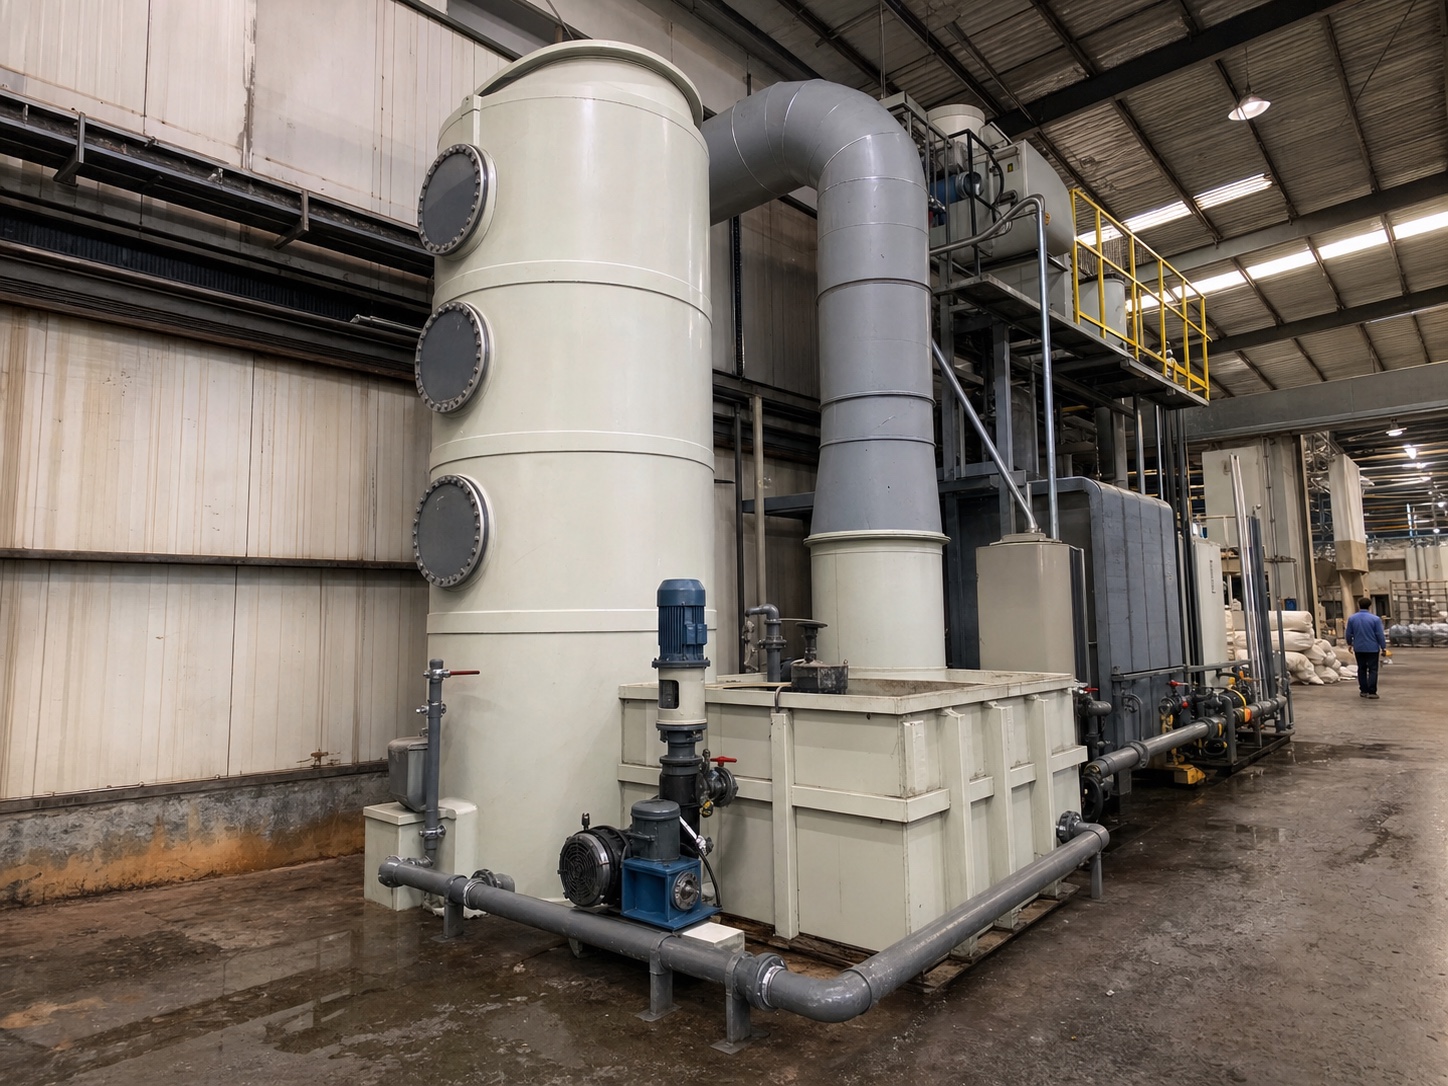
Specify the PP Ductwork Scope by Drawing
Use plans, elevations, sections, and an isometric or spool schedule when available. Identify straight runs, elbows, branches, transitions, inspection openings, drain points, expansion provisions, removable sections, flanges, gaskets, fasteners, supports, and penetration details. If a component is to match existing equipment, provide photographs, dimensions, and the mating-interface information rather than relying on a site name.
| RFQ section | Information to include | Why it changes the quotation |
|---|---|---|
| Route and geometry | Drawings, elevations, clearances, branch locations, bends, and transitions. | Defines fabrication pieces, site fit-up, access, and interfaces. |
| Connections | Mating dimensions, flange standard or project detail, gasket and fastener requirements, and items by others. | Prevents a fabricated duct section from arriving without a defined connection boundary. |
| Support and access | Support responsibility, building attachment limits, access doors, inspection points, and maintenance clearances. | Separates duct fabrication from structural, installation, and service work. |
| Documentation | Submittals, drawings, material identification, inspection records, packing, and handover requirements. | Lets the supplier price the requested evidence and turnover package. |
For the base-material documentation path, link the RFQ to the PP sheet material submittal checklist for EPC projects. A material submittal and a ventilation design are different documents; the RFQ should request both where the project needs them.
Separate Fabrication, Installation, and Commissioning Responsibilities
State whether the quotation is for supplied components only, shop fabrication, site installation, or a defined combination. Name who provides field measurements, lifting, supports, site welding, leak checks, airflow testing, commissioning, and the final system performance decision. A clear split protects both the purchaser and the supplier from treating an incomplete equipment scope as a turnkey ventilation commitment.
If the ductwork discharges to a wet scrubber, identify the handoff point and review the associated equipment scope. QEEHUA’s PP sheet for wet scrubbers guide can help frame the fabricated-equipment discussion, but it does not replace process, ventilation, or emissions engineering for a specific installation.
Ask for the Acceptance and Handover Record Up Front
Include the required drawing approvals, material identification, fabrication inspection, packaging, delivery, and turnover documents in the RFQ. If the buyer requires a particular test, method, witness point, or report format, name it before quotation. Do not convert general ventilation guidance into an unagreed acceptance test; the project owner and responsible engineer must define the acceptance basis.
PP Sheet Production Context for the RFQ
The RFQ should distinguish material supply and fabricated ductwork from the system’s capture and ventilation performance design. The following QEEHUA video is included only as context for PP sheet production; it does not demonstrate acid compatibility, duct sizing, capture performance, or commissioning.
Video reference: “PP Sheet Extrusion: Pneumatic Control Panel | QEEHUA” shows a PP sheet production control stage. It is relevant only to material-production context and does not validate a ductwork RFQ or a finished extraction system.
FAQ
What process data should an acid fume ductwork RFQ include?
Include the identified emission points, chemical names, concentrations, temperatures, mist or vapour conditions, operating modes, and any cleaning or upset conditions the process owner can provide.
Should an RFQ state the airflow for PP ductwork?
Yes. Include the airflow or pressure basis supplied by the responsible ventilation designer, or explicitly state that it remains to be provided. A material supplier should not be asked to assume the ventilation duty.
What drawings are useful for a PP ductwork quotation?
Provide plans, elevations, sections, and an isometric or spool schedule when available. Mark routes, bends, branches, transitions, connection interfaces, supports, clearances, access points, and items by others.
Does a PP ductwork RFQ prove chemical suitability?
No. The RFQ supplies the service data needed for review. QEEHUA-specific material suitability and fabrication details require confirmation against the actual project conditions.
Send QEEHUA a drawing-led ductwork request
Share the equipment layout, process conditions, connection details, required documentation, and the defined scope of supply. QEEHUA can then review the PP material and fabricated-component request with the project information in view.

