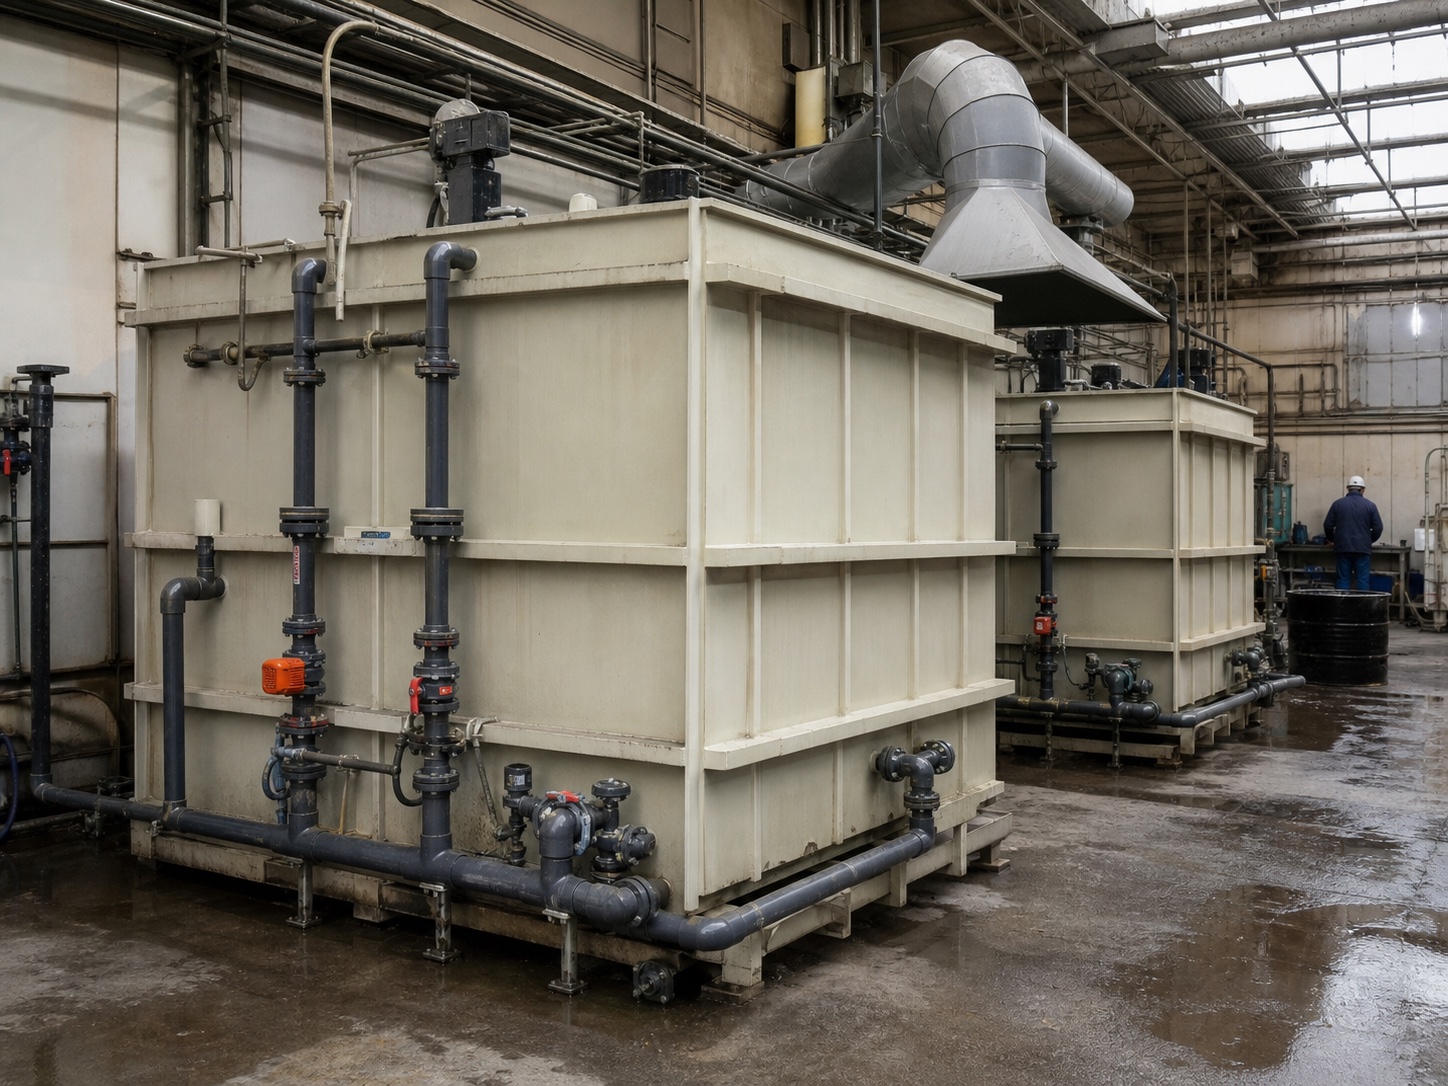
PP sheet for chemical tanks is assessed against the actual project duty. PP sheet can be a practical material for fabricated chemical tanks, scrubber sumps, process enclosures, and related equipment when the proposed sheet is confirmed for the actual duty. Start with the chemical name, concentration, continuous and peak temperature, equipment geometry, support layout, joint design, and any outdoor or fire requirement. QEEHUA’s chemical-resistance table is useful for early screening, while the final material decision needs the project conditions. A tensile or temperature figure alone does not define a safe tank design. Send the operating information with the drawing so the sheet, fabrication route, and sample can be reviewed together.
PP sheet chemical tanks should be reviewed against the documented project duty, drawings, fabrication scope, material records, and acceptance requirements.
Project duty
PP sheet chemical tanks: project review
Use the documented project requirements to compare the relevant material, fabrication, and quality-control inputs before release.
A material inquiry is easier to review when it describes the duty in process terms. Identify every liquid, vapour, cleaning chemical, and possible upset condition that will contact the sheet. Record concentration, operating temperature, cleaning temperature, pressure or vacuum, and whether the condition is continuous or intermittent. For a tank, include liquid height, panel dimensions, stiffener arrangement, outlet locations, supports, and transport constraints. For a scrubber or enclosure, include the expected condensate, gas stream, and inspection access.
This information separates a simple material question from an equipment design question. A wall panel may see local load near a nozzle, a welded corner, or a support point that is not represented by a coupon test. The drawing and duty sheet should therefore travel with the material request. QEEHUA’s industry applications page is a useful starting point for matching a project to common fabrication uses, but it does not replace project confirmation.
Duty sheet
A workable duty sheet normally fits on one page: medium and concentration; normal and maximum temperature; dimensions and liquid height; pressure or vacuum; installation location; joining method; and the performance requirement that matters most. If a requirement is unknown, mark it as open rather than assuming a typical value. That gives the engineering team a clear list of points to close before material is released.
Chemical screening
QEEHUA’s internal product data includes a chemical-resistance reference table for individual media at stated temperatures. Use it to narrow the options, then verify the exact duty. Chemical name alone is not enough. Concentration, temperature, exposure time, mechanical stress, and mixed media can change the result. The same discipline is reflected in ASTM D543, a practice for evaluating plastics against chemical reagents.
Ask for the commercial or trade name when a process fluid contains additives, surfactants, solvents, or proprietary cleaners. Do not convert a single table entry into a claim that PP is suitable for every acid, alkali, solvent, or temperature. If the medium or operating window is outside the available internal reference, record the item as requiring project confirmation.
Relevant data
Material data is an input to the design, not the design itself. Tensile, flexural, impact, and heat-deflection results help an engineer compare a proposed sheet with the project requirement. They do not establish wall thickness, stiffener spacing, nozzle reinforcement, or an allowable service temperature on their own. Those decisions depend on geometry, load, joint efficiency, safety factors, and the service environment.
The current QEEHUA PP sheet data sheet provides the following reported results. Each row retains the unit, method, condition status, and source so that a number is not separated from its evidence.
| Property | Reported result | Product and test condition | Method |
|---|---|---|---|
| Density | 912 kg/m³ | QEEHUA PP sheet data-sheet sample; specimen conditioning not stated | ASTM D792-20 |
| Tensile strength | 30 MPa | QEEHUA PP sheet data-sheet sample; specimen conditioning not stated | ASTM D638-22 |
| Flexural modulus | 1,870 MPa | QEEHUA PP sheet data-sheet sample; specimen conditioning not stated | ASTM D790-25 |
| Deflection temperature under load | 137.0 °C | QEEHUA PP sheet data-sheet sample; specimen conditioning not stated | ASTM D648-18 |
Scope of the data: these are reported results for the data-sheet sample, not universal design allowables or a continuous service-temperature rating. The current sheet lists homopolymer and copolymer options without assigning every result to a saleable grade. Confirm the grade, fabrication conditions, and project design basis before specifying material.
Fabrication checks
Tank performance is shaped by the fabricated assembly. Define the welding process, joint form, filler selection, inspection points, and access for welding before the sheet order is finalized. If the equipment uses thermoplastic welding, include the material and profile request for the matching PP welding rods. Where an edge, channel, or reinforcement detail is required, describe the profile and dimensions rather than selecting a standard part by name alone.
Arrange the fabrication sequence so that the welder can reach seams and inspect them. Flatness, handling marks, cut edge quality, storage temperature, and transport support may matter more on a large panel than on a small test piece. A realistic sample should represent the intended sheet and, when relevant, the proposed joint or machined feature.
Fire and outdoor checks
The data sheet reports separate UL 94 V-0 and V-2 results, but it does not tie those results to every commercial grade. Treat fire performance as a grade-specific item for confirmation. The same approach applies to outdoor exposure. The data sheet includes an ASTM G154 accelerated-weathering result; it is not a published outdoor life promise. State the location, expected exposure, and required approval in the inquiry.
Equipment scope
Supply requests are most useful when they describe the equipment rather than only the sheet size. A tank fabricator may need cut panels, welding rod, and a detail for a top flange. An OEM may need a repeatable sheet format for an enclosure or treatment module. A contractor may need material for a replacement lining component. QEEHUA’s PP sheet range is the base material reference. For a profile requirement, review the PP U-shaped slots page and send the drawing with the request.
Use the same file to identify the quantities for a sample, pilot build, and production lot. That prevents a technical review from being mistaken for a quotation or a production commitment. When the project needs a property outside the current data sheet, name the test method, acceptance value, specimen direction, and condition that the project requires.
Sample request
For a useful project sample, send the application, chemical medium and concentration, normal and maximum temperature, drawing or panel dimensions, preferred thickness, colour if relevant, welding or machining plan, and the test or approval requirement. Include the installation environment if the equipment will be outdoors or has a fire-performance condition. The QEEHUA team can then check the request against the available product information and identify which items still need confirmation.
Request a project sample or send your equipment drawing. A complete inquiry makes it possible to discuss the proposed material without treating a generic data point as an approval for the whole assembly.
Frequently asked questions
Can PP sheet be selected from the chemical name alone?
No. The review should include concentration, normal and maximum temperature, exposure time, mixed media, mechanical loading, and the equipment design. The chemical table is an initial screen, not a blanket approval.
Does a deflection-temperature result set the continuous operating temperature?
No. It is a laboratory result under the stated method. Continuous service temperature depends on the grade, chemical medium, load, geometry, joints, and the project design basis.
When should welding rods be included in a PP sheet inquiry?
Include them whenever the fabricated equipment will use thermoplastic welded joints. State the proposed sheet, joint type, welding process, and required profile so material compatibility can be reviewed with the assembly.
What should be sent for a sample review?
Send the duty information, drawing, requested dimensions, fabrication plan, and any test or approval requirement. If a point is undecided, identify it as open for project confirmation.
For PP sheet chemical tanks, record the final project assumptions and acceptance checks before releasing the fabrication or purchase scope.