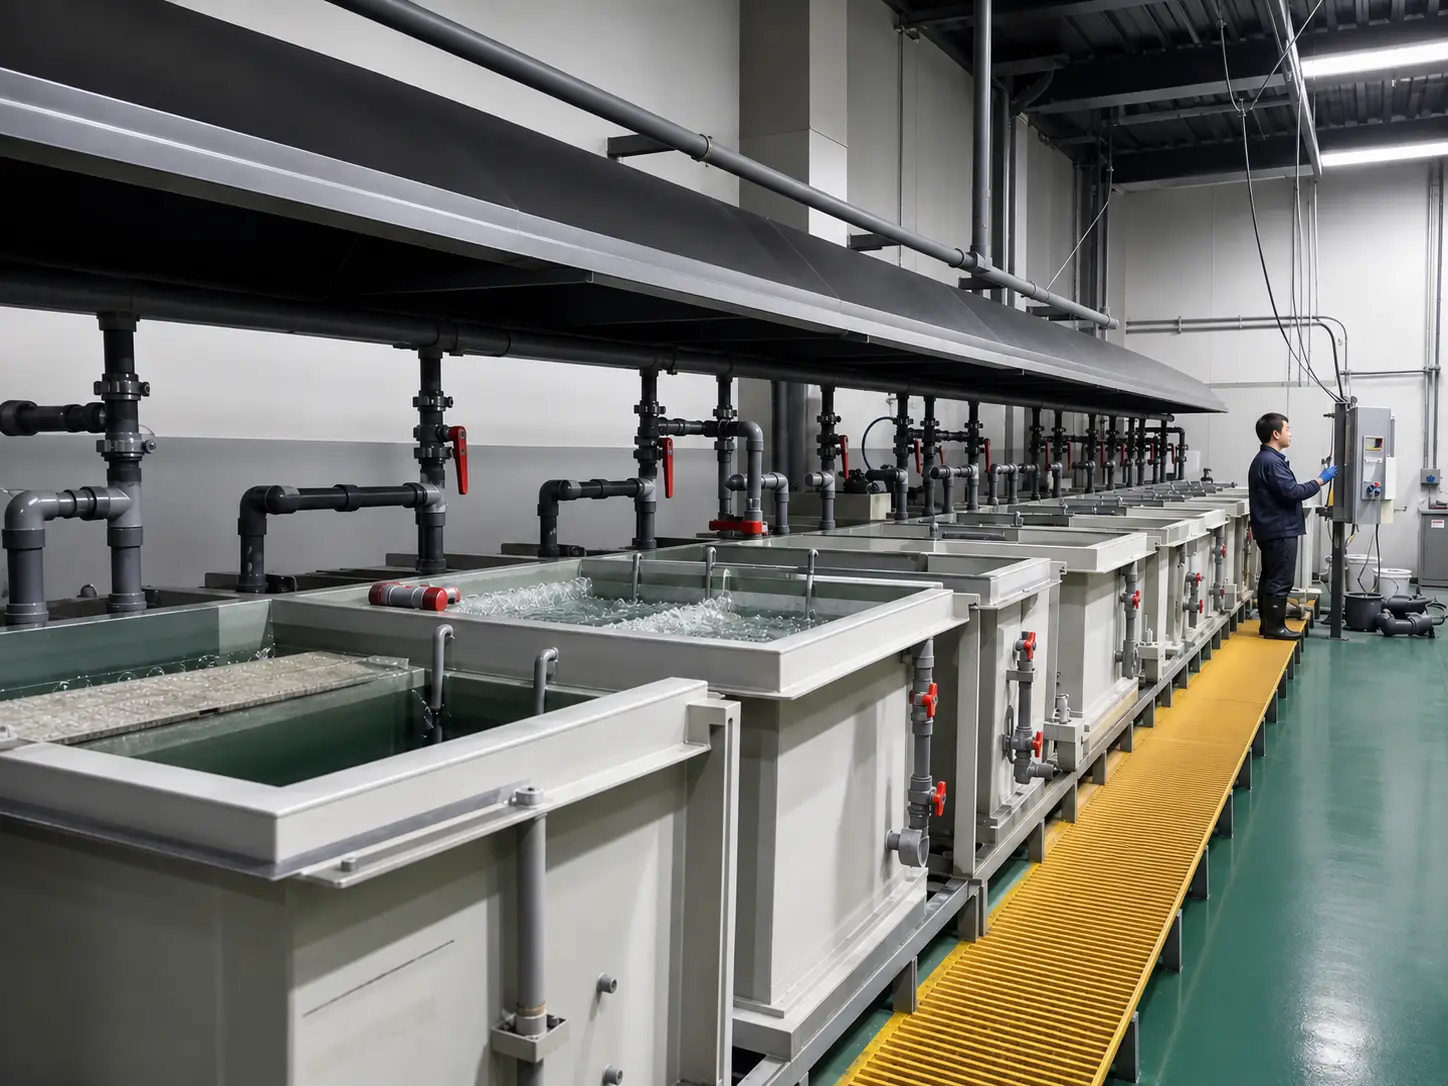
PP sheet for electroplating tanks is assessed against the actual project duty. Electroplating tank selection should start with the actual equipment duty and drawing. Electroplating equipment can include process baths, rinses, and cleaning chemistry. List every fluid, its concentration, normal and maximum temperature, liquid height, nozzles, supports, access points, and any local heat source. PP sheet can be considered only after those conditions are reviewed. The material request needs the chemical, temperature, geometry, support, joint, and inspection information that applies to the finished assembly. QEEHUA internal data can support a first material discussion, but it should not be expanded into a grade-wide promise, an equipment design calculation, or an approval for unlisted conditions. Send the project information with the sample request so the proposed sheet, rod, or profile can be reviewed against the real use before material is released.
PP sheet electroplating tanks should be reviewed against the documented project duty, drawings, fabrication scope, material records, and acceptance requirements.
Project duty
PP sheet electroplating tanks: project review
Use the documented project requirements to compare the relevant material, fabrication, and quality-control inputs before release.
Electroplating equipment can include process baths, rinses, and cleaning chemistry. List every fluid, its concentration, normal and maximum temperature, liquid height, nozzles, supports, access points, and any local heat source. PP sheet can be considered only after those conditions are reviewed.
Use the QEEHUA industry applications page as context for the equipment category. The final decision needs the stated project information and should not rely on a generic application label.
Treat each liquid-contact zone as a separate line on the duty sheet. A plating bath, an activation bath, a rinse, and a maintenance cleaner may not have the same concentration or temperature. The drawing should show which surfaces see each liquid, including the tank bottom, weir, return area, drain connection, and any secondary containment.
The equipment drawing also needs the items that create local demand. Record the operating liquid level, overflow route, pump or return nozzles, heater or coil location, access cover, and any lifting or support points. These are equipment details, not material-property questions, so they need to stay with the fabrication review.
Material role
The QEEHUA PP sheet range is the base product reference. The selection question is whether the proposed material, construction detail, and service conditions work together. A panel, a welded joint, a profile, and a support interface can have different demands in the same equipment.
Separate the initial material screen from the equipment approval. This keeps a useful data-sheet discussion from being mistaken for a design calculation or a production commitment.
Conditions to confirm
Service conditions
State every relevant medium, concentration, normal and maximum temperature, exposure duration, cleaning condition, and upset condition. If the project includes no chemical contact, state the installation environment and operating temperature instead. Do not infer performance from a similar chemical or a broad process name. The same condition-based approach is reflected in ASTM D543.
Geometry and support
Record panel spans, liquid height or process load, positive or negative pressure where relevant, supports, penetrations, reinforcement, welding access, and inspection points. These details determine what the fabricator and project engineer need to review.
Use the chemical name used by the process owner, not a broad label such as “plating solution.” State the concentration and the normal and maximum temperature for every bath. If a proprietary additive, brightener, cleaner, or rinse aid is present, identify it as an open item. A preliminary table entry cannot confirm a mixed process liquid without those details.
Wall panels see more than a coupon test. A full tank can have liquid head, a local nozzle load, an unsupported edge, a welded corner, or a stiffener connection. The project engineer should define the support arrangement and inspection access before a sheet thickness or fabrication route is accepted. This article does not provide a tank-wall calculation.
Relevant data
The following table keeps the reported data or required project inputs with the condition that gives them meaning. It is not a substitute for the equipment design basis.
| Project data | Reported value or input | Material or condition | Method or check |
|---|---|---|---|
| Density | 912 kg/m³ | Tested PP sheet sample | ASTM D792-20 |
| Tensile strength | 30 MPa | Tested PP sheet sample | ASTM D638-22 |
| Flexural test result | 1,870 MPa | Tested PP sheet sample | ASTM D790-25 |
| Deflection temperature under load | 137.0 °C | Tested PP sheet sample | ASTM D648-18 |
Scope of the data: The reported values are for a tested PP sheet sample. They are not design allowables or universal grade claims. Confirm the material, service conditions, geometry, support, and joints for the project.
Before a buyer compares sheet options, make one equipment list that links every tank component to its duty. Include the main tank wall, floor, cover, weir, nozzle zone, support interface, and any secondary containment. This makes it possible to identify where the same material screen applies and where a separate project check is required. It also prevents a test result for one sample from being applied to an unrelated fabrication detail.
Fabrication checks
Define the cut edges, joint type, sequence, access, process equipment, and inspection requirement before issuing the production request. When a thermoplastic welded detail is involved, include the matching PP welding rod request. When a channel or reinforcement feature is involved, include the PP U-shaped slot section drawing and mating dimensions.
Joint quality and finished-equipment performance depend on the assembly process. The safest specification is the one that makes the drawing, service duty, material, and inspection condition visible to the same review.
Set the fabrication sequence before the order is released. The drawing should identify seam locations, joint access, nozzle installation order, any post-weld machining, and the inspection points that matter to the buyer. If a joint must be assessed with a coupon, state the joint form and the acceptance method. A material sample does not represent a finished tank unless the sample is agreed as a fabrication sample.
Sample request
Send the drawing, equipment use, chemical and temperature information where relevant, requested dimensions, fabrication route, sample purpose, and any test or approval requirement. Request a project sample or submit the equipment information. An open point should be marked as open, not replaced with an assumed typical condition.
For a related selection example, see the QEEHUA PP sheet guide for chemical tanks. It explains why the product data and the project duty must be read together.
For a project where the risk is a welded corner, nozzle area, or reinforcement detail, request a sample that represents that detail rather than a loose sheet piece. Send the current drawing revision with the request and state what the sample will be checked for. That gives the material, fabrication, and quality teams the same reference.
Frequently asked questions
What information is needed for a electroplating tank review?
Provide the equipment drawing, service conditions, dimensions, fabrication route, quantity, and any inspection or approval requirement.
Can a single data-sheet value approve the full assembly?
No. Material test results are inputs to a project review. The final assembly also depends on geometry, loads, supports, joints, service conditions, and the design basis.
Why should the drawing be sent with the material request?
The drawing shows spans, penetrations, supports, joint access, and interfaces that cannot be determined from a material name or panel size alone.
What should be included with a sample request?
Send the project duty, drawing, requested material or detail, fabrication plan, sample purpose, and acceptance requirement so the sample can be discussed against the real use.
For PP sheet electroplating tanks, record the final project assumptions and acceptance checks before releasing the fabrication or purchase scope.