
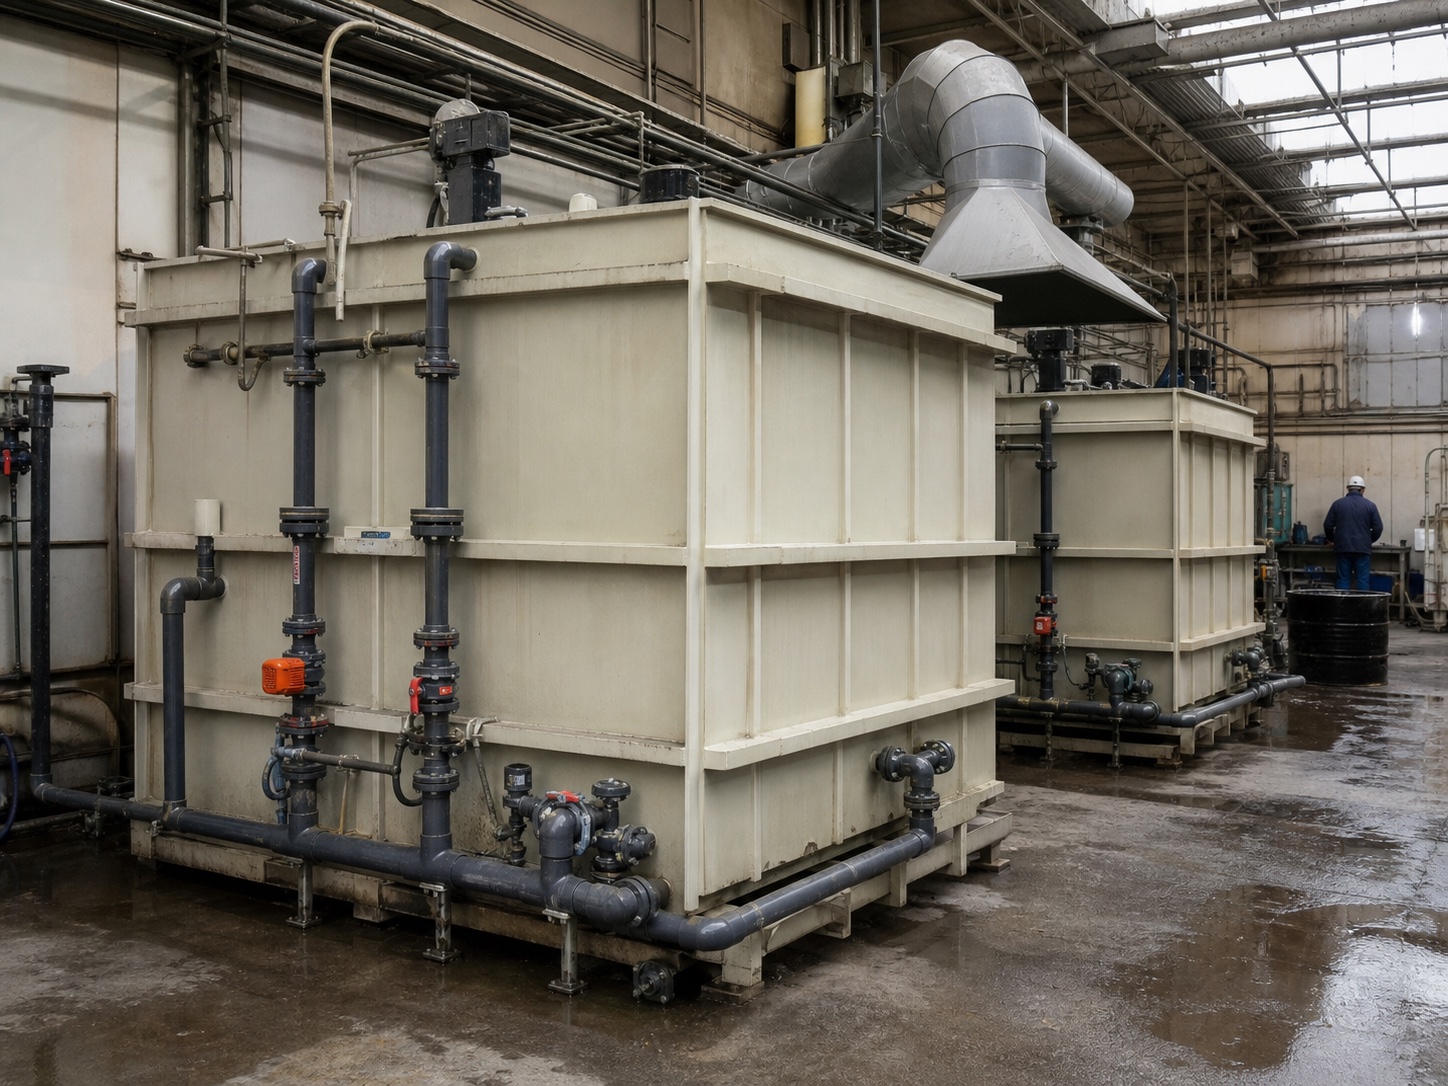
PP sheet can be a candidate for a battery charging tank or electrolyte tank when the electrolyte concentration, temperature, exposure cycle, support arrangement, and cleaning method are defined and confirmed. It is not enough to write “acid resistant PP” on a purchase order. The tank, welds, ventilation interfaces, drainage, and secondary containment must be reviewed as one system.
Lead-acid battery electrolyte is dilute sulfuric acid, and charging can release hydrogen and electrolyte mist. For a battery charging area, OSHA requires designated charging areas, ventilation, acid-resistant construction, spill-flushing arrangements, and protection against electrolyte exposure. The material decision should therefore begin with the process and safety boundary, then move to the PP sheet and fabrication details. QEEHUA’s PP sheet chemical-tank selection guide provides the broader material-screening path; the PP Sheet selection and fabrication guide gives the wider material-to-application context, while this article narrows it to battery charging and electrolyte handling.
Define the battery duty before choosing a sheet
A charging tank, acid-filling tank, battery immersion tank, and spill tray can all be called a “battery tank,” but they do not impose the same duty on the PP sheet. Record the process boundary before asking for a quotation.
| Input to document | Why it changes the PP tank decision |
|---|---|
| Battery chemistry and electrolyte identity | Lead-acid electrolyte is different from alkaline or mixed battery chemistries. Do not transfer a PP recommendation between chemistries without a new compatibility review. |
| Concentration, normal temperature, and peak temperature | Resistance references are conditional. A result at ambient temperature cannot be treated as proof for a hotter charging or cleaning cycle. |
| Contact time and operating cycle | Intermittent filling, continuous immersion, charging, draining, and washdown create different exposure histories. |
| Liquid depth, tank footprint, and support points | Hydrostatic load and panel span affect reinforcement, supports, weld layout, and dimensional stability. |
| Gas, mist, drainage, and spill path | Ventilation, drain routing, curbs, and emergency containment are part of the equipment interface, not optional accessories. |
OSHA’s battery-charging requirements call for ventilation to prevent an explosive gas mixture and for acid-resistant construction. The agency also identifies quick drenching or flushing facilities and electrolyte-resistant racks or trays as part of the charging-area controls. See OSHA 1926.441 and its battery electrical-source guidance, then confirm which occupational-safety rule applies to your facility.
When PP sheet is a reasonable candidate—and when it is not automatic
PP sheet is worth screening when the electrolyte is known, the concentration and temperature are bounded, the tank is a welded fabricated component, and the project can define supports and inspection. That is a starting condition, not a blanket approval.
QEEHUA’s internal PP chemical-resistance reference lists individual media at 20°C, 60°C, and 100°C and uses rating categories tied to changes such as swelling, weight loss, and tensile behavior. It is useful for early screening, but the table does not replace a project review. If the tank also handles dosing or cleaning chemicals, compare the duty with the PP dosing-equipment selection guidance rather than transferring a recommendation without review. The RFQ should identify the exact electrolyte concentration, highest operating and cleaning temperature, exposure duration, and whether the liquid is contaminated with lead, additives, or other chemicals.
Design a battery charging tank and its interfaces as one system
A battery tank needs more than a liquid-tight box. The drawing should show how batteries enter and leave, where acid can drain, how the tank is supported, and how ventilation and electrical equipment stay outside the chemical boundary.
- Loading and access: define battery size, insertion direction, lifting method, clearance, removable covers, and the cleaning access required after a spill.
- Freeboard and overflow: show the normal fill level, maximum upset level, overflow path, and a drain that does not create an uncontrolled discharge.
- Support and movement: state whether the PP tank sits on a continuous base, a frame, or local supports. Large spans and point loads need a separate structural review.
- Battery charging ventilation boundary: coordinate the hood, room exhaust, tank cover, and any duct connection. A tank material choice cannot substitute for a ventilation design.
- Secondary containment: specify the curbed or lined area that receives a leak, washdown liquid, or damaged battery. EPA guidance describes non-reactive, impermeable, curbed surfaces and leak-proof containment as important battery-storage controls; see the EPA auto-battery storage guidance for the relevant handling context.
For a fabricated tank, include the liquid depth, panel spans, support locations, nozzle or drain loads, and thermal movement assumptions in the drawing package. These inputs let the fabricator distinguish a self-supporting vessel from a PP liner or a tray inside a metal frame. Drain and cleanout interfaces should also be coordinated with the PP equipment drainage and cleanout access guide.
Control PP sheet fabrication and welding
Battery service exposes weak fabrication details quickly. The RFQ should identify the PP sheet grade or approved material family, thickness range, surface condition, welding rod compatibility, joint preparation, and inspection method. “Virgin PP” by itself is not a complete welding specification.
QEEHUA’s project review normally separates the material record from the weld record: the parent sheet, welding rod, batch or lot information, joint detail, operator or process requirements, and any repair or retest decision should remain traceable to the finished tank. The welding rod should match the confirmed parent material; the PP welding-rod selection guide is useful for the consumable review. If the tank has thick panels, deep corners, inserts, or restricted access, request a fabrication sequence and representative test weld before release.
The following QEEHUA sheet-formation video gives general manufacturing context for a PP material enquiry. It does not establish electrolyte compatibility, tank thickness, welding acceptance, or battery-area safety.
Video reference: “PP Sheet Extrusion: Sheet Formation Process | QEEHUA” is a general sheet-manufacturing reference only; the battery-tank RFQ still needs project-specific chemical, geometry, welding, and acceptance inputs.
Turn the decision into a useful battery-tank RFQ
A supplier cannot confirm a PP battery charging tank from a capacity number alone. A battery charging tank RFQ should connect the process duty to the fabricated part and its acceptance evidence through a controlled schedule.
| RFQ section | Information to provide | Expected review output |
|---|---|---|
| Process duty | Battery type, electrolyte name, concentration range, normal and peak temperature, cycle time, and cleaning chemicals | Compatibility screening and information gaps |
| Geometry | Internal length, width, depth, freeboard, access openings, drains, overflow, and lifting or loading clearances | General arrangement and interface review |
| Loads and support | Liquid depth, battery weight, point loads, frame or base details, seismic or transport requirements where applicable | Support and reinforcement scope |
| Fabrication | Sheet grade, thickness, color or surface requirement, welding rod, joint detail, inserts, and repair limits | Fabrication route and traceability plan |
| Safety interfaces | Ventilation connection, acid mist control, drainage destination, secondary containment, eyewash and emergency access responsibilities | Responsibility split between tank, building services, and site safety design |
| Inspection and handover | Dimensional checks, weld visual criteria, leak-test method, cleaning or packaging requirement, drawings, material records, and test reports | Release dossier and acceptance checklist |
For larger or heated equipment, distinguish the tank supplier’s fabrication scope from the site’s ventilation, electrical, lifting, and hazardous-area responsibilities. The PP tank RFQ checklist can be used for the general quotation package, while this battery-specific schedule carries the electrolyte and charging-area details.
Inspection points before the tank is accepted
Before a battery charging tank is accepted, confirm the finished tank, not only the raw sheet certificate. Check the released drawing revision, dimensions and openings, support contact, weld continuity, drain and overflow orientation, visible contamination, and the agreed leak-test record. If the tank will be cleaned before shipment, record the cleaning method and packaging condition so the site does not receive an untraceable surface.
Keep the chemical-resistance basis, sheet and welding-rod records, fabrication drawings, inspection results, and any repair or retest notes together. This documentation makes a later electrolyte change or temperature increase a controlled engineering decision instead of an assumption based on the original purchase order.
FAQ
Is polypropylene automatically suitable for sulfuric-acid battery electrolyte?
No. PP may be a candidate for a documented electrolyte duty, but suitability depends on concentration, temperature, exposure time, stress, tank geometry, and fabrication details. Confirm the actual project conditions against a chemical-resistance reference and obtain project-specific approval before fabrication.
Can a PP battery tank replace room ventilation and acid-spill controls?
No. The tank contains liquid; it does not control hydrogen accumulation, acid mist, ignition sources, eyewash access, or emergency neutralization. Battery-area ventilation and spill controls must be designed and verified separately under the rules that apply to the facility.
What should be included in a PP electrolyte-tank quotation request?
Include the battery chemistry, electrolyte concentration, normal and peak temperature, cycle and cleaning conditions, tank dimensions, liquid depth, support and battery loads, openings, drains, overflow, ventilation interfaces, secondary containment, welding scope, inspection method, and required handover documents.
Does the PP sheet thickness come only from tank capacity?
No. Thickness and reinforcement depend on liquid depth, panel span, support arrangement, temperature, geometry, loads, and fabrication method. Capacity is one input; it cannot replace a drawing-based structural and fabrication review.
Need a battery-tank material and fabrication review?
Send the electrolyte concentration, temperature cycle, tank drawing, support arrangement, ventilation boundary, and inspection requirements. QEEHUA can help organize the PP sheet, welding, and quotation inputs for project review.

