
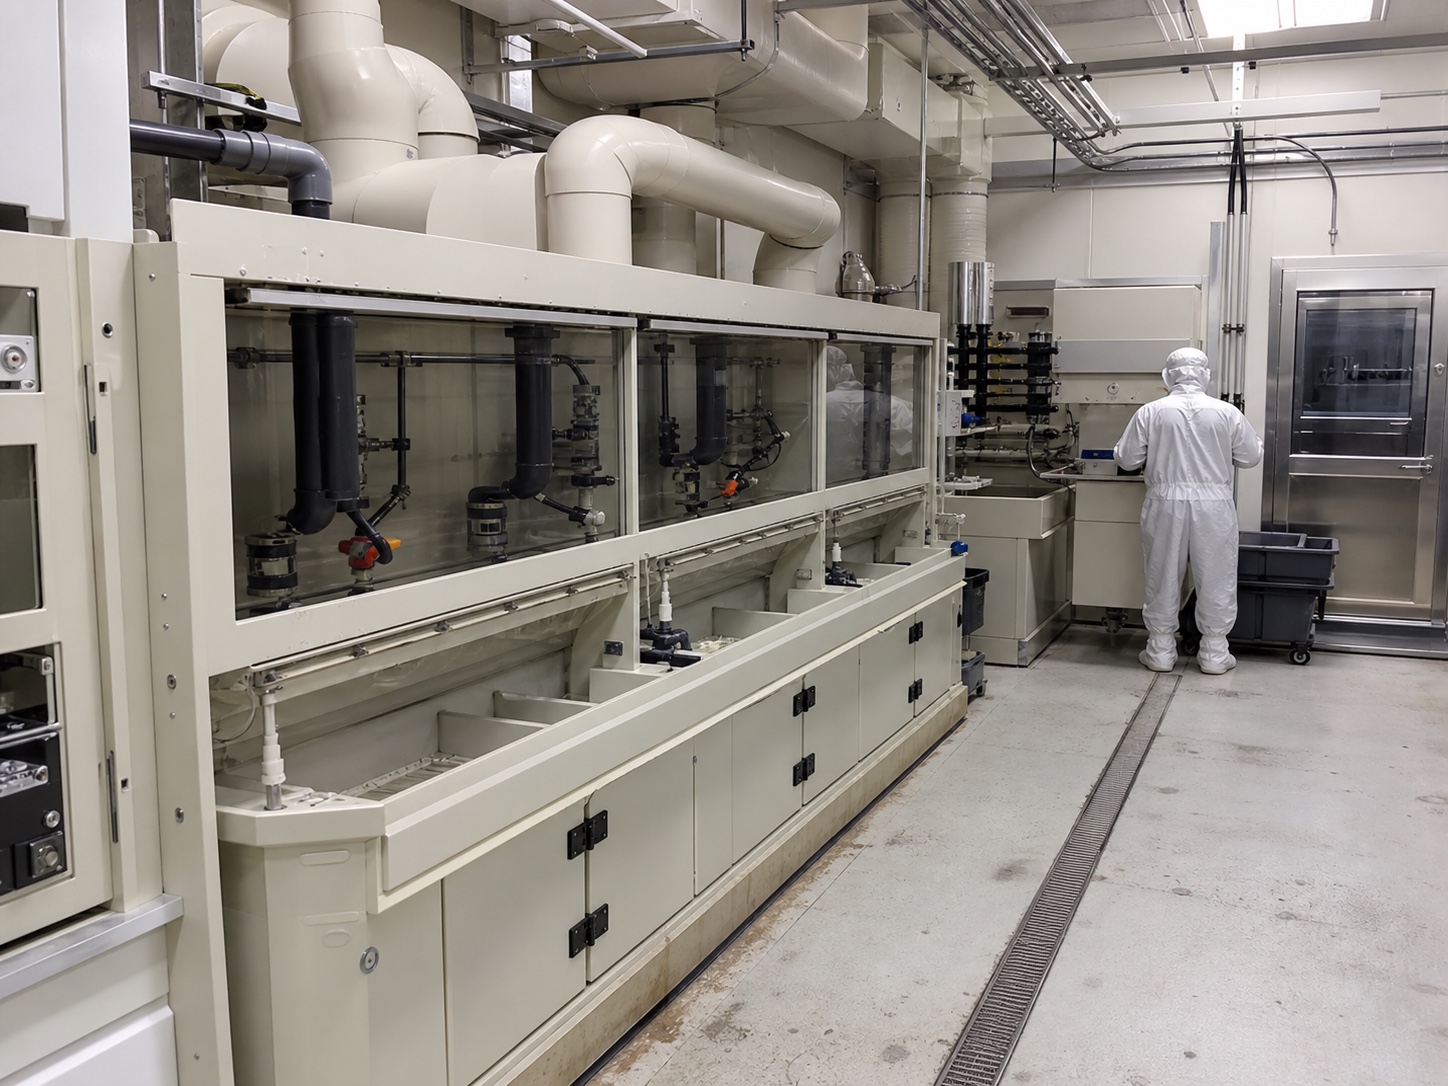
For semiconductor wet-process equipment, the right polypropylene sheet is selected by the chemical exposure, temperature, equipment geometry, welding method, cleanliness controls, and project qualification requirements—not by the word “cleanroom” alone. PP sheet can be a practical material for process screens, tank liners, splash guards, drain components, ductwork, and fabricated wet benches, but ordinary PP should not automatically be described as cleanroom grade, ultrapure, high-purity-contact, anti-static, or conductive.
This article explains the selection path: identify the wet-process problem, define the material requirements, evaluate a PP solution, and give the fabricator enough information to confirm the final sheet and fabrication details.
What problem does the customer face?
PP sheet for semiconductor wet-process equipment: project review
Use the documented project requirements to compare the relevant material, fabrication, and quality-control inputs before release.
Semiconductor wet processes expose equipment to repeated contact with process liquids, rinsing water, splashes, vapors, drainage, and cleaning operations. Screens and guards may sit close to spray zones. Tank liners and partitions may experience continuous or intermittent immersion. Ductwork and exhaust components may face chemical vapors rather than direct liquid contact.
The purchasing problem is usually more specific than “find a plastic sheet.” The customer must choose a sheet that can be fabricated into the required geometry, remain compatible with the process media, support reliable welded joints where needed, and fit the site’s contamination-control and inspection procedures. If the sheet is selected only by thickness or price, the project may later encounter distortion, difficult welding, poor fit-up, chemical incompatibility, cleaning limitations, or an approval issue.
A wet-process screen RFQ may also have requirements that differ from a tank wall. A thin screen or splash panel may need dimensional stability and cleanable surfaces. A structural tank component may require engineering review of span, support, liquid head, temperature, joints, and reinforcement. These are separate design questions and should not be reduced to a single “recommended PP thickness.”
Why does material selection become difficult in a cleanroom environment?
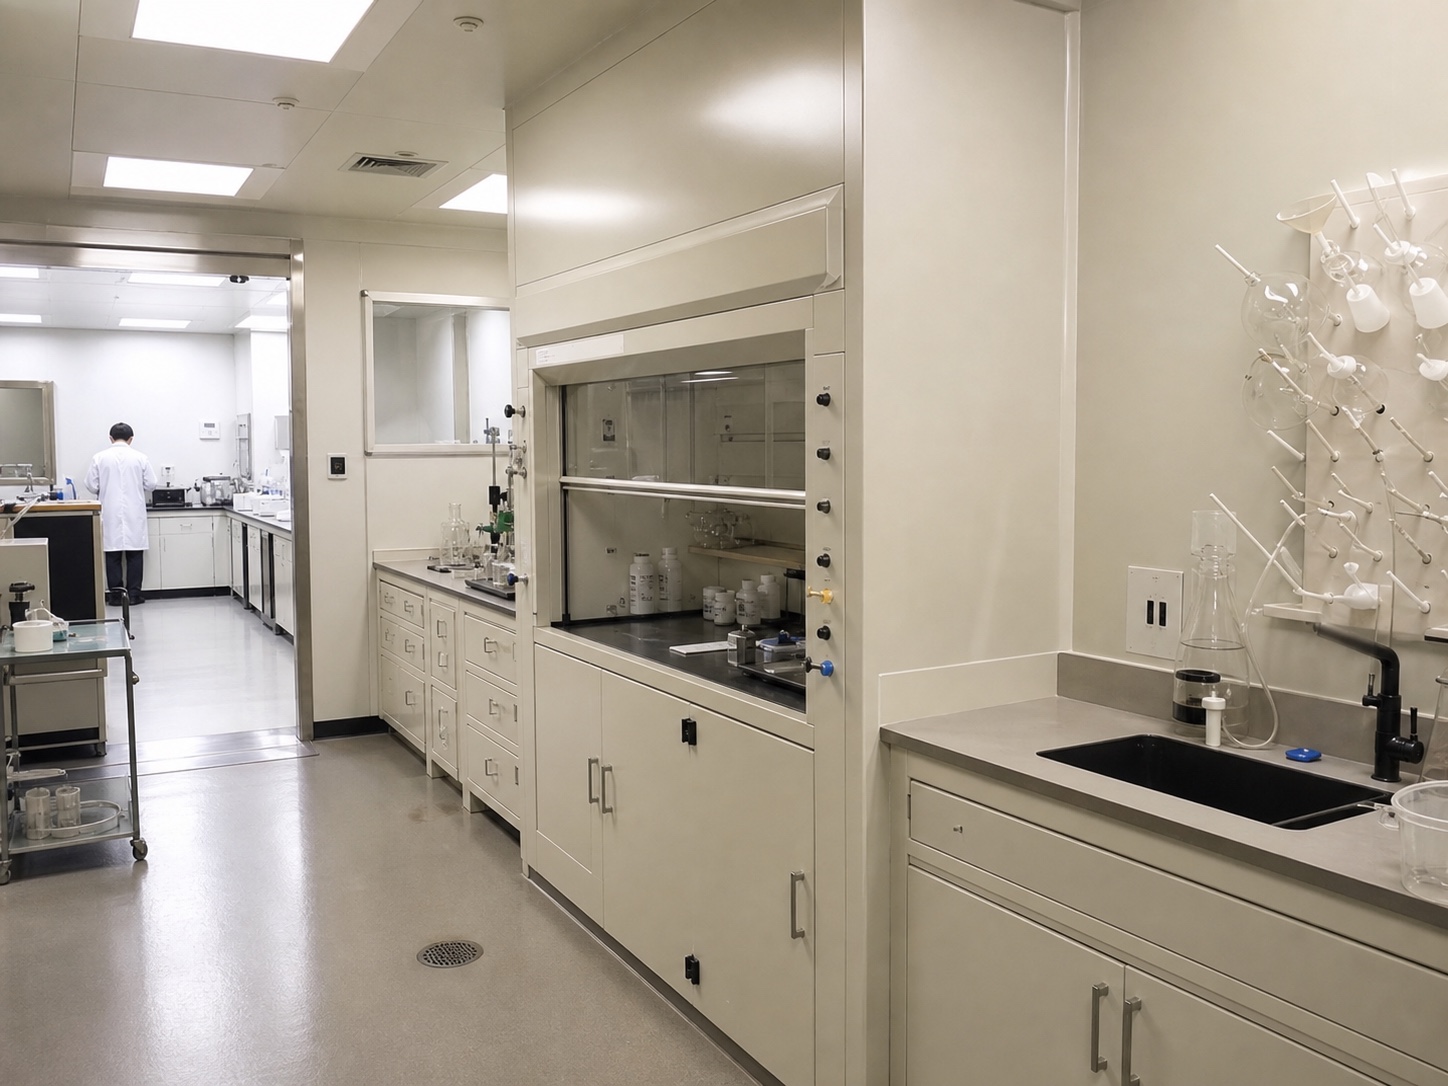
“Cleanroom equipment” describes the operating environment and contamination-control objectives. It does not, by itself, prove that a particular ordinary PP sheet has a cleanroom classification or an ultrapure-contact qualification. Those descriptions require project-specific evidence, documentation, testing, and acceptance criteria.
For this reason, a standard PP sheet should be described accurately as polypropylene sheet unless the exact grade, processing controls, surface requirements, and qualification documents have been confirmed. Do not assume that a conventional PP sheet is cleanroom grade, ultrapure, high-purity-contact, anti-static, or conductive.
The same distinction applies to chemical resistance. Polypropylene is commonly considered for many industrial chemical-handling applications, but compatibility depends on the actual chemical, concentration, temperature, exposure time, stress, weld condition, and mechanical load. A general material statement is not a substitute for a compatibility review. The project team should compare the process chemistry with documented chemical-resistance information and obtain supplier confirmation for the specific application.
What material requirements should be defined first?
Before asking for a quotation, prepare a short application specification. It should describe what the PP sheet will do, what it will contact, and how it will be fabricated.
| Selection item | Information to provide | Why it matters |
|---|---|---|
| Process media | Chemical name, concentration, mixtures, rinse water, vapor exposure, and cleaning agents | Chemical compatibility cannot be judged reliably from the industry name alone. |
| Temperature | Normal, maximum, start-up, shutdown, and cleaning temperatures | Temperature can affect chemical attack, stiffness, expansion, weld behavior, and dimensional stability. |
| Geometry | Panel size, span, supports, openings, bends, flanges, penetrations, and drainage details | Fabrication and mechanical loading often determine the practical sheet design. |
| Joining method | Hot-gas welding, extrusion welding, mechanical fastening, or another approved method | Joint design and welding procedure influence leak control and service performance. |
| Cleanliness controls | Cleaning method, packaging, handling, particle limits, and acceptance inspection | These requirements must be confirmed separately from the base resin selection. |
| Static requirements | Whether the project requires standard PP, anti-static PP, or conductive PP | Ordinary PP must not be represented as anti-static or conductive without verified product evidence. |
For chemical and regulatory context, the project team can also review the EPA semiconductor manufacturing effluent guidelines. This reference helps frame wastewater and process-discharge considerations; it does not certify a sheet, tank, screen, or fabrication method.
How can PP sheet solve the wet-process equipment problem?
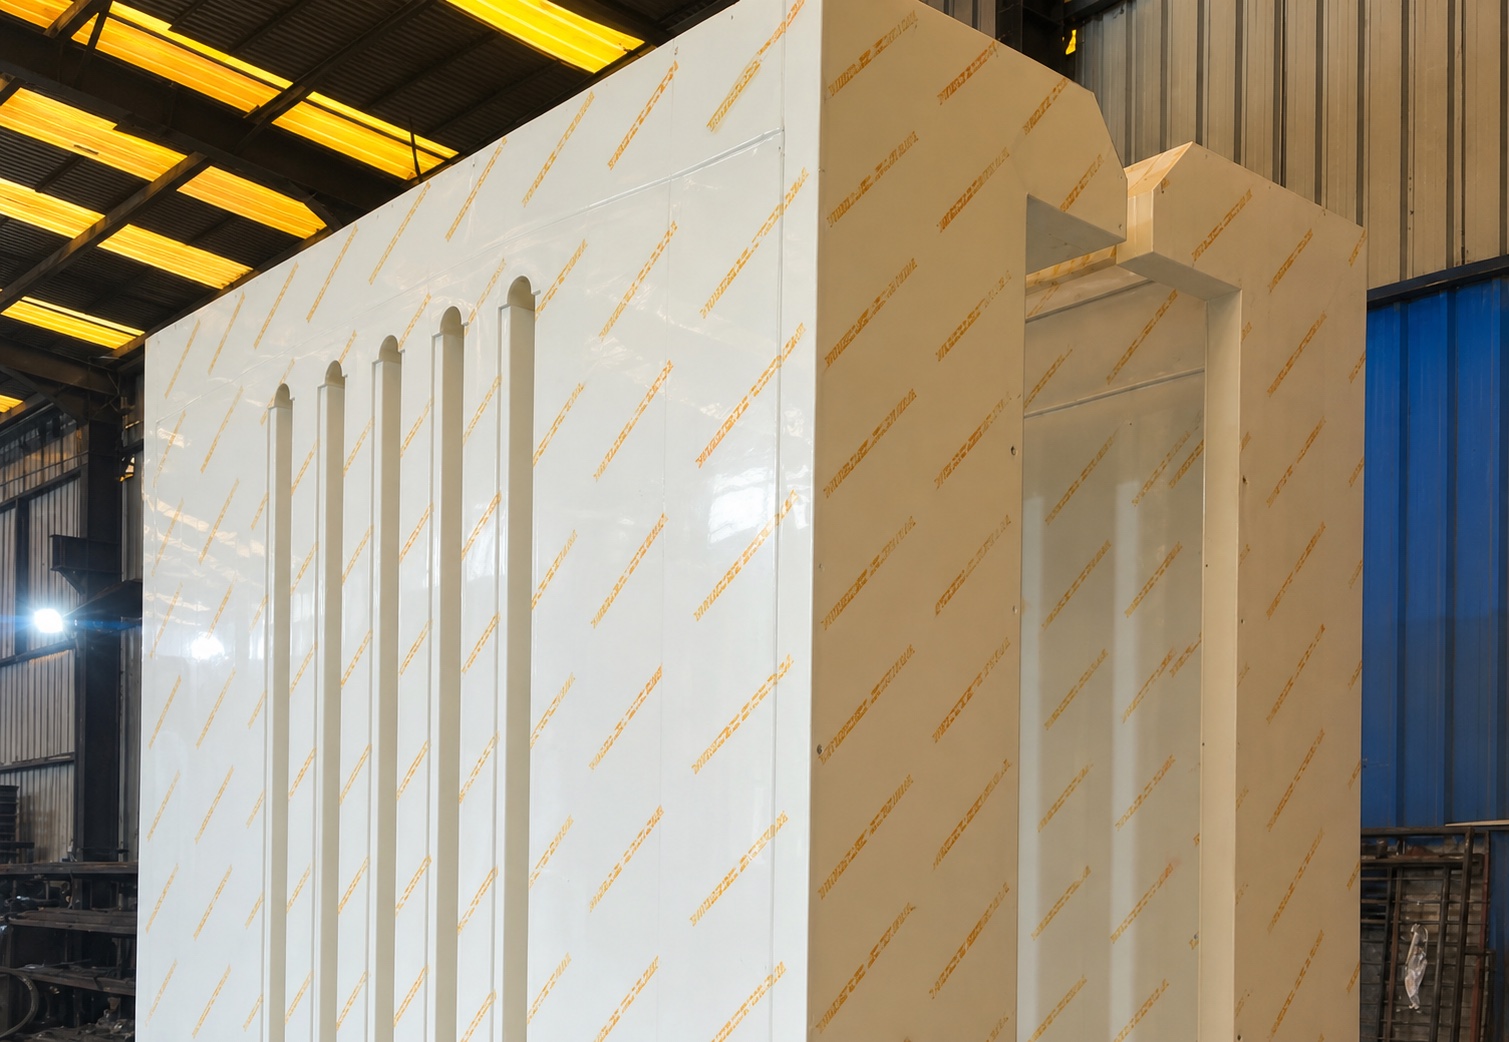
PP sheet is often considered when the equipment needs a thermoplastic surface that can be cut, formed, joined, and fabricated into process-specific components. In a wet-process system, that may include tank liners, partitions, splash guards, screens, trays, covers, drain channels, fume-hood components, or ductwork. The value of the material is linked to the complete fabricated assembly, not simply to the sheet in isolation.
For semiconductor applications, the first question is whether the selected PP grade is chemically suitable for the actual media and temperature. The second is whether the sheet can be converted into the required component without introducing unacceptable contamination, distortion, weld defects, trapped liquid, or difficult-to-clean geometry.
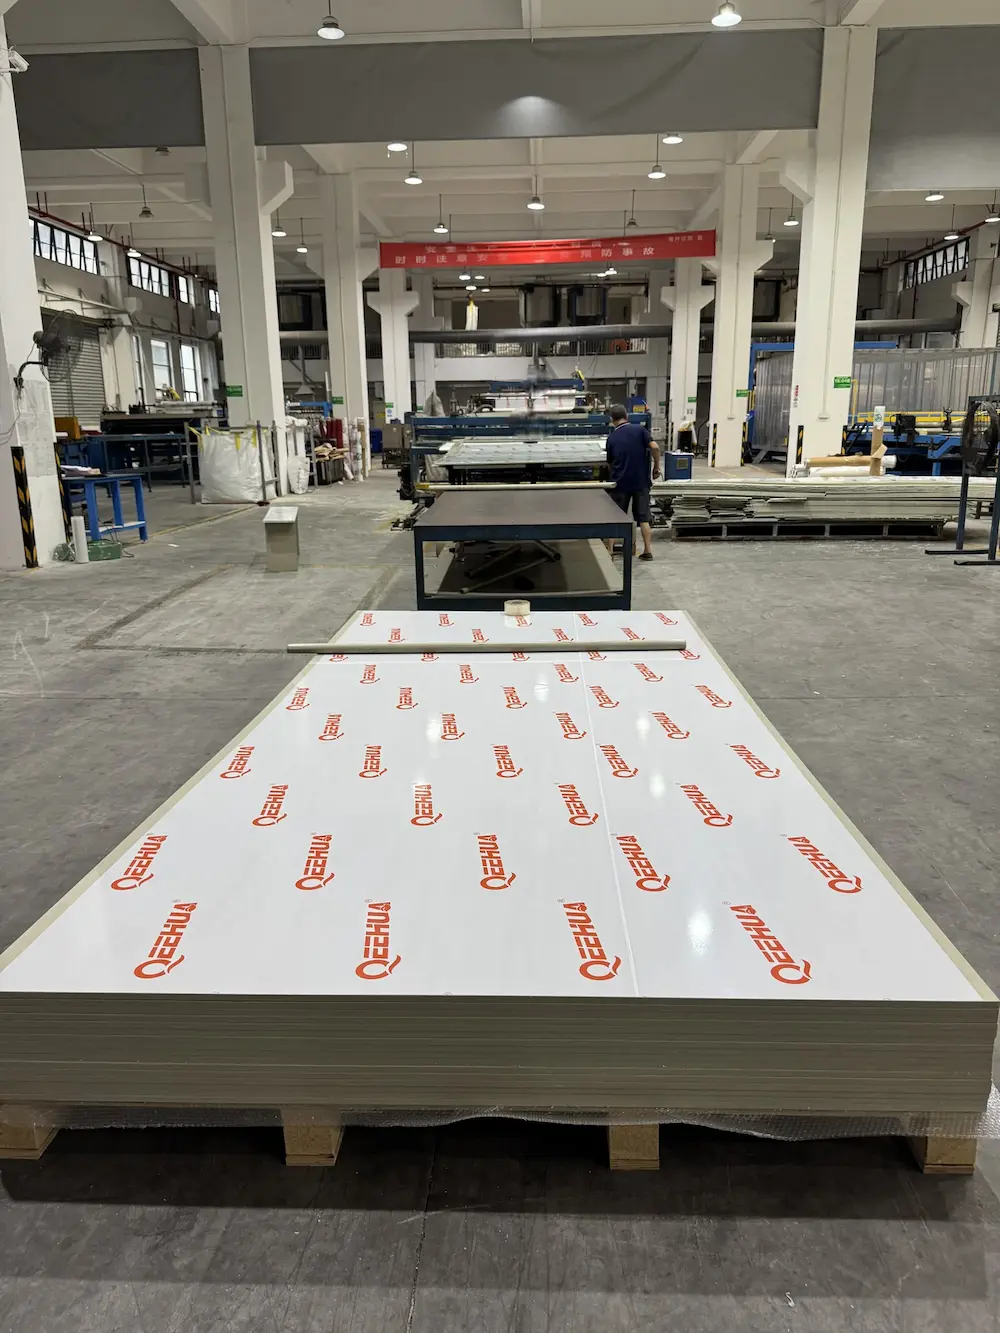
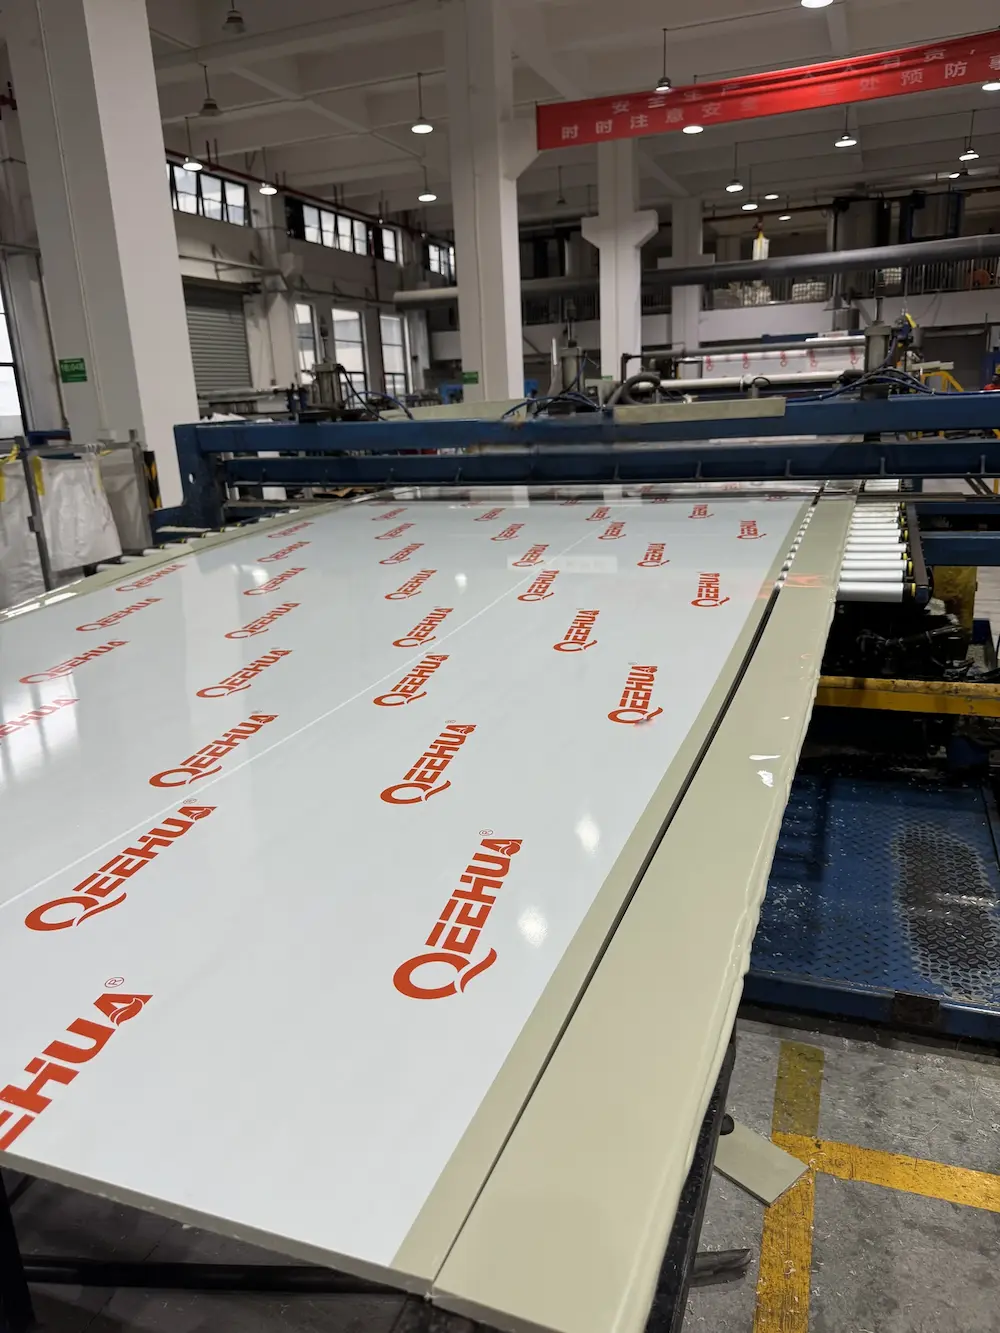
QEEHUA can be evaluated as a source for polypropylene sheet and polypropylene plastic fabrication, subject to confirmation of the exact grade, available dimensions, thickness range, surface condition, fabrication process, welding materials, inspection documentation, and project-specific cleanliness requirements. These details must be confirmed before they are written into a purchase specification.
Which PP sheet factors should buyers compare?
1. Resin and application compatibility
Ask for the exact polypropylene material designation and the intended service conditions. “PP sheet” is not a complete engineering specification. Confirm whether the sheet is homopolymer, copolymer, or another formulation, and request the supplier’s applicable technical documentation. If the project requires contact with a specific chemical mixture, provide the full exposure information rather than asking for a generic chemical-resistant polypropylene claim.
2. Thickness and support
Thickness should follow the component’s dimensions, supports, temperature, liquid head, pressure conditions, handling loads, and fabrication details. A screen, liner, and tank wall may need different design approaches. Any preliminary thickness discussion should be treated as a screening step only; final wall thickness and reinforcement require engineering review and must not be presented as a QEEHUA design guarantee.
3. Flatness, dimensions, and tolerances
Large panels can be affected by thermal expansion, storage, transport, cutting, and welding. Confirm sheet length, width, thickness tolerance, flatness expectations, edge condition, and inspection method. If the part must fit an existing wet bench or tank, provide a controlled drawing rather than relying on nominal dimensions.
4. Welding and fabrication
For welded equipment, confirm the compatible welding rod, welding process, joint preparation, operator requirements, visual inspection, leak testing, and repair procedure. A sheet quotation without a fabrication and inspection plan may leave important performance risks unresolved.
5. Surface and cleanliness requirements
Specify how the finished part will be cleaned, handled, packaged, and accepted. If the customer has particle, extractables, ionic contamination, outgassing, or other high-purity requirements, request the relevant evidence and define the test method. Do not use “ultrapure” or “high-purity-contact” as a marketing substitute for project documentation.
6. Static control
Standard PP is not automatically anti-static or conductive. If static dissipation is part of the semiconductor equipment requirement, identify it as a separate material and validation topic. Ask QEEHUA to confirm whether an appropriate anti-static or conductive PP option is actually available for the intended application, including its electrical-performance documentation and surface-cleaning limitations.
How should the procurement request be written?
A useful inquiry should let the supplier evaluate the material and the fabricated part together. Include the following information:
- Application: semiconductor wet-process screen, tank liner, wet bench component, drain part, splash guard, or ductwork.
- Process media: chemical names, concentrations, mixtures, vapors, rinse liquids, and cleaning agents.
- Operating conditions: normal and maximum temperatures, exposure duration, immersion or splash contact, and pressure or liquid-head conditions.
- Drawings: dimensions, supports, openings, bends, flanges, weld joints, penetrations, and drainage requirements.
- Material requirements: PP grade, thickness, surface, color, dimensional tolerances, and documentation.
- Cleanliness requirements: cleaning, packaging, handling, inspection, and any customer-specific acceptance tests.
- Electrical requirements: standard, anti-static, or conductive material, if applicable.
- Quality documents: technical data, certificates, inspection records, chemical-compatibility evidence, and welding documentation, where required.
When the exact QEEHUA parameter is not publicly verified, write “to be confirmed by QEEHUA” in the inquiry. This applies to available thicknesses, sheet sizes, surface finishes, resin designations, certifications, cleanroom handling, fabrication tolerances, lead time, minimum order quantity, and testing capability.
For related planning, review QEEHUA’s PP sheet selection and fabrication guide, PP sheet data-sheet guide, and PP welding joint-preparation guide. Use the QEEHUA contact page for a project-specific inquiry.
Recommended selection path
- Define the equipment part and its function.
- List every chemical, concentration, temperature, and exposure condition.
- Separate ordinary material compatibility from cleanroom or high-purity qualification.
- Confirm the required geometry, supports, thickness, joints, welding method, and inspection plan.
- Identify whether standard PP, anti-static PP, or conductive PP is required.
- Ask QEEHUA to confirm the exact product data and fabrication capability.
- Approve a drawing and procurement specification before production.
The practical recommendation is to treat PP sheet for semiconductor wet process equipment as a coordinated material-and-fabrication decision. Standard PP may be suitable for some wet-process screens and cleanroom equipment components, but the final choice depends on verified chemistry, temperature, geometry, welding, cleanliness, and project acceptance requirements. QEEHUA can be included in the supplier review once those inputs are defined and the unverified parameters are confirmed.
For a project-specific review, send QEEHUA the process media list, operating temperatures, component drawings, required quantity, cleanliness controls, and any static or documentation requirements through the QEEHUA inquiry channel.
Frequently asked questions
Is ordinary PP sheet suitable for semiconductor wet-process equipment?
Ordinary PP sheet may be suitable for some semiconductor wet-process components, but suitability depends on the process chemicals, concentration, temperature, exposure, geometry, fabrication method, cleanliness controls, and customer acceptance requirements. It should not automatically be called cleanroom grade, ultrapure, high-purity-contact, anti-static, or conductive.
Can PP sheet be used for cleanroom screens and wet benches?
PP sheet can be considered for screens, splash guards, liners, partitions, trays, and other wet-process components when the material and fabrication process meet the project requirements. The cleanroom designation must be confirmed separately through the required handling, cleaning, documentation, and validation controls.
How do I choose the thickness of PP sheet for a semiconductor tank or screen?
Choose thickness using the component dimensions, supports, span, liquid head, temperature, mechanical loads, weld design, and required dimensional stability. A general thickness value is not a tank-design guarantee; final thickness and reinforcement should be confirmed by an engineer and the fabricator.
Is polypropylene sheet chemical resistant for semiconductor wet processes?
Polypropylene may be compatible with some wet-process chemicals, but chemical resistance depends on the exact chemical, concentration, temperature, exposure time, stress, and fabricated condition. Provide the complete process-media list and request confirmation for the specific application rather than relying on a generic chemical-resistant polypropylene claim.
Is standard PP sheet anti-static or conductive?
No. Standard PP sheet should not be represented as anti-static or conductive without verified product evidence. If static control is required, specify the electrical requirement separately and ask QEEHUA to confirm the available material, documentation, and application limits.
What should I include in a QEEHUA PP sheet inquiry?
Include the equipment function, process media, concentrations, temperatures, exposure conditions, drawings, dimensions, supports, thickness target, welding method, cleanliness requirements, static requirements, quantity, delivery needs, and required technical or inspection documents. Ask QEEHUA to confirm any product or fabrication parameter that has not been verified.
For PP sheet for semiconductor wet-process equipment, record the final project assumptions and acceptance checks before releasing the fabrication or purchase scope.

