Short answer
A useful RFQ identifies whether the plate forms an overflow edge, a launder interface, or a removable component; includes a dimensioned drawing; and records the process medium, temperature, support points, hole pattern, and acceptance checks. Confirm final material and fabrication details with QEEHUA against the project design.
In a clarifier, treated water commonly leaves the settling zone over a weir and into an effluent collection arrangement. The U.S. EPA Water9 manual describes this overflow arrangement for primary clarifiers. This article focuses on specifying a fabricated PP plate component around that design—not on setting process loading rates or approving the clarifier hydraulics.
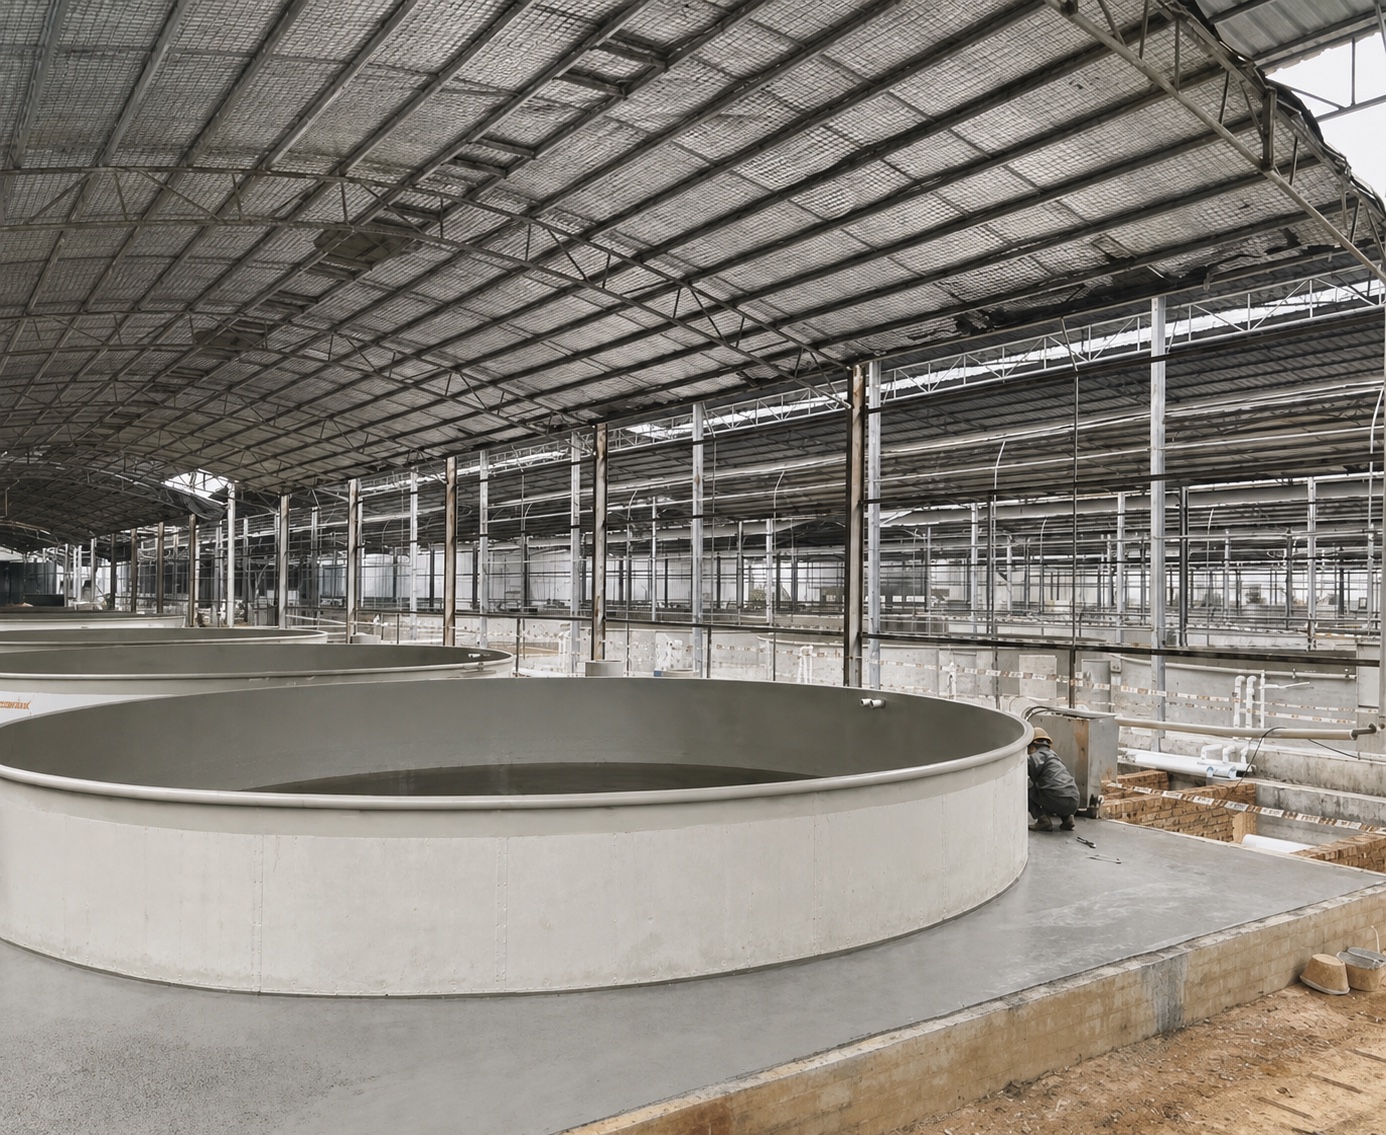
PP Sheet Weir Plates: Start with the Clarifier Function and Boundary
First state where the plate sits and what it must interface with. A perimeter overflow edge, a launder-side plate, and a removable maintenance component create different drawing, tolerance, and fixing requirements. Do not use a generic “PP panel” description when the component controls the clarified-water overflow path.
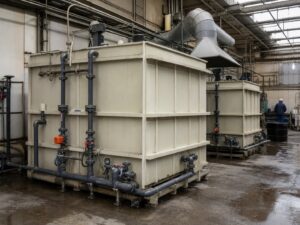
For the wider material and equipment context, link the RFQ to the existing PP sheet for wastewater-treatment equipment resource. If the project also uses internal flow-guidance panels, keep that scope separate and reference the water-treatment baffle plate RFQ checklist.
Information to include in a PP weir-plate RFQ
For PP sheet weir plates, provide the following items in one controlled drawing package. They allow QEEHUA to review the requested part as a fabrication component rather than infer critical details from a photo or an overall tank diameter.
| RFQ item | What to provide | Why it matters |
|---|---|---|
| Component role | Overflow edge, launder-side plate, internal plate, or removable section | Sets the review boundary and the relevant interface details. |
| Geometry | Plan, elevation, developed length or segment layout, and section views | Shows curvature, joints, local clearances, and the part split. |
| Hydraulic design inputs | Design flow, normal and high liquid levels, required crest elevation, and designer-approved weir arrangement | Lets the supplier identify the design data that must remain controlled by the project engineer. |
| Mounting | Support points, brackets, bolt or slot locations, backing members, and access constraints | Avoids an unspecified load path or an inaccessible fixing method. |
| Process conditions | Wastewater chemistry, concentration, temperature, cleaning method, and any solids or abrasion concern | Supports a project-specific PP material suitability review. |
| Fabrication details | Plate thickness requested by the project designer, edge finish, holes, slots, welds, and allowable joint locations | Prevents a quotation based on incomplete machining or assembly scope. |
| Acceptance | Drawing revision, dimensions to inspect, level/straightness checks, visual criteria, packaging, and installation records | Creates a practical handover checklist for the site team. |
Keep hydraulic design and component supply separate
The project engineer should establish the clarifier hydraulics, including the selected overflow arrangement and any allowable level variation. EPA training material notes that clarified wastewater can leave a settling basin over a weir and that the arrangement is part of the process path; see the EPA wastewater-treatment operation manual. A fabricated PP plate cannot validate those process assumptions on its own.
For the material component, QEEHUA can review the supplied drawing, service medium, support layout, and fabrication requirements. Include the PP-sheet grade or any required project specification rather than assuming that one sheet format suits every chemical, temperature, or structural condition. The PP sheet data-sheet guide is a useful companion when preparing the material submittal.
Specify the edges, holes, and installation interfaces
State which edges are functional overflow edges and which are covered, supported, or joined to another component. Identify all holes and slots from datums on the drawing, distinguish field-installed holes from factory-machined holes, and show clearances to launders, brackets, fasteners, and access covers.
Where a level or straight overflow edge is a project requirement, make the inspection method and acceptance authority explicit in the RFQ. The supplier can check fabricated dimensions against the approved drawing; the project designer or operator remains responsible for the final hydraulic criterion and installation alignment.
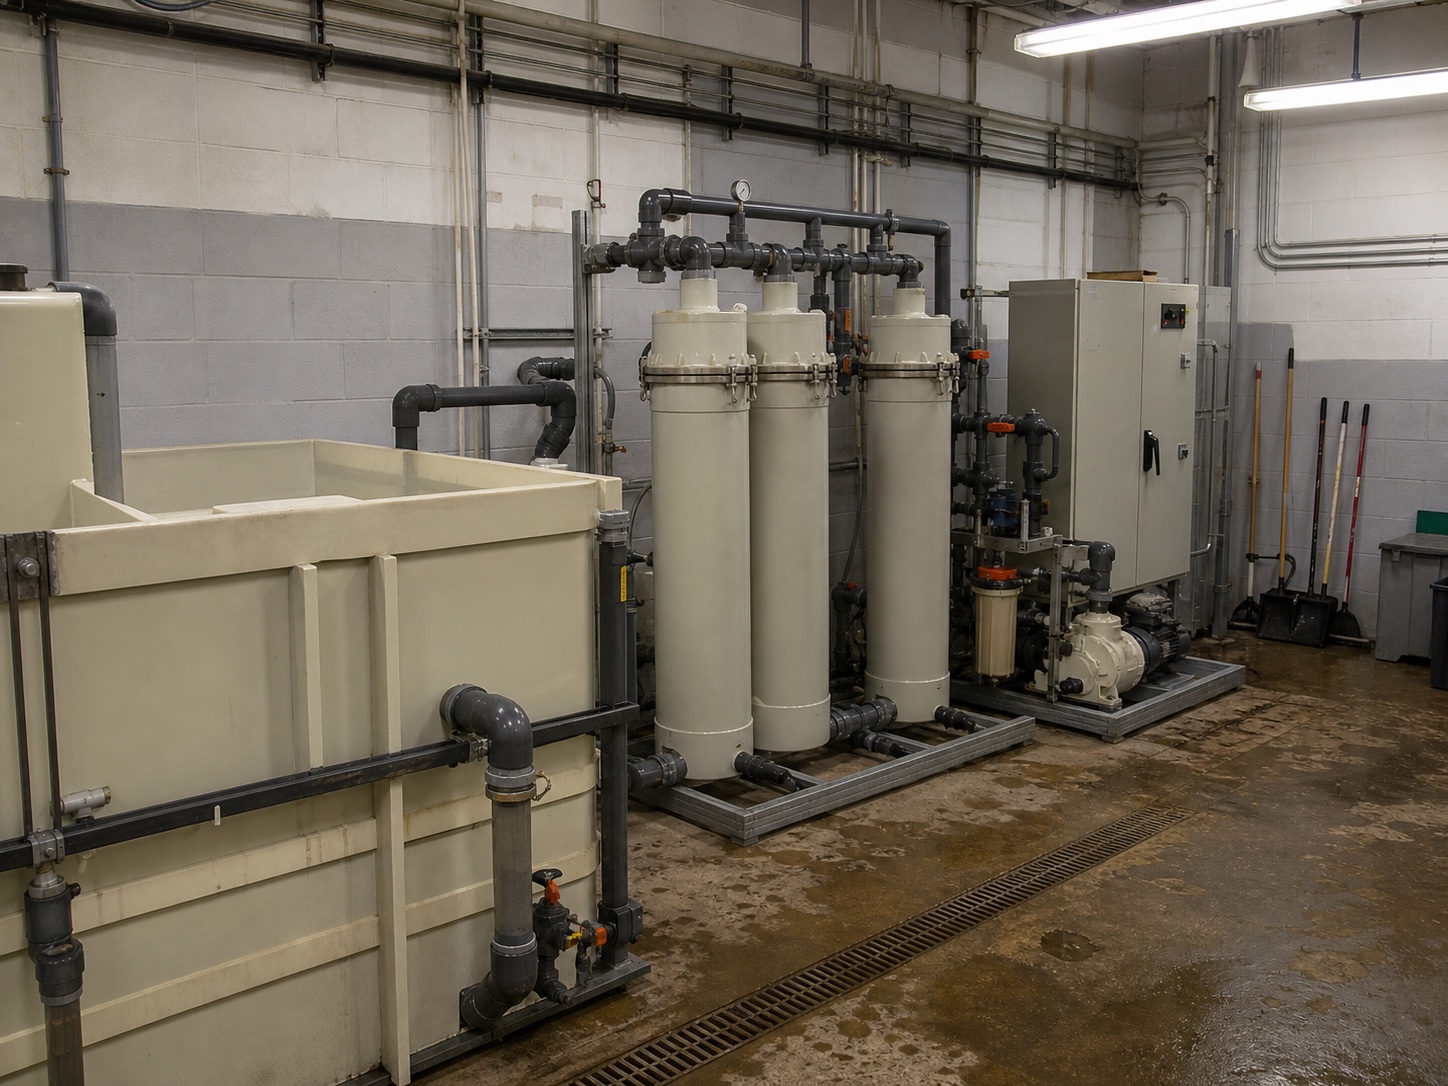
Check PP Sheet Weir Plates Before Installation
Before releasing a component for installation, compare the supplied part with the approved drawing revision. Verify the quantity and segment identification, overall and interface dimensions, hole and slot locations, edge condition, visible damage, labels, and any agreed packaging or inspection records. Record deviations before the plate is fixed in the clarifier.
This is a component acceptance check, not a substitute for commissioning, site survey, or hydraulic performance testing. If the part interfaces with a fabricated tank, use the project drawing and the final installation sequence as the controlling documents.
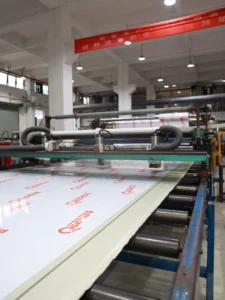
Video reference: PP Sheet Cutting Process: Precision Edge Cutting | QEEHUA. It illustrates general edge and cut-out preparation; it does not demonstrate a clarifier weir design or confirm project suitability.
Request a Drawing Review for PP Sheet Weir Plates
Send the controlled drawing, process summary, required documentation, delivery destination, and target schedule with the RFQ. QEEHUA can then confirm what information is still needed to assess PP sheet fabrication for the stated wastewater-clarifier component. Use the QEEHUA enquiry channel to submit the drawing package and clarify the project-specific material review.
FAQ
What should be shown on a PP sheet weir-plate drawing?
Show the component role, plan and section views, controlled dimensions, crest or interface elevation supplied by the project designer, segment joints, support points, holes, slots, edge treatment, and the drawing revision. Also identify which dimensions the supplier is expected to inspect.
Can a PP sheet supplier design the clarifier weir overflow rate?
No. The project engineer or process designer must set the hydraulic design, including the required overflow arrangement and acceptance criteria. A PP sheet supplier can review whether the requested fabricated component can be assessed from the supplied project information.
Which operating conditions should an RFQ include?
Include the wastewater chemistry, concentration, temperature, cleaning method, solids or abrasion concern, liquid levels, and any applicable project material specification. QEEHUA-specific suitability must be confirmed for the actual service conditions.
What should be checked when PP weir plates arrive on site?
Check the approved drawing revision, part identification, quantity, overall and interface dimensions, hole and slot locations, edge condition, visible transit damage, and required records before installation. Escalate any variance before the component is fixed in the clarifier.