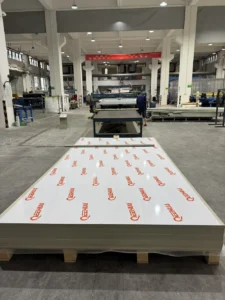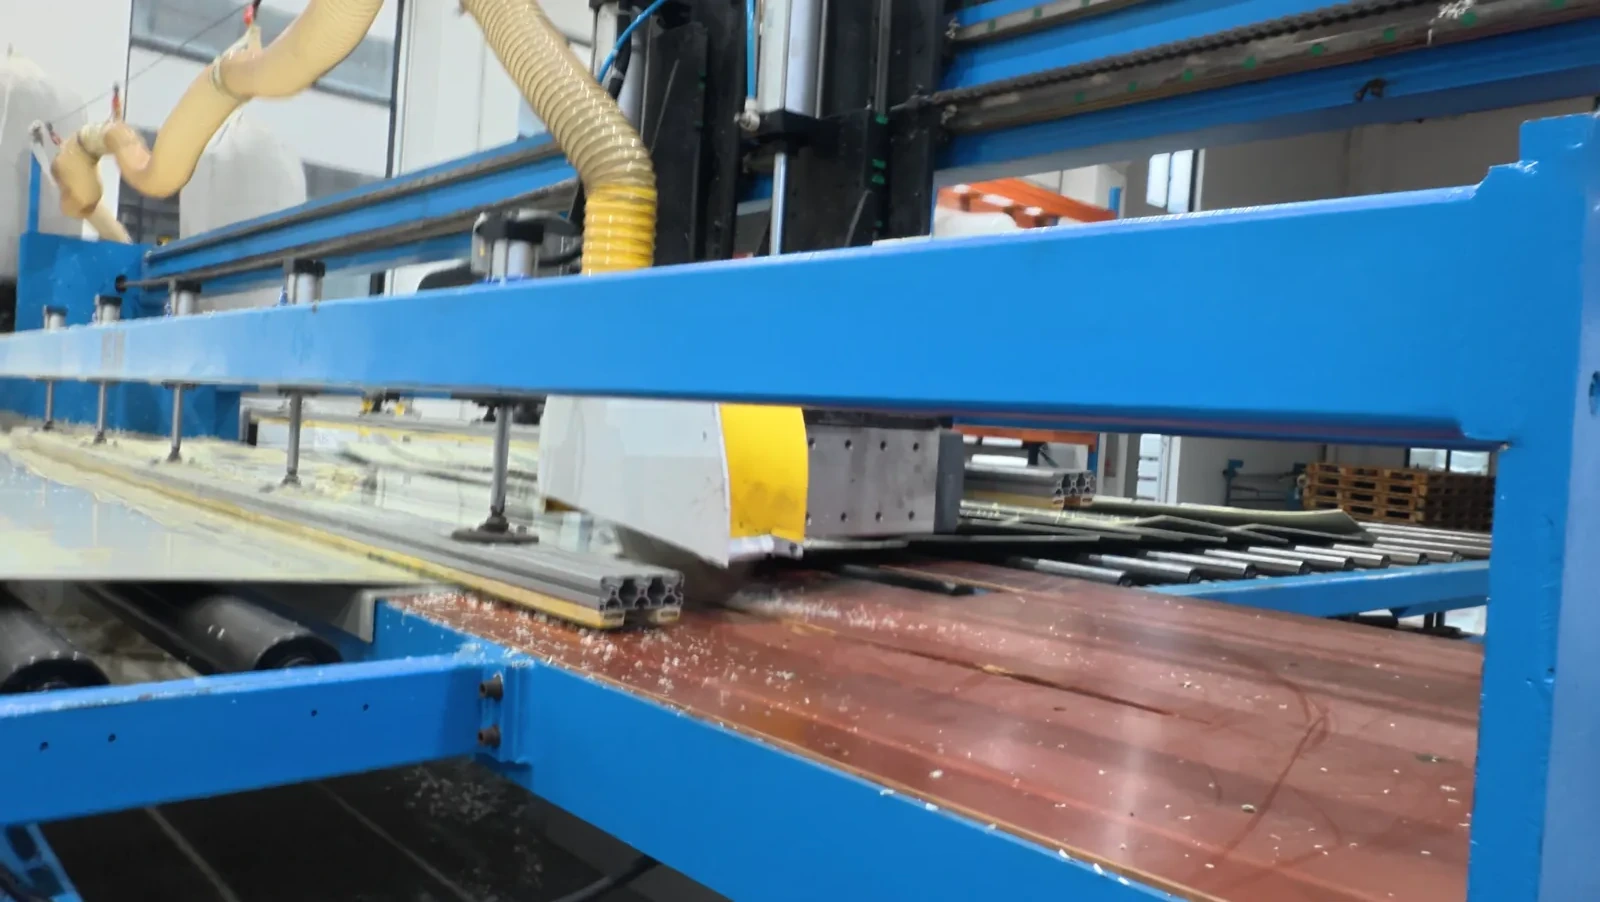
A PP sheet automatic feeding system is useful context for a buyer who wants to understand how material reaches a sheet-production line. It is not enough to approve a sheet for an equipment project. The purchase review must still identify the finished component, the requested grade and dimensions, the chemical or environmental duty, and the fabrication route. The embedded QEEHUA video shows pipes and a hopper in one automatic feeding sequence. Treat it as a visual production reference. Confirm order-specific material, dimensions, test needs, and delivery scope in writing before release.
PP sheet automatic feeding system should be reviewed against the documented project duty, drawings, fabrication scope, material records, and acceptance requirements.
Project context
PP sheet automatic feeding system: project review
Use the documented project requirements to compare the relevant material, fabrication, and quality-control inputs before release.
Automatic feeding does not remove the need for a project material brief. A buyer should state what will be fabricated from the sheet, where it will be installed, and which operating condition matters. A process enclosure, a plating-tank panel, and a wastewater cover can all begin with a PP sheet request but require different technical questions.
The first review should also separate confirmed requirements from open items. If the project owner has not supplied a cleaning chemical, peak temperature, panel span, or functional requirement, keep it open. Assumptions made before production are difficult to correct after cut panels or fabricated parts have been released.
For application context, review QEEHUA’s industry applications and match the inquiry to a named component rather than a broad material label.
Video reference
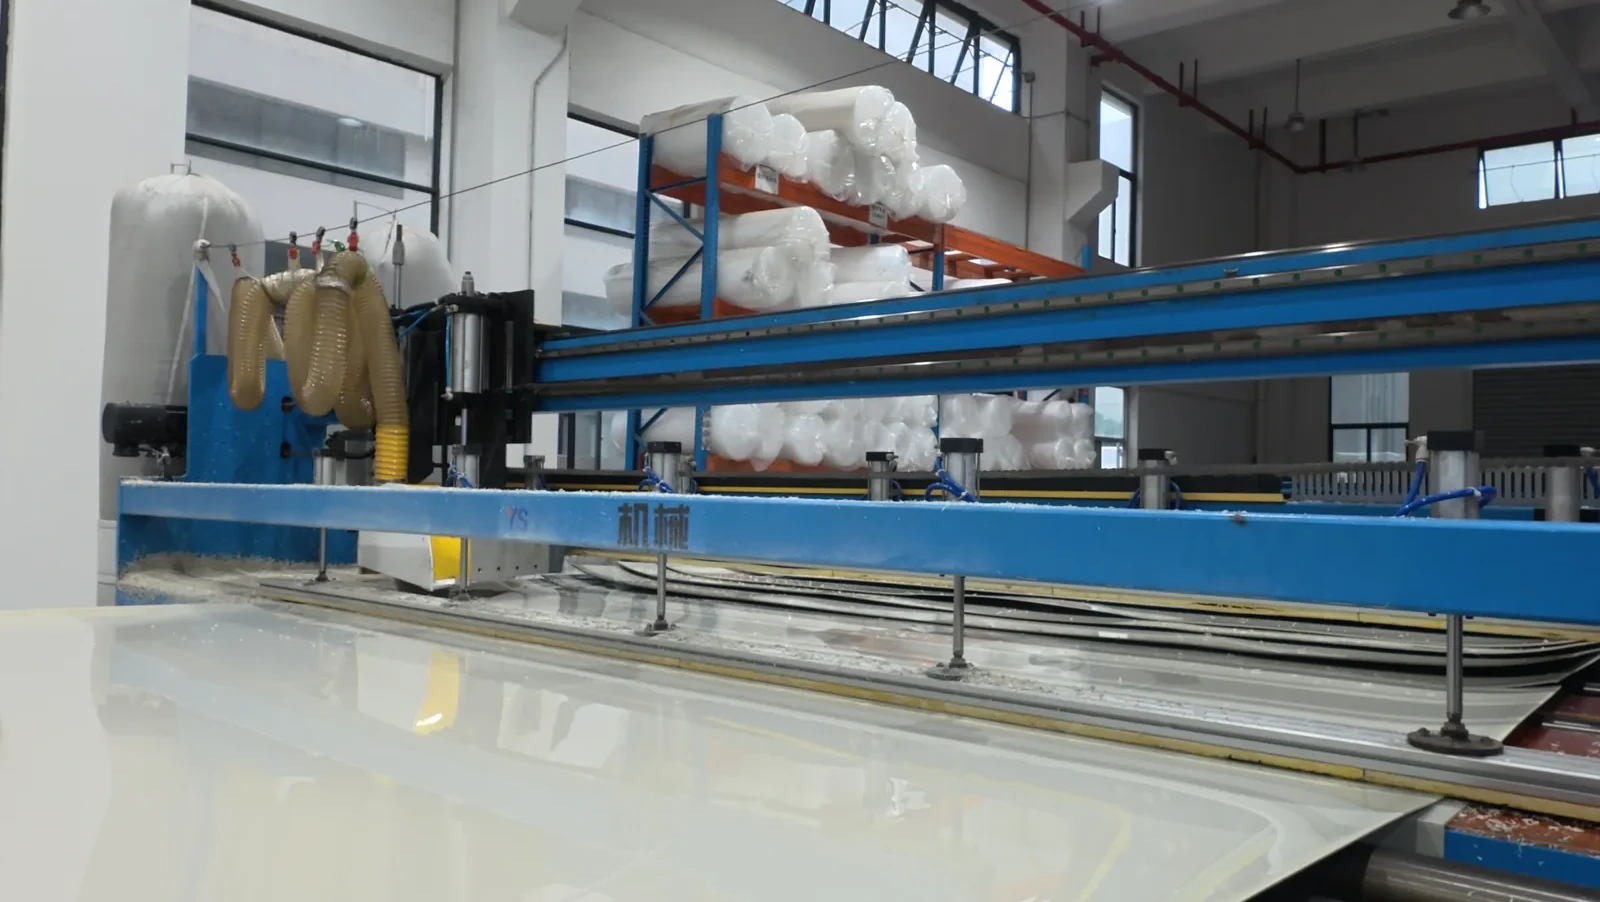
This QEEHUA video shows an automatic feeding arrangement with pipes and a hopper. It is included to give readers a clear visual point of reference when discussing the upstream production stage. It does not disclose a bill of materials, prove a fixed output, or establish the production method for every PP sheet order.
The useful buyer question is whether the supplied material record and the project request point to the same finished part. Put the intended use, sheet details, sample purpose, and drawing revision in one request. That makes it easier to identify when a separate grade or fabrication review is needed.
Video reference: PP Sheet Manufacturing: Hopper in Automatic Feeding System | QEEHUA. It shows a raw-material feeding stage; it does not confirm the complete system configuration or project-specific material requirements.
Material checks
QEEHUA’s data sheet reports density, tensile, flexural, impact, and temperature-related results for a tested sheet sample. Use those records as technical context, not as a replacement for a grade confirmation. A value from a test coupon does not determine panel span, seam design, support spacing, chemical compatibility, or a finished-equipment acceptance condition.
Start with the QEEHUA PP sheet range, then compare the request with the operating conditions and drawing. For chemical-duty equipment, the chemical tank selection guide explains why the medium, concentration, temperature, load, and geometry must remain in the review.
Project data
The following values are presented as a compact reference for the material-review discussion. They remain attached to the tested sample and method. They are not values to copy into a finished-equipment calculation.
| Property | Reported value | Sample and condition | Method |
|---|---|---|---|
| Density | 912 kg/m³ | QEEHUA PP sheet data-sheet sample; conditioning and production grade are not stated | ASTM D792-20 |
| Tensile modulus | 1,820 MPa | QEEHUA PP sheet data-sheet sample; conditioning and production grade are not stated | ASTM D638-22 |
| Notched impact strength | 59 J/m | QEEHUA PP sheet data-sheet sample; conditioning and production grade are not stated | ASTM D256-24 |
| Deflection temperature under load | 137.0 °C | QEEHUA PP sheet data-sheet sample; conditioning and production grade are not stated | ASTM D648-18 |
These are reported values for the data-sheet sample. They do not set a saleable-grade specification, a production tolerance, or a finished-equipment design. Confirm the grade, thickness, drawing, process medium, and operating conditions for the project.
Sources and limits: The embedded QEEHUA process video shows the production scene discussed here. ISO 1133-1 melt flow rate and ISO 291 conditioning and testing atmospheres provide published method or measurement context. The table still identifies the ASTM methods used for the reported QEEHUA sample. Neither external source converts a tested-sample value into an order specification; confirm the project requirements before release.
Before a purchase release, compare the data sheet with the actual request line by line. Check the proposed product, grade or required function, thickness, panel dimensions, colour where relevant, process duty, drawing revision, and sample purpose. A number that is not connected to a named component and condition cannot settle the project decision.
If the project asks for a capability outside the approved data record, state the requirement plainly. This can include a functional grade, an application approval, a special resistance target, a tolerance, or a fabrication test. QEEHUA can then confirm what information is available instead of allowing a general video or a tested-sample value to imply more than it proves.
Factory checks
Production visibility helps when a buyer is comparing material options, but it should not create a claim that is absent from the order. Record the requested sheet format, colour, surface, cut requirement, quantity, and inspection need. If the customer needs a deviation from the normal request, put it on the drawing or specification rather than relying on a video frame or a verbal description.
Where the finished part will be welded or joined, tie the material review to the joint. State the matching sheet, proposed filler, joint form, accessible weld side, and expected operating condition. This is especially important where the part contains liquid, sees a cleaning cycle, or connects to a support frame.
Video limits
A production clip can show a process stage, but it does not show every material grade, inspection point, or order requirement. It should never be used to infer fixed lead time, universal tolerance, certification, functional performance, or a finished-equipment design.
Release record
Keep the release record simple and traceable. It should identify the customer component, drawing revision, proposed sheet, dimensions, the condition that controls the review, requested fabrication, sample purpose, and the party who will approve the result. When one of those items changes, the review should be reopened for that changed item.
This record also separates a technical discussion from a commercial assumption. A production image, a process video, a sheet coupon, and a completed equipment drawing have different purposes. Keep each item attached to the question it can answer, then record any requirement that still needs a project-specific confirmation.
Sample request
A sample is more useful when it answers one defined question. State whether the buyer will review surface appearance, machining, fit, a welded detail, or a project test. Include the latest drawing and the project conditions that affect the answer. See the PP sheet sample-request guide for a project checklist, then send the drawing and request a project sample.
Frequently asked questions
Does an automatic feeding video confirm material availability?
No. The video is a production reference. Availability, grade, dimensions, and order details require confirmation for the project.
What should an automatic-feeding-system article help a buyer check?
It should help the buyer prepare a material brief that links the finished part, operating conditions, drawing, and sample purpose.
Can a test value be used as a sheet tolerance?
No. The reported test data does not publish an order tolerance. Confirm dimensions and tolerance requirements for the requested product.
When is a welded sample better than a flat coupon?
Use a welded sample when the project decision concerns a joint, corner, penetration, or another fabricated detail.
For PP sheet automatic feeding system, record the final project assumptions and acceptance checks before releasing the fabrication or purchase scope.