PP U-shaped slots is assessed against the actual project duty. Pp u-shaped slot selection should start with the actual equipment duty and drawing. A U-shaped slot should be specified from the equipment drawing and its role in the assembly. Describe the cross-section, mating part, span, load, frame, joint, vibration, exposure, and installation sequence. Larger spans or loaded equipment may need reinforcement review; this is not a universal structural rule. The material request needs the chemical, temperature, geometry, support, joint, and inspection information that applies to the finished assembly. QEEHUA internal data can support a first material discussion, but it should not be expanded into a grade-wide promise, an equipment design calculation, or an approval for unlisted conditions. Send the project information with the sample request so the proposed sheet, rod, or profile can be reviewed against the real use before material is released.
PP U-shaped slots should be reviewed against the documented project duty, drawings, fabrication scope, material records, and acceptance requirements.
Project duty
PP U-shaped slots: project review
Use the documented project requirements to compare the relevant material, fabrication, and quality-control inputs before release.
A U-shaped slot should be specified from the equipment drawing and its role in the assembly. Describe the cross-section, mating part, span, load, frame, joint, vibration, exposure, and installation sequence. Larger spans or loaded equipment may need reinforcement review; this is not a universal structural rule.
Use the QEEHUA industry applications page as context for the equipment category. The final decision needs the stated project information and should not rely on a generic application label.
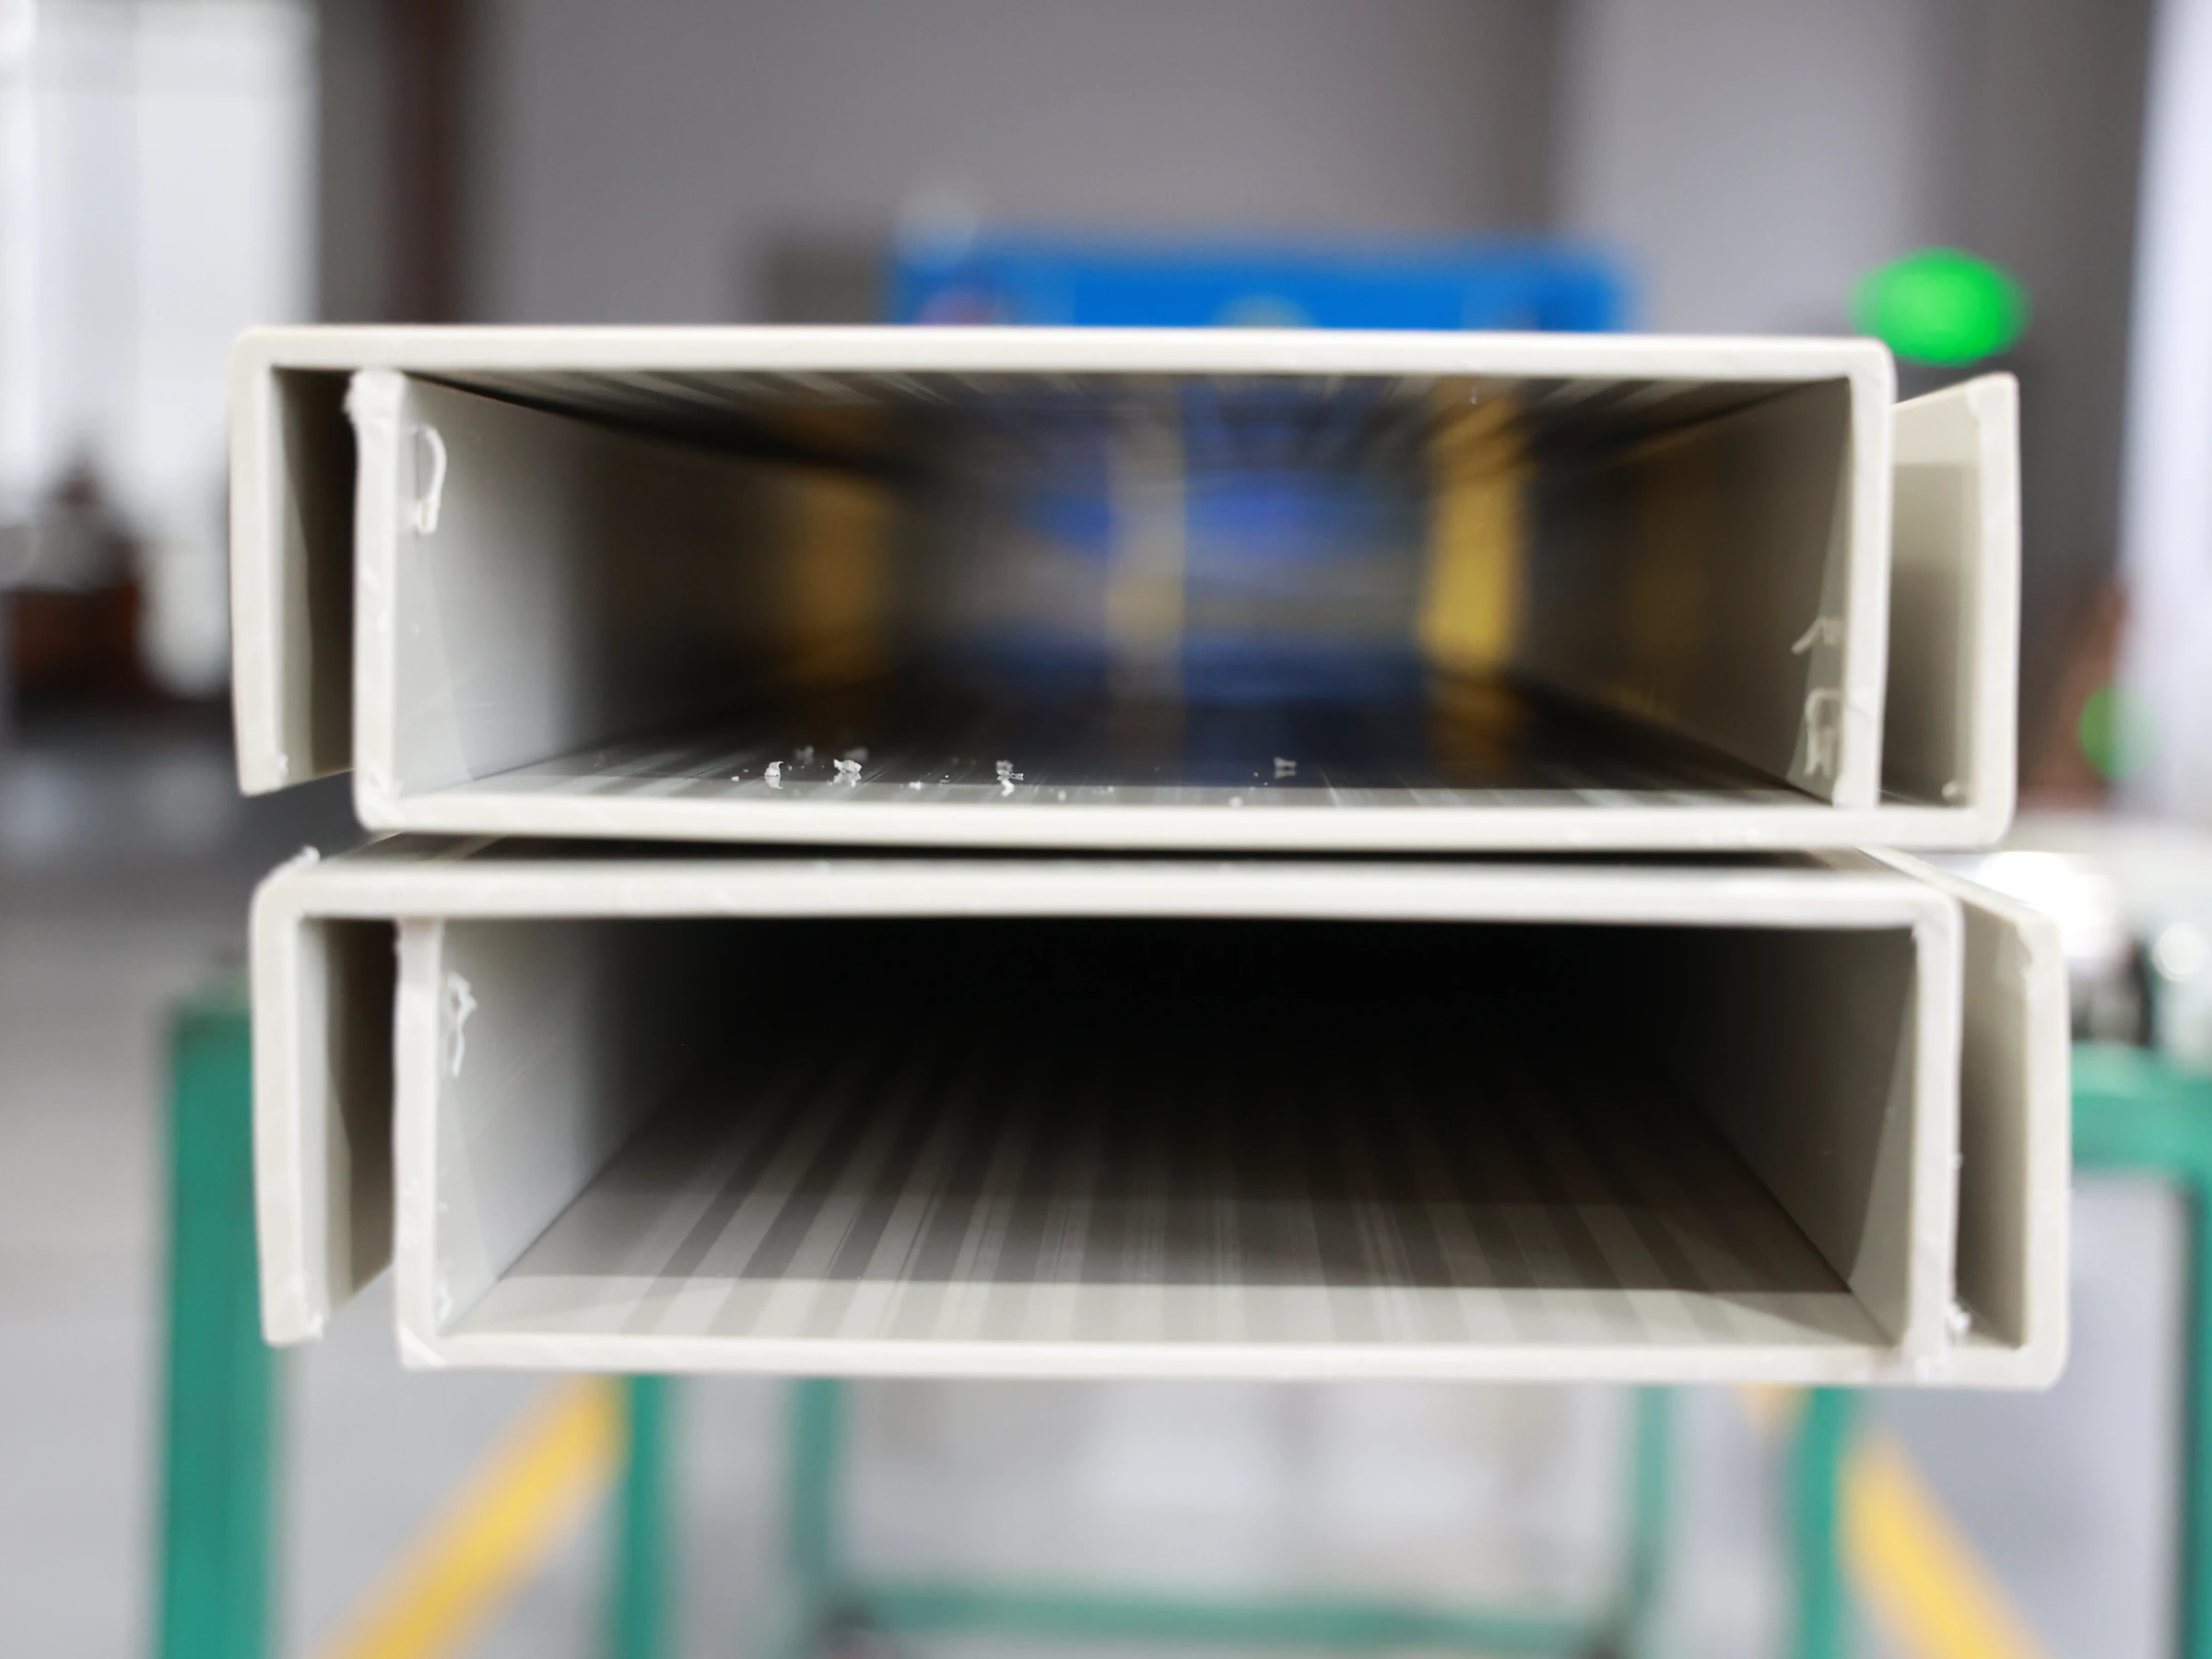
A PP U-shaped slot is a component in an assembly, not a stand-alone performance claim. Start with a dimensioned cross-section and identify the mating sheet or part, the installed orientation, the length, the span between supports, the joining method, and the service environment. The drawing should also show whether the profile carries a local load or only guides and protects another component.
Larger spans or loaded equipment may need a reinforcement review. That statement is not a universal 500 mm rule and does not replace a structural calculation. The project engineer needs the actual span, frame arrangement, load, vibration, pressure or vacuum effect, and installation sequence before deciding how the profile is supported.
Material role
The QEEHUA PP sheet range is the base product reference. The selection question is whether the proposed material, construction detail, and service conditions work together. A panel, a welded joint, a profile, and a support interface can have different demands in the same equipment.
Separate the initial material screen from the equipment approval. This keeps a useful data-sheet discussion from being mistaken for a design calculation or a production commitment.
Conditions to confirm
Service conditions
State every relevant medium, concentration, normal and maximum temperature, exposure duration, cleaning condition, and upset condition. If the project includes no chemical contact, state the installation environment and operating temperature instead. Do not infer performance from a similar chemical or a broad process name.
Geometry and support
Record panel spans, liquid height or process load, positive or negative pressure where relevant, supports, penetrations, reinforcement, welding access, and inspection points. These details determine what the fabricator and project engineer need to review.
The environment should be described where the profile is installed. State whether it is indoors, outdoors, wet, exposed to a listed process liquid, or near a cleaning operation. If temperature cycling or vibration is expected, put it on the inquiry. These conditions can affect the interface and support review even when the profile itself has a simple cross-section.
A profile drawing should show the mating dimensions and the allowed assembly route. A channel that must be welded after another part is installed has different access from a channel fitted before closing the assembly. Record the cut ends, corners, penetrations, and any frame connection so the fabrication team can identify open points early.
Relevant data
The following table keeps the reported data or required project inputs with the condition that gives them meaning. It is not a substitute for the equipment design basis.
| Project data | Reported value or input | Material or condition | Method or check |
|---|---|---|---|
| Profile section | Dimensioned cross-section | Mating sheet or component | Confirm drawing |
| Span and load | Project value | Installed assembly | Review support and frame |
| Joining plan | Welded or mechanical detail | Joint location | Confirm access and process |
| Environment | Indoor, outdoor, wet, or chemical contact | Service conditions | Confirm project duty |
Scope of the data: A U-shaped slot is not a structural calculation. Review span, load, frame, joints, vibration, and service conditions before final selection.
A profile request becomes easier to review when the drawing identifies the part function. State whether the U-shaped slot guides a panel, protects an edge, joins a detail, or works with a support frame. Then add the component length and installation orientation. Note which part is supplied by the customer and which part is inside the PP profile scope. Mark any on-site trimming, drilling, or field joining that may change the installed detail. These points do not create a structural claim. They tell the project reviewer which dimensions, interfaces, and service conditions need to be checked before material is released.
Fabrication checks
Define the cut edges, joint type, sequence, access, process equipment, and inspection requirement before issuing the production request. When a thermoplastic welded detail is involved, include the matching PP welding rod request. When a channel or reinforcement feature is involved, include the PP U-shaped slot section drawing and mating dimensions.
Joint quality and finished-equipment performance depend on the assembly process. The safest specification is the one that makes the drawing, service duty, material, and inspection condition visible to the same review.
Keep the request focused on the installed detail. Include the cross-section, length, toleranced mating dimension where specified by the project, cut or corner detail, joining plan, support points, and inspection requirement. If the profile is part of a reinforced assembly, show the frame or support drawing rather than asking the supplier to infer it from the profile name.
Sample request
Send the drawing, equipment use, chemical and temperature information where relevant, requested dimensions, fabrication route, sample purpose, and any test or approval requirement. Request a project sample or submit the equipment information. An open point should be marked as open, not replaced with an assumed typical condition.
A useful U-shaped slot sample normally includes the section that will mate with the project component. When fit is the main question, send the mating part dimensions or a drawing view. When load or support is the question, the project team should first define the design basis and the sample purpose.
Frequently asked questions
What information is needed for a PP U-shaped slot review?
Provide the equipment drawing, service conditions, dimensions, fabrication route, quantity, and any inspection or approval requirement.
Can a single data-sheet value approve the full assembly?
No. Material test results are inputs to a project review. The final assembly also depends on geometry, loads, supports, joints, service conditions, and the design basis.
Why should the drawing be sent with the material request?
The drawing shows spans, penetrations, supports, joint access, and interfaces that cannot be determined from a material name or panel size alone.
What should be included with a sample request?
Send the project duty, drawing, requested material or detail, fabrication plan, sample purpose, and acceptance requirement so the sample can be discussed against the real use.
For PP U-shaped slots, record the final project assumptions and acceptance checks before releasing the fabrication or purchase scope.